For the efficient and reliable transportation of organic fertilizer granules, the design and selection of a pneumatic conveying system are critical. This article provides a comprehensive overview of the key considerations, calculations, and equipment choices involved in implementing such a system, tailored for the specific needs of organic fertilizer processing facilities.
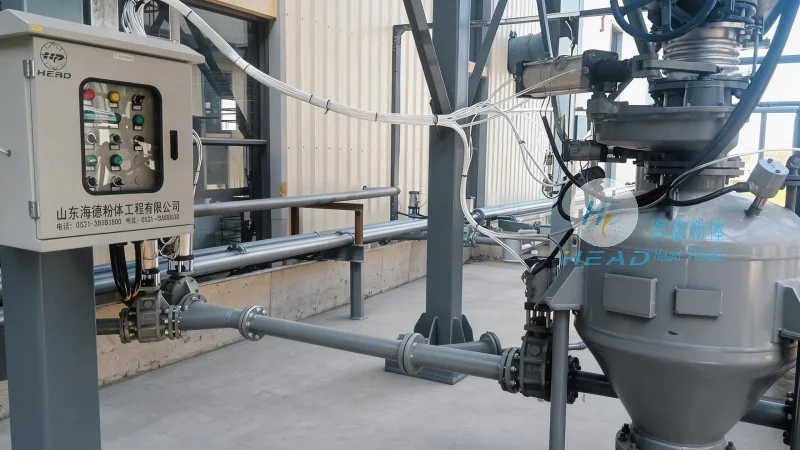
Organic fertilizer granules, often composed of composted materials or other natural nutrient sources, present unique challenges in material handling due to their size, density, and moisture content. Traditional mechanical conveyors may struggle with the abrasive or sticky properties of these granules, leading to increased wear and maintenance costs. Pneumatic conveying systems offer a solution by utilizing air pressure to transport materials through pipelines, providing a flexible, dust-free, and low-maintenance alternative. The design of an effective pneumatic conveying system for organic fertilizer granules requires careful consideration of several factors, including material characteristics, conveying distance, and desired throughput.
When designing a pneumatic conveying system for organic fertilizer granules, engineers must first assess the physical properties of the material. This includes determining the particle size distribution, bulk density, and flowability of the granules. These parameters directly impact the selection of the conveying method—whether it's a pressure or vacuum system—and the required air velocity and pressure. For example, smaller granules may require higher air velocities to prevent clogging, while larger or denser granules might necessitate higher air pressure to ensure proper suspension. The system's design must also account for the potential for moisture content variations, as excess moisture can affect the material's flow characteristics and increase the risk of blockages.
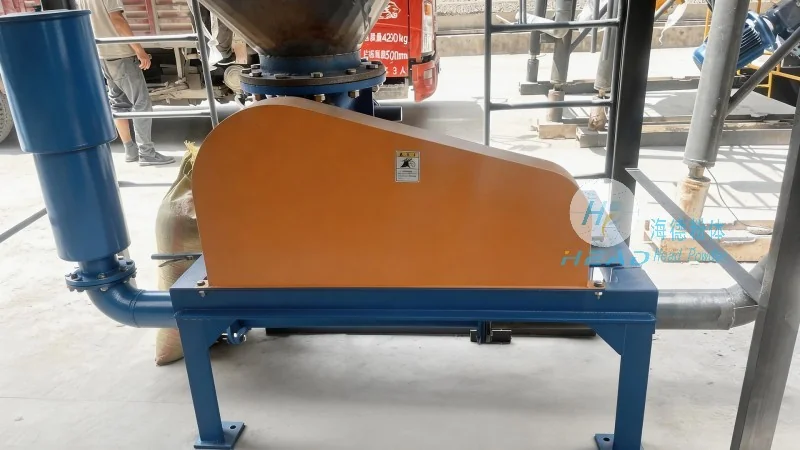
Accurate calculation of pneumatic conveying parameters is essential to ensure the system operates efficiently and reliably. The primary calculations involve determining the required air volume, pressure, and power consumption. The air volume is typically calculated based on the material's bulk density and the desired conveying rate. The pressure required is determined by the total pressure drop across the system, which includes losses due to bends, fittings, and the conveying pipeline itself. Engineers use empirical formulas and industry standards, such as those from the Pneumatic Conveying Institute (PCI), to estimate these parameters. For instance, the pressure drop per unit length of pipe can be calculated using the Darcy-Weisbach equation, adjusted for the specific characteristics of the organic fertilizer granules. Additionally, the power consumption of the air compressor is calculated based on the required air volume and pressure, ensuring the system is energy-efficient and cost-effective.
The selection of appropriate equipment is a critical step in the design of a pneumatic conveying system for organic fertilizer granules. The key components include the material feed system, air compressor, conveying lines, and material discharge equipment. The material feed system must be capable of handling the organic fertilizer granules without causing blockages or excessive wear. Options include rotary valves, star feeders, or screw conveyors, depending on the material's flowability and the system's requirements. The air compressor must be selected based on the required air volume and pressure, with considerations for noise levels, maintenance, and energy efficiency. Common types include rotary lobe compressors and centrifugal compressors, each with its own advantages and limitations. The conveying lines are typically made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of the organic fertilizer granules. The line diameter and length are determined based on the air velocity and pressure drop calculations. Finally, the material discharge equipment, such as rotary valves or pneumatic receivers, must be designed to handle the granules without causing clogging or spillage, ensuring smooth operation at the end of the conveying line.
Once the individual components are selected, the entire system must be integrated and optimized for performance. This involves simulating the system's operation under various conditions to identify potential bottlenecks or areas for improvement. Engineers may use computational fluid dynamics (CFD) software to model the flow of air and granules through the system, allowing for adjustments to the design before implementation. The system's control system is also critical, as it must regulate the air pressure, material feed rate, and discharge operation to maintain consistent performance. Automation features, such as variable frequency drives (VFDs) for the air compressor and material feeders, can enhance the system's efficiency and reduce energy consumption. Regular maintenance and monitoring are essential to ensure the system operates within its design parameters and to address any issues promptly.
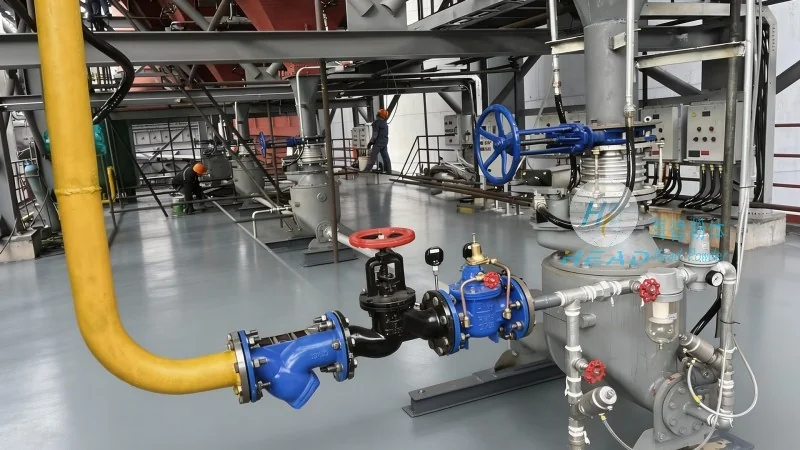
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, has successfully implemented a pneumatic conveying system for an organic fertilizer granule processing plant. The project involved the design and installation of a pressure pneumatic conveying system capable of transporting 10 tons per hour of organic fertilizer granules over a distance of 200 meters. The system was designed to handle granules with a particle size range of 2-5 mm and a bulk density of 0.8-1.0 g/cm³. The calculations for the system included determining the required air volume (approximately 5000 m³/h) and pressure (0.6 MPa). The equipment selected included a rotary lobe air compressor, stainless steel conveying lines with a diameter of 150 mm, and a rotary valve discharge system. The system has been in operation for over two years, achieving high reliability and low maintenance costs. The client reported significant improvements in production efficiency and reduced labor costs compared to traditional mechanical conveyors.
Designing and selecting a pneumatic conveying system for organic fertilizer granules requires a comprehensive approach that considers material properties, system calculations, and equipment selection. By following industry best practices and leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., facilities can achieve efficient, reliable, and cost-effective material handling solutions. The key to success lies in thorough planning, accurate calculations, and the selection of appropriate equipment tailored to the specific needs of the organic fertilizer processing operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top