Shandong HeadPowder Engineering Co., Ltd., commonly known as Headpowder, is a professional manufacturer and supplier based in Shandong, China. The company specializes in the research, development, and production of material handling systems, particularly those designed for lightweight aggregate applications. With a focus on innovation and customer-centric solutions, Headpowder aims to provide efficient and reliable equipment for various industrial and construction needs.
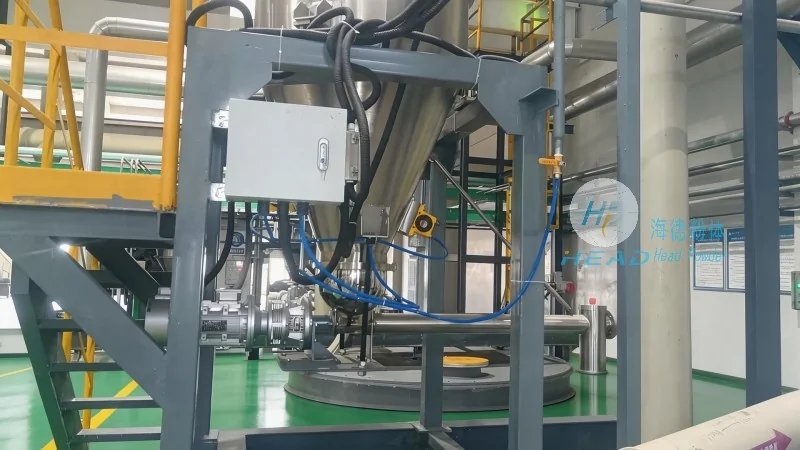
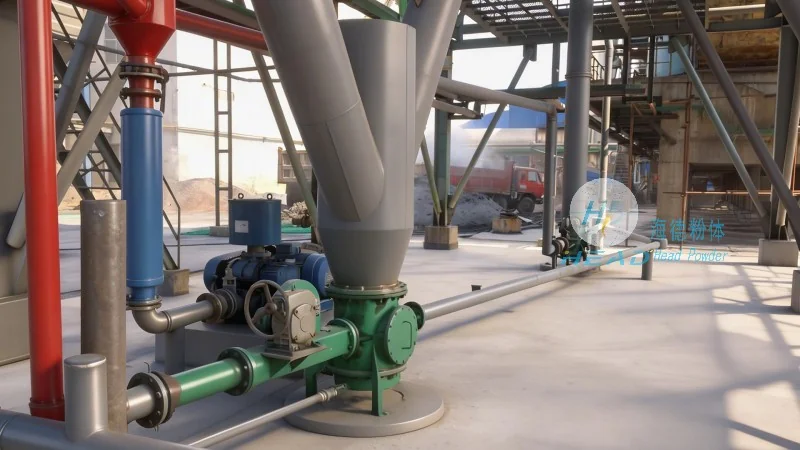
The fundamental principle of lightweight aggregate material handling systems revolves around the efficient transport of bulk materials, such as expanded clay, perlite, or other lightweight aggregates. These systems are engineered to handle materials with low density and fine particle characteristics, which often present challenges in traditional material handling. The core technology employed includes pneumatic conveying, where air is used to move materials through pipelines, and mechanical conveying, which may involve screw conveyors, belt conveyors, or bucket elevators. The choice of method depends on factors like material properties, distance, and required flow rate. For lightweight aggregates, pneumatic conveying is often preferred due to its ability to minimize dust generation and maintain material integrity. The system typically consists of a material hopper, a conveyor line, and a control unit. The hopper stores the aggregate, while the conveyor transports it to the target location. Advanced control systems ensure precise flow regulation, preventing overloading or underflow. Additionally, features like dust collection and filtration are integrated to comply with environmental regulations and maintain a clean working environment.
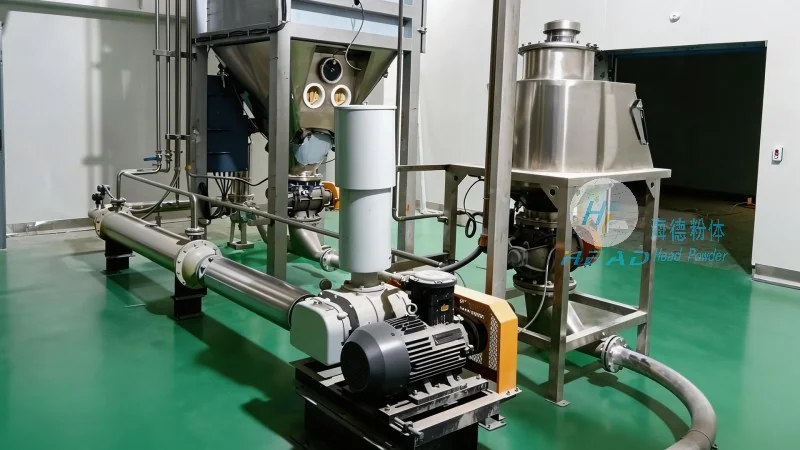
Lightweight aggregate material handling systems from Headpowder are designed with several key features that enhance their performance and reliability. One of the primary advantages is their energy efficiency, achieved through optimized air flow and motor control systems. This reduces operational costs and aligns with sustainable manufacturing practices. The equipment is also built with durable materials to withstand the abrasive nature of lightweight aggregates, ensuring long service life and minimal maintenance. Advanced control technology allows for real-time monitoring and adjustment of the system, providing operators with detailed insights into material flow and system performance. Additionally, the systems are equipped with safety features, such as overload protection and emergency stop mechanisms, to prevent accidents and ensure workplace safety. The modular design of the equipment enables easy installation and maintenance, reducing downtime and increasing overall productivity. These features collectively make the systems a reliable and cost-effective solution for handling lightweight aggregates in various applications.
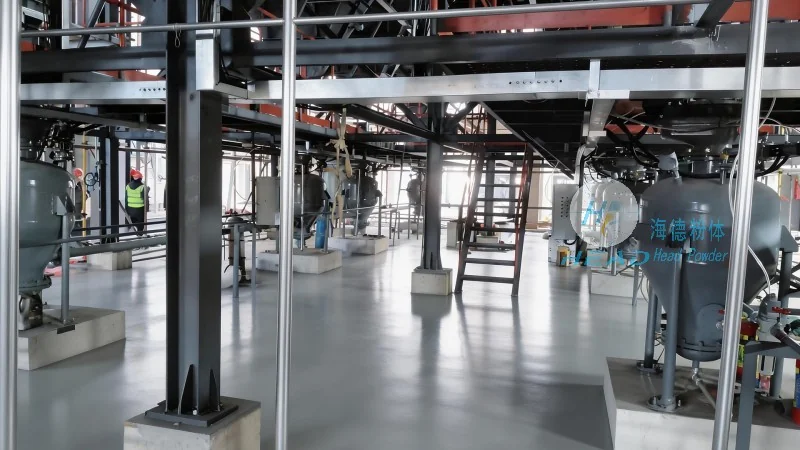
Lightweight aggregate material handling systems are deployed in a variety of working environments, each presenting unique challenges and requirements. In concrete mixing plants, the primary application is to supply lightweight aggregates to batching equipment, ensuring consistent mix proportions and reducing the risk of material segregation. The systems operate continuously, matching the production rate of the mixing plant and maintaining a steady flow of aggregates. This not only enhances the quality of concrete but also improves overall plant efficiency. On construction sites, the equipment is used to transport aggregates from storage silos or bulk containers to the mixing location. The systems are designed for high mobility and can be easily repositioned as the construction progresses. This flexibility allows for efficient material handling across different project phases, from foundation to superstructure. In industrial production lines, the systems support automated processes by delivering aggregates to processing machinery, such as grinding or mixing equipment. The ability to maintain a consistent material supply is critical for maintaining production throughput and product quality. Key advantages in these scenarios include increased operational efficiency, reduced labor costs, and improved safety by minimizing manual handling. The systems also contribute to environmental sustainability by reducing dust emissions and improving material utilization rates.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top