HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for malt powder applications. This article delves into the fundamental principles of malt powder pneumatic conveying and explores the specific operational scenarios where such systems excel, highlighting the efficiency and reliability that define modern malt processing operations.
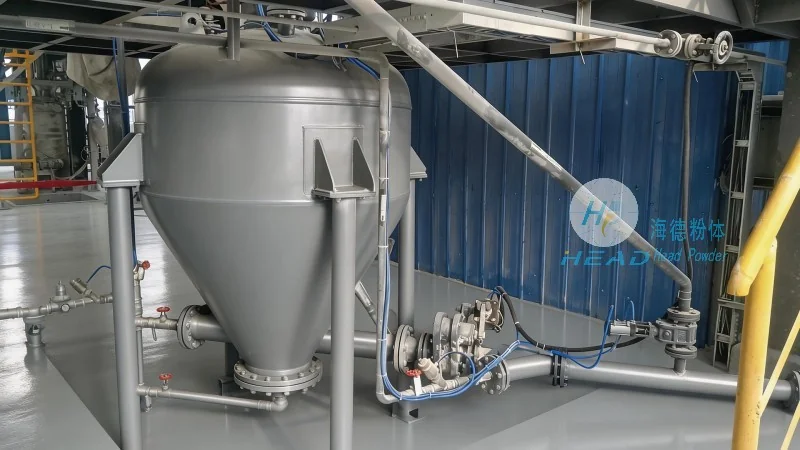
Pneumatic conveying is a method of transporting bulk materials, such as malt powder, using a stream of pressurized or vacuum air. The process involves several key components and mechanisms that work in concert to ensure smooth and efficient material movement. At its essence, the system relies on the creation of a pressure differential to move the powder through a pipeline. There are two primary types of pneumatic conveying systems: pressure systems, which use positive pressure to push the material forward, and vacuum systems, which use negative pressure to pull the material toward the receiver. For malt powder, which is typically fine and can be prone to caking or agglomeration, a well-designed pressure system often offers superior performance due to its ability to maintain consistent flow rates and prevent material degradation.
The fundamental principle of pressure pneumatic conveying involves the use of a blower or compressor to generate high-pressure air that is introduced into the material hopper. As the air flows through the hopper, it entrains the malt powder particles, forming a dense mixture known as a "conveying stream." This stream is then directed through the pipeline to the destination point, such as a silo, storage tank, or processing unit. The velocity of the air within the pipeline is critical; it must be sufficient to overcome the gravitational forces acting on the powder and maintain a stable flow without causing excessive wear on the system components. Proper design of the pipeline diameter, length, and bends is essential to minimize pressure drop and ensure that the conveying velocity remains within the optimal range for the specific malt powder characteristics.
Effective malt powder pneumatic conveying systems consist of several interconnected components, each playing a vital role in the overall operation. The primary components include the material hopper, which serves as the storage and feeding point for the malt powder; the air supply unit, which provides the necessary pressure or vacuum; the conveying pipeline, which transports the material; and the receiver, where the material is deposited. Additional components may include filters, cyclones, and dust collectors to manage air quality and prevent material loss. The material hopper is typically equipped with a feeder, such as a rotary valve or a screw feeder, which regulates the flow of malt powder into the conveying system. This feeder ensures a consistent feed rate, preventing overloading or underloading of the system, which can lead to inefficient operation or equipment damage. The air supply unit, whether a positive displacement blower or a centrifugal fan, must be capable of delivering the required air volume and pressure to maintain the desired conveying velocity. The conveying pipeline is usually made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of malt powder and the potential for moisture or chemical exposure. Bends and elbows in the pipeline are designed with smooth transitions to minimize pressure loss and reduce the risk of material deposition or blockages. The receiver, often a silo or storage tank, is equipped with a discharge valve to control the release of the malt powder, ensuring that the material is deposited in a controlled manner without spillage or contamination.
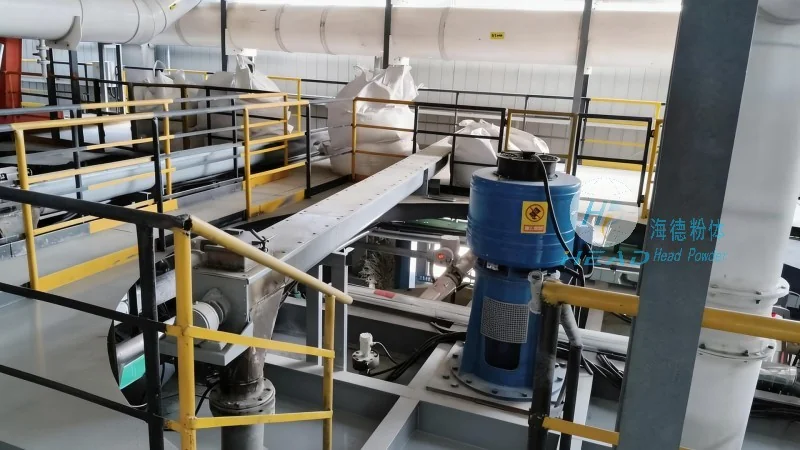
Malt powder pneumatic conveying is particularly well-suited for a variety of operational scenarios within the malt processing industry. One common application is the transfer of malt powder from bulk storage silos to processing equipment, such as maltsters or mash tanks. In this scenario, the system efficiently moves large quantities of malt powder over significant distances, often with minimal manual intervention. The ability to handle fine powders without the need for mechanical conveying equipment, such as conveyor belts or buckets, reduces the risk of material degradation and contamination, which is critical for maintaining the quality of the final product. Another key scenario is the transfer of malt powder between different processing stages, such as from a grinding unit to a mixing tank or from a drying unit to a storage silo. Pneumatic conveying systems excel in these applications due to their flexibility and ability to handle varying flow rates and material characteristics. For example, when transferring malt powder from a dryer to a storage silo, the system can handle the increased temperature and moisture content of the material without causing caking or blockages, as the air flow helps to maintain the powder in a free-flowing state.
A third important operational scenario involves the use of pneumatic conveying systems in large-scale malt production facilities, where multiple production lines may need to share a common storage or processing area. In such cases, the system can be configured to route malt powder from various production units to a central storage silo or to different processing equipment as needed. This flexibility allows for efficient material management and reduces the need for multiple manual handling operations, which can be time-consuming and labor-intensive. Additionally, pneumatic conveying systems are often used in scenarios where the malt powder needs to be transported through complex layouts, such as around existing equipment or through multi-story buildings. The ability to route the pipeline vertically and horizontally with minimal restrictions makes pneumatic conveying a practical solution for these challenging layouts.
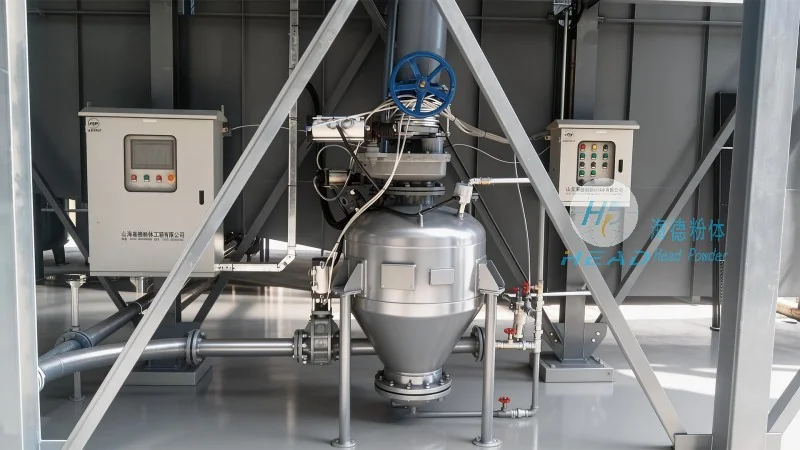
Implementing a malt powder pneumatic conveying system offers several advantages that make it a preferred choice for many malt processing operations. One of the primary benefits is the reduction in material handling costs. By eliminating the need for mechanical conveyors, such as belt conveyors or bucket elevators, the system reduces the capital and operational expenses associated with these equipment types. Additionally, pneumatic conveying systems can handle fine powders more effectively than mechanical systems, reducing the risk of material degradation and ensuring consistent product quality. The system also minimizes the risk of cross-contamination, as the material is contained within the pipeline and does not come into direct contact with the environment. Another advantage is the flexibility of the system, which allows for easy modification or expansion as production needs change. For example, additional pipelines or receivers can be added to the system without major reconfiguration, providing scalability for growing operations.
However, there are also considerations to keep in mind when implementing a malt powder pneumatic conveying system. One of the main challenges is the potential for pressure drop and material blockages, especially with fine or cohesive powders like malt powder. Proper system design, including appropriate pipeline sizing and the use of filters and cyclones, is essential to prevent these issues. Additionally, the system requires regular maintenance to ensure optimal performance. Components such as the air supply unit, filters, and pipeline must be inspected and serviced regularly to prevent wear and tear or clogging. The cost of the initial investment for a pneumatic conveying system can also be higher than that of mechanical systems, although the long-term operational savings often justify the upfront cost. Finally, the system's efficiency depends on the proper selection of the air velocity and pressure, which must be matched to the specific characteristics of the malt powder being conveyed. Incorrect settings can lead to inefficient operation or damage to the system components.
HeadPowder, with its expertise in powder handling technology, plays a crucial role in providing tailored pneumatic conveying solutions for malt powder applications. By understanding the unique characteristics of malt powder and the specific operational requirements of malt processing facilities, HeadPowder designs and implements systems that optimize material flow, minimize degradation, and enhance overall operational efficiency. The company's commitment to quality and innovation ensures that its customers receive reliable and durable systems that meet their production needs. With a focus on customer satisfaction and long-term partnership, HeadPowder continues to be a leader in the field of malt powder pneumatic conveying, helping to advance the efficiency and quality of malt processing operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top