Understanding the principles and application characteristics of bentonite powder pneumatic conveying is crucial for industries that rely on efficient material handling. This article provides a detailed overview of the technology, its operational mechanisms, and the specific scenarios where it excels, all presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
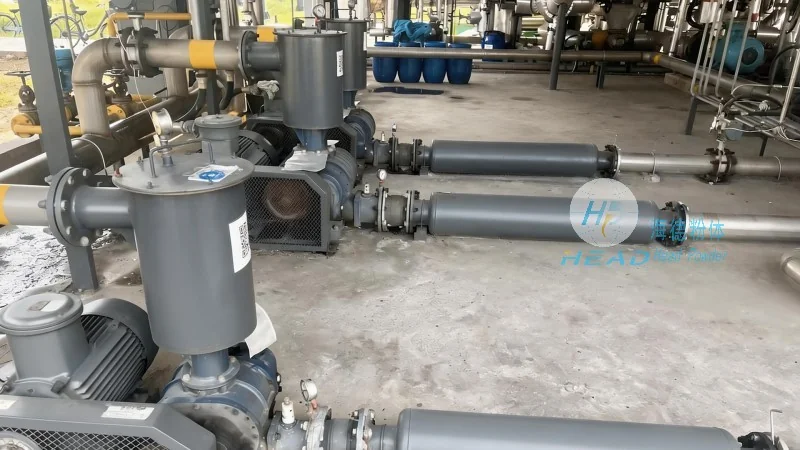
Bentonite powder, a versatile clay material widely used in various industrial applications, requires specialized handling methods to ensure safety, efficiency, and product integrity. Pneumatic conveying offers an effective solution for transporting bentonite powder from one location to another, leveraging air pressure to move the material through a system of pipes and equipment. This method not only minimizes dust exposure and contamination risks but also enhances operational flexibility compared to traditional bulk handling techniques.
The fundamental principle behind bentonite powder pneumatic conveying is the use of air as the transport medium. In a typical system, a blower or compressor generates the necessary air pressure, which is then directed into a hopper containing the bentonite powder. As the air flows through the hopper, it lifts and carries the powder particles through the pipeline network to the destination point, such as a storage silo, processing unit, or packaging area. The velocity of the air and the design of the conveying system are critical factors that determine the efficiency and reliability of the process. Proper air velocity ensures that the powder is fully suspended and transported without clogging or degradation.
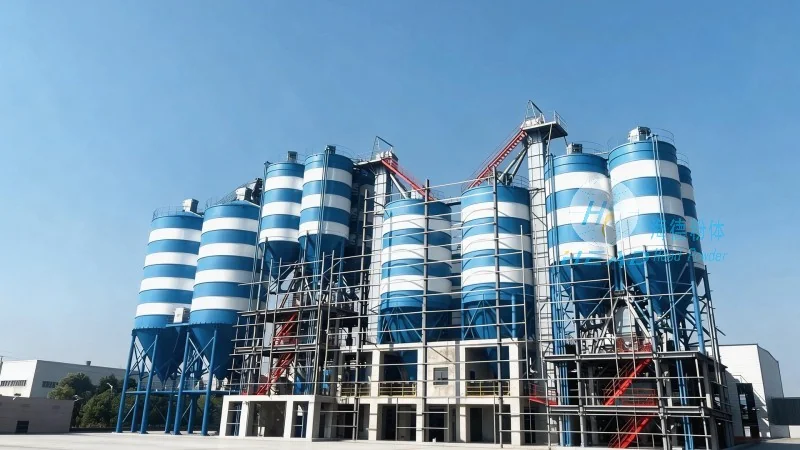
A well-designed pneumatic conveying system for bentonite powder consists of several essential components, each playing a vital role in the overall operation. These components include a hopper or feeder to store and meter the powder, a blower or compressor to generate the air flow, a pipeline network to transport the material, and a receiver or silo to collect the delivered powder. Additionally, accessories such as filters, cyclones, and pressure vessels may be incorporated to manage dust, separate air from the powder, and maintain system pressure. The selection of these components depends on factors like the powder's properties (e.g., particle size, moisture content, density), the conveying distance, and the required flow rate.
Compared to other material handling methods, pneumatic conveying offers several advantages for bentonite powder applications. One of the most significant benefits is the reduction of dust and contamination, which is particularly important for products that require high purity, such as those used in pharmaceuticals, food processing, or water treatment. The enclosed system also minimizes environmental impact and improves workplace safety by containing dust and preventing exposure to airborne particles. Furthermore, pneumatic conveying systems can be designed for both low and high-pressure operations, allowing flexibility in handling different powder characteristics and distances. The ability to transport powder in a continuous or batch mode provides operational versatility, enabling seamless integration with existing production lines or storage facilities.
Bentonite powder pneumatic conveying is widely used in various industrial sectors, each with specific requirements that the technology addresses effectively. In the mining and mineral processing industry, it is employed to transport bentonite used as a flocculant or binder in ore processing. The construction industry utilizes bentonite powder for soil stabilization and as a component in cement and concrete mixtures, where the system ensures consistent mixing and delivery. The paper and pulp industry relies on bentonite as a filler or coating agent, and pneumatic conveying facilitates its precise application in production processes. Additionally, in the water treatment sector, bentonite is used for sludge dewatering and filtration, and the technology enables efficient transport of the powder to treatment facilities. Each of these applications benefits from the controlled and hygienic nature of pneumatic conveying, ensuring that the bentonite powder remains in optimal condition throughout the handling process.
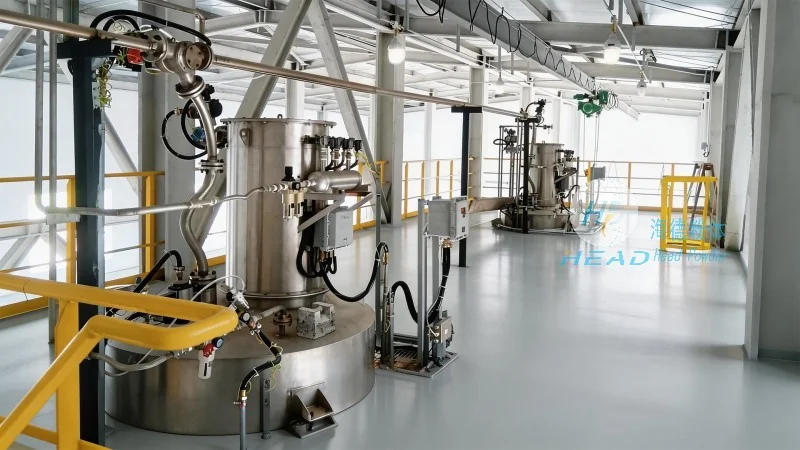
Successfully implementing a bentonite powder pneumatic conveying system requires careful consideration of several operational factors to maximize efficiency and minimize downtime. First, the properties of the bentonite powder must be thoroughly analyzed, including particle size distribution, moisture content, and bulk density, as these characteristics directly impact the system's design and performance. Proper sizing of the hopper and feeder is essential to prevent bridging or agglomeration, which can lead to blockages in the pipeline. The air velocity must be optimized to ensure complete suspension of the powder particles, avoiding excessive velocity that could cause wear on the system components or insufficient velocity that results in clogging. Regular maintenance of the blower, filters, and pipeline is crucial to maintain system efficiency and prevent contamination. Additionally, monitoring the system's pressure and flow rates provides early detection of potential issues, allowing timely intervention and ensuring continuous operation.
Bentonite powder pneumatic conveying is a sophisticated and efficient technology that addresses the unique challenges of handling fine, dusty materials. By leveraging air pressure to transport the powder, this method offers significant advantages in terms of safety, purity, and operational flexibility. Shandong HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, provides comprehensive solutions for bentonite powder pneumatic conveying systems tailored to the specific needs of various industries. From system design and installation to maintenance and support, the company ensures that clients achieve optimal performance and reliability in their material handling operations. With a focus on quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted partner for industries seeking advanced solutions for bentonite powder transportation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top