For industrial applications involving the handling and transportation of magnesium silicate powders, specialized conveying systems are essential to ensure efficiency, safety, and reliability. This article explores the fundamental principles behind magnesium silicate powder handling systems, as well as the key working scene characteristics that define their operational effectiveness.
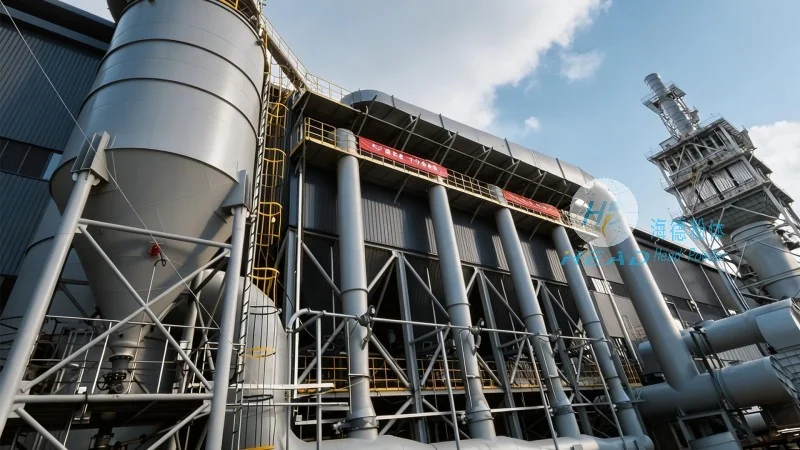
Magnesium silicate, commonly used in various industrial processes such as refractory production, construction materials, and chemical manufacturing, presents unique challenges during material handling due to its fine particle size and cohesive properties. Traditional methods like manual shoveling or basic pneumatic conveying often fall short in maintaining consistent flow and preventing material degradation. To address these challenges, advanced powder handling systems have been developed, incorporating technologies tailored to the specific characteristics of magnesium silicate powders.
The primary principle of magnesium silicate powder handling systems is to create a controlled environment that minimizes particle attrition, agglomeration, and loss during transport. Key components typically include feed hoppers, rotary valves, conveying lines, and discharge mechanisms, all designed to handle the material's flow characteristics. The system operates by drawing the powder from the source, transporting it through a sealed pipeline, and delivering it to the target location. This closed-loop design helps maintain material integrity and reduces contamination risks. Advanced systems may incorporate features like air classifiers or cyclones to separate oversized particles or moisture, ensuring the delivered material meets quality specifications.
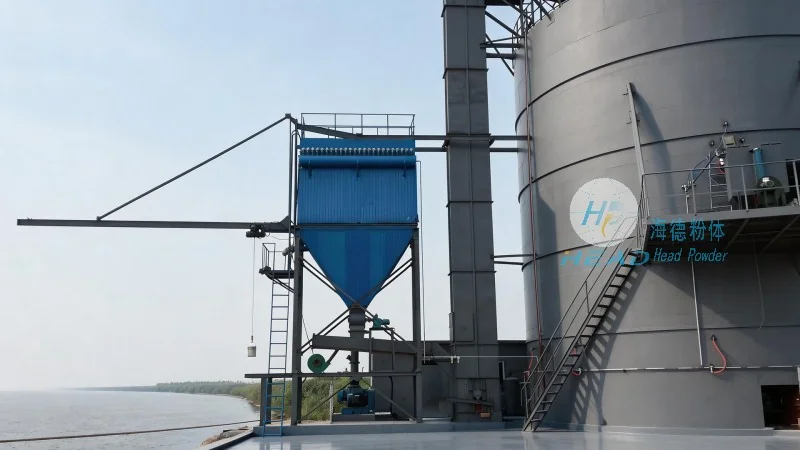
The working scene characteristics of magnesium silicate powder handling systems are tailored to meet the demands of diverse industrial environments. These systems are designed to handle high volumes of material while maintaining low maintenance requirements and energy efficiency. Key operational advantages include:
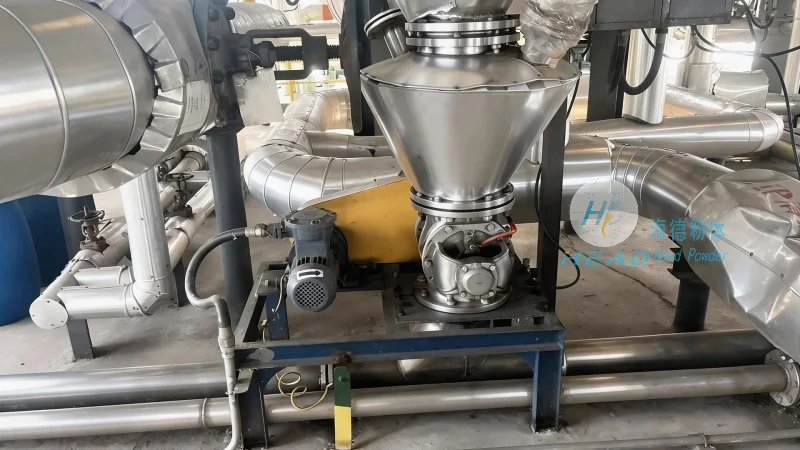
Magnesium silicate powder handling systems are widely used in several industrial sectors. In the refractory industry, these systems efficiently transport raw materials to production lines, ensuring consistent quality in the final products. In construction material manufacturing, they facilitate the delivery of magnesium silicate-based additives to mixing and processing equipment. Additionally, in chemical processing plants, the systems help manage the handling of magnesium silicate powders used as catalysts or fillers, supporting precise dosing and process control. The systems are also applicable in pharmaceutical and food processing industries where material purity and contamination control are critical.
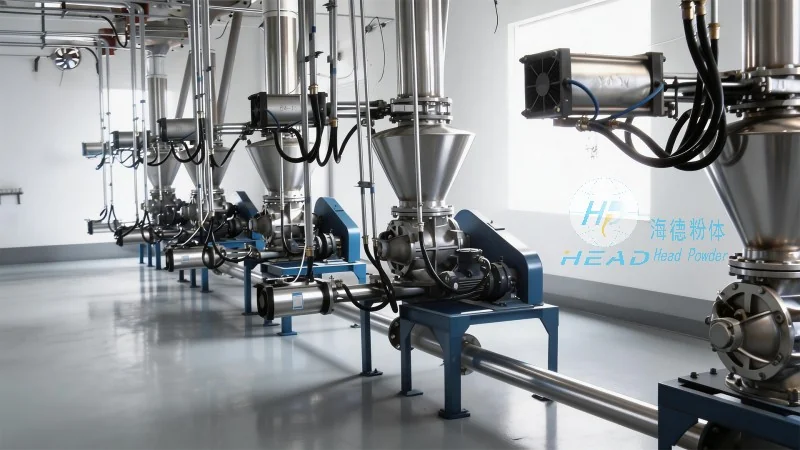
HeadPowder, a leading provider of advanced powder handling solutions, specializes in designing and manufacturing systems tailored to the unique needs of magnesium silicate powder applications. With a focus on innovation and customer-centric engineering, the company has established itself as a trusted partner in the industry. HeadPowder's systems are engineered to deliver superior performance, reliability, and cost-effectiveness, helping clients optimize their material handling processes. The company's R&D team continuously researches new technologies to improve system efficiency and adapt to evolving industry standards.
HeadPowder is headquartered in Shandong, China, with a dedicated facility equipped to support research, development, and manufacturing of powder handling systems. The company's commitment to quality and customer satisfaction is reflected in its state-of-the-art production processes and rigorous quality control measures. For inquiries or further information about magnesium silicate powder handling systems, please contact HeadPowder directly.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top