Multi-functional pneumatic conveying systems represent a sophisticated solution for material handling in various industrial applications. These systems are designed to transport bulk materials efficiently through the use of air or other gases as the conveying medium. Understanding the working principles and key features of such systems is crucial for selecting the right equipment for specific operational needs.
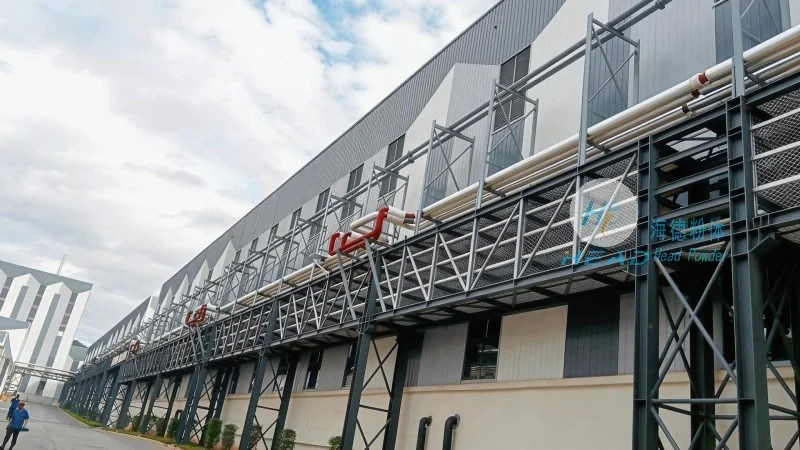
At the core of multi-functional pneumatic conveying systems lies the principle of transporting solid particles through a pipeline using a pressurized or vacuum air stream. The system operates by creating a flow of air that carries the material particles from the source to the destination. There are primarily two types of pneumatic conveying systems: pressure systems and vacuum systems. Pressure systems use positive pressure to push the material through the pipeline, while vacuum systems use negative pressure to draw the material into the system. Multi-functional systems often combine elements of both, allowing for flexibility in handling different material characteristics and process requirements.
The process begins with the material being fed into the conveying line, either by a hopper or a feeder. The air is then introduced, creating a mixture of air and solid particles known as a slurry or a two-phase flow. The velocity of the air stream must be sufficient to overcome the gravitational and frictional forces acting on the particles, ensuring stable transport. The system's design, including the size of the pipeline, the air velocity, and the pressure differentials, is critical in determining the efficiency and capacity of the conveying operation. Advanced multi-functional systems may incorporate features like variable speed drives, pressure regulators, and particle separation units to enhance performance and adaptability.
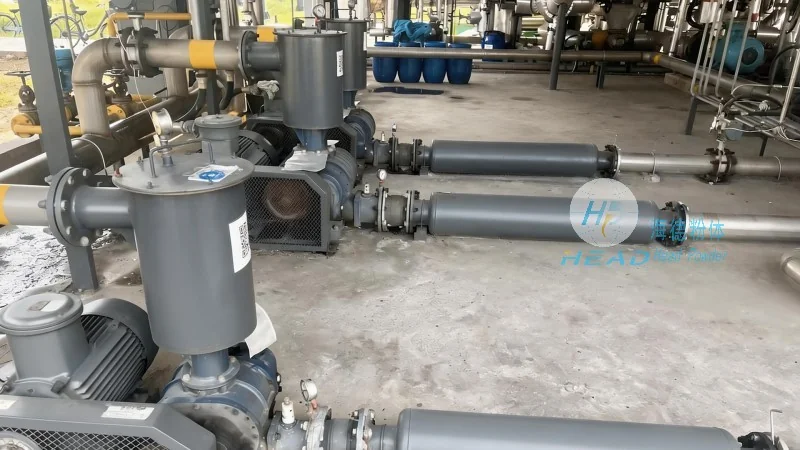
Multi-functional pneumatic conveying systems are distinguished by several key features that make them versatile and efficient for diverse applications. One of the primary features is their ability to handle a wide range of materials, from fine powders to bulk solids, with varying particle sizes and densities. This versatility is achieved through adjustable conveying parameters, such as air pressure and flow rate, which can be tailored to the specific material properties. Another significant feature is the system's flexibility in terms of layout and installation. Unlike traditional mechanical conveyors, pneumatic systems can be installed in complex or irregular spaces, with the pipeline routed around obstacles, making them suitable for facilities with limited space or challenging layouts.
Efficiency and energy savings are also notable features of these systems. By using air as the conveying medium, the system minimizes mechanical wear and reduces the need for maintenance compared to traditional belt or screw conveyors. Additionally, the ability to operate in a closed system helps in controlling dust emissions and maintaining a clean working environment, which is essential for industries where dust control is a regulatory requirement. The systems also offer high throughput capabilities, with some models capable of transporting materials at rates of several tons per hour, making them suitable for high-volume production lines.
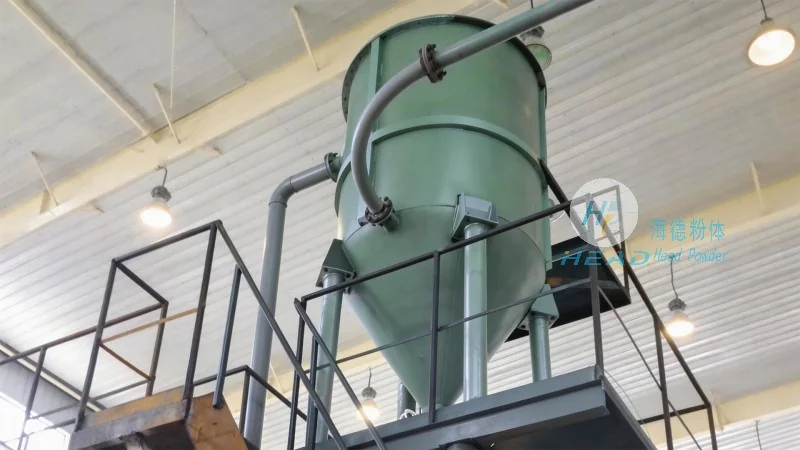
Another important feature is the system's adaptability to different process stages. Multi-functional pneumatic conveying systems can be integrated into existing production lines or used as standalone units for material transfer. They can be configured to handle both bulk material transport and fine powder handling, providing a comprehensive solution for various material handling challenges. The systems also support remote monitoring and control, allowing operators to adjust parameters in real-time and optimize performance based on operational conditions.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced pneumatic conveying systems. With a focus on innovation and quality, the company has established itself as a trusted partner in the material handling industry. HeadPowder's headquarters and main operations are located in Shandong, China, where the company leverages its local expertise and resources to develop cutting-edge solutions for global clients. The company's commitment to research and development ensures that its products meet the evolving needs of modern industrial applications, providing reliable and efficient material handling solutions for various sectors, including food, pharmaceuticals, chemicals, and manufacturing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top