HeadPowder Engineering, a leading provider in the field of powder handling solutions, specializes in the design, manufacturing, and implementation of advanced polyurethane powder conveying systems. These systems are engineered to efficiently transport various types of powders from one location to another within industrial settings. The following content delves into the fundamental principles behind these systems and highlights the key characteristics that define their performance across different working scenarios.
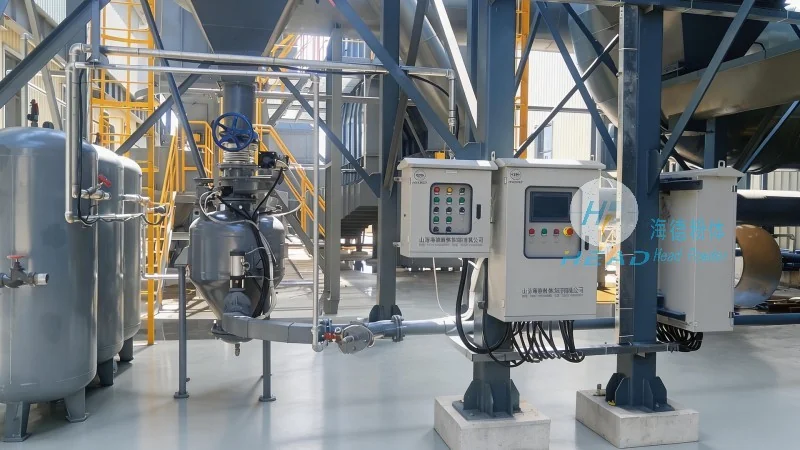
Polyurethane powder conveying systems are sophisticated equipment designed to move bulk powders from one location to another within industrial settings. At the heart of these systems lies a combination of mechanical and pneumatic components that work in tandem to ensure smooth and efficient material transfer. The systems are typically composed of several key elements, including a hopper for material storage, a conveying line (often made of durable polyurethane tubing), a control unit for regulating flow and pressure, and a discharge mechanism for delivering the material to its final destination. The choice of polyurethane as the primary material for the conveying components is deliberate, as it offers exceptional resistance to abrasion, corrosion, and impact, making it ideal for handling a wide range of powders, from fine to coarse, and even those with high moisture content or aggressive chemical properties.
The operational principle of a polyurethane powder conveying system revolves around the use of air pressure or vacuum to move the powder through the conveying line. In a typical pneumatic conveying setup, the system generates a pressure differential between the inlet and outlet of the conveying line. This differential causes the powder to be drawn into the line and propelled forward by the moving air stream. The polyurethane tubing, with its smooth interior surface, minimizes friction and particle attrition, ensuring that the material is transported without degradation. The control unit plays a critical role in maintaining consistent flow rates and pressure levels, which are essential for preventing blockages and ensuring uniform delivery. Additionally, the system may incorporate features such as pulse-jetting or rotary valves to enhance material flow and prevent clogging, further optimizing the conveying process.
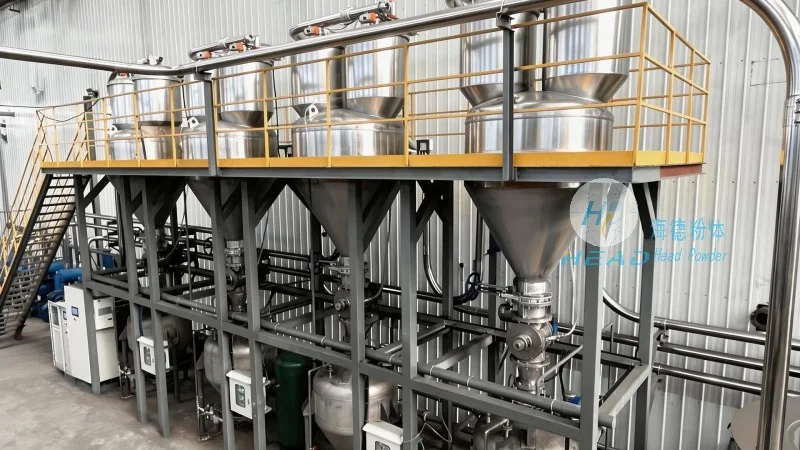
The working scene characteristics of polyurethane powder conveying systems are shaped by their adaptability to various industrial environments and operational requirements. These systems are designed to operate in a wide range of conditions, from standard factory settings to more specialized applications such as food processing, pharmaceutical manufacturing, and chemical processing. The key characteristics that define their performance in these scenarios include high efficiency, low maintenance, and compliance with industry-specific standards. For instance, in food processing facilities, the systems are often constructed with sanitary-grade polyurethane components that meet strict hygiene regulations, ensuring that the conveyed powders remain free from contamination. In pharmaceutical applications, the systems are equipped with GMP-compliant features, such as easy-to-clean surfaces and sealed connections, to maintain product integrity and regulatory compliance. Similarly, in chemical processing industries, the systems are engineered to handle aggressive chemicals and abrasive powders, with reinforced polyurethane components that resist corrosion and wear.
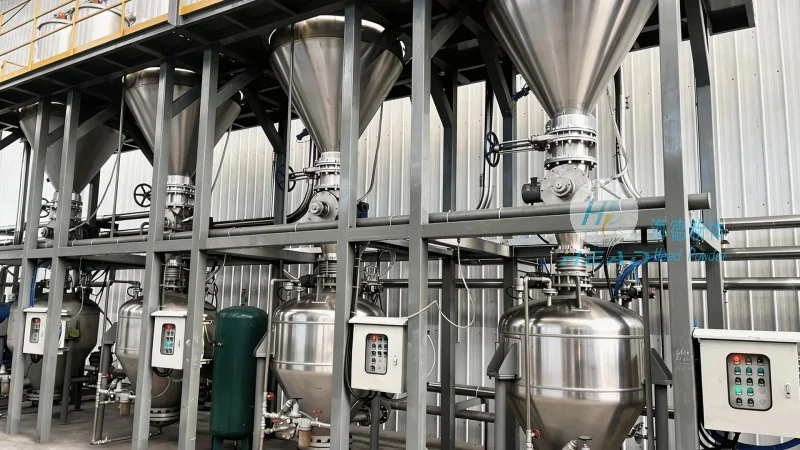
Polyurethane powder conveying systems find extensive application across multiple industries, each with unique demands and operational constraints. In the chemical industry, these systems are used to transport raw materials, intermediates, and finished products, such as pigments, catalysts, and polymers. The systems' ability to handle abrasive and corrosive powders makes them suitable for processes that involve high-temperature or high-pressure conditions. In the food and beverage sector, the systems are employed to convey ingredients like flour, sugar, and spices, where hygiene and product purity are paramount. The use of food-grade polyurethane components and sealed systems ensures that the conveyed powders meet stringent safety standards. In the pharmaceutical industry, the systems are critical for transporting active pharmaceutical ingredients (APIs) and excipients, where precision and contamination control are non-negotiable. The systems' GMP-compliant design and minimal particle generation help maintain the quality and safety of pharmaceutical products. Furthermore, in the agricultural sector, polyurethane powder conveying systems are utilized to transport fertilizers, pesticides, and other agricultural chemicals, supporting efficient farming operations.
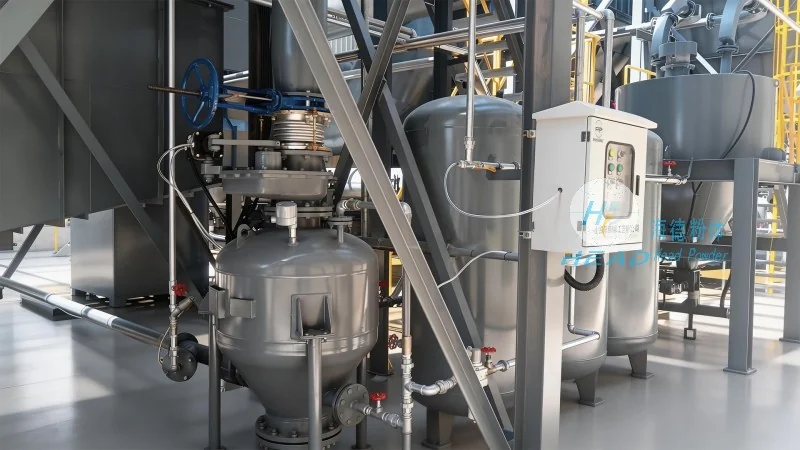
The advantages of polyurethane powder conveying systems are evident in their ability to deliver reliable performance across diverse industrial environments. One of the primary benefits is their high efficiency in material handling, as they can transport large volumes of powder at consistent speeds, reducing downtime and increasing productivity. The systems also offer low maintenance requirements, as the polyurethane components are durable and resistant to wear, minimizing the need for frequent replacements or repairs. Additionally, the systems are designed for easy integration into existing production lines, with modular components that can be customized to fit specific operational needs. Another key advantage is their adaptability to different powder types and sizes, allowing them to handle a wide range of materials without the need for extensive modifications. The systems also provide flexibility in terms of layout and installation, as they can be configured to fit tight spaces or complex production layouts. Finally, the systems contribute to improved safety in industrial settings, as they eliminate the need for manual handling of powders, reducing the risk of dust explosions and occupational hazards.
HeadPowder Engineering's polyurethane powder conveying systems represent a sophisticated solution for efficient and reliable powder handling in various industrial applications. By leveraging advanced materials and engineering principles, these systems offer superior performance, durability, and adaptability across diverse working scenarios. As industries continue to evolve and demand higher standards of efficiency and safety, the role of polyurethane powder conveying systems will remain critical in supporting production processes. With a commitment to innovation and quality, HeadPowder Engineering remains at the forefront of providing tailored powder handling solutions that meet the evolving needs of modern industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top