For industrial applications that require efficient and reliable material handling, vacuum powder pneumatic conveying systems offer a versatile solution. These systems are designed to transport bulk powders and granular materials over short to medium distances, providing a clean and low-maintenance method compared to traditional mechanical conveying equipment. The core of such a system lies in its ability to create a vacuum to draw material from a source to a destination, making it ideal for applications in pharmaceuticals, food processing, chemical manufacturing, and other industries where material purity and contamination control are critical.
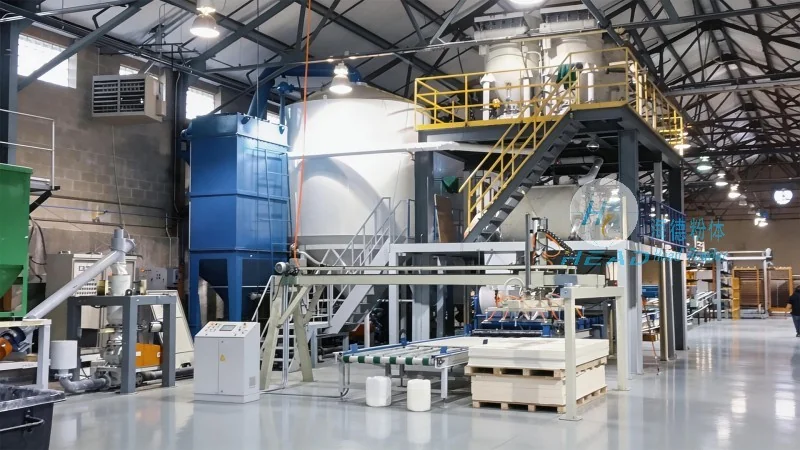
The fundamental working principle of a vacuum powder pneumatic conveying system involves the use of a vacuum pump to generate a pressure differential between the material source and the conveying line. When the system is activated, the vacuum pump draws air and material particles from the source container (such as a hopper or silo) into the conveying pipeline. The material is then carried by the airflow through the system to the discharge point, where the material is deposited. The system typically includes components like a vacuum pump, a filter to separate material from air, a hopper for material storage, and a discharge valve for controlled material release. The entire process is controlled by a system of valves and a control panel, ensuring precise and automated operation. The vacuum created by the pump ensures that the material is drawn efficiently, with minimal air leakage and optimal material flow rates. This principle allows for the gentle handling of delicate powders, preventing agglomeration or degradation during transport. For instance, in pharmaceutical applications, the system’s ability to maintain a sterile environment is crucial, as the vacuum pump and filter are designed to prevent external contamination. The pipeline is often made of stainless steel or other inert materials to further ensure material purity. The control panel allows operators to adjust the vacuum level and flow rate in real-time, adapting to different material characteristics and system requirements.
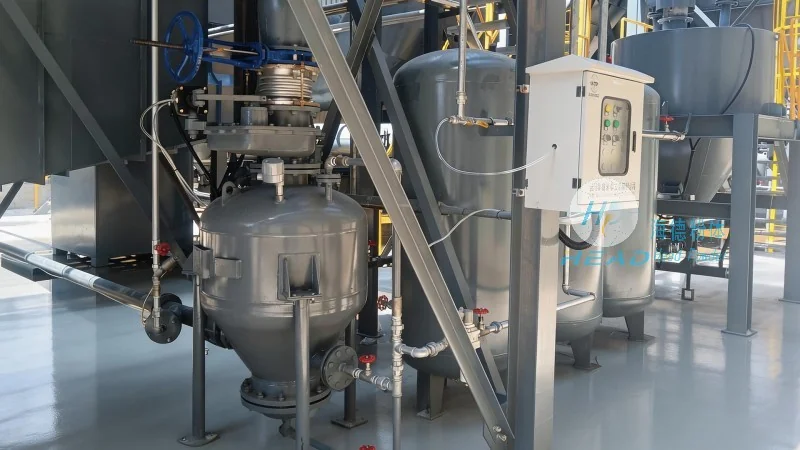
Vacuum powder pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. (headpowder) are characterized by several key features that enhance their performance and suitability for various industrial needs. One of the primary advantages is the ability to handle a wide range of powder types, including fine, cohesive, and abrasive materials, without the need for mechanical components that could cause wear or contamination. The system’s design minimizes material contact with metal surfaces, reducing the risk of cross-contamination, which is essential in industries like pharmaceuticals and food processing. Additionally, the vacuum operation allows for a clean and dust-free environment, as the material is contained within the pipeline and filtered air is returned to the system or released safely. Another significant feature is the flexibility in system layout, as the conveying line can be configured to follow existing facility layouts, reducing installation complexity and costs. The systems are also equipped with advanced control systems that enable real-time monitoring of material flow rates, pressure, and vacuum levels, ensuring optimal performance and preventing system failures. Furthermore, the low maintenance requirements of these systems contribute to long-term cost savings, as they have fewer moving parts compared to mechanical conveyors and require less frequent servicing. Safety features such as overpressure and vacuum alarms are integrated into the control panel, providing immediate alerts if system parameters deviate from normal operating ranges. This proactive approach to safety ensures that the system operates within safe limits and prevents potential hazards.
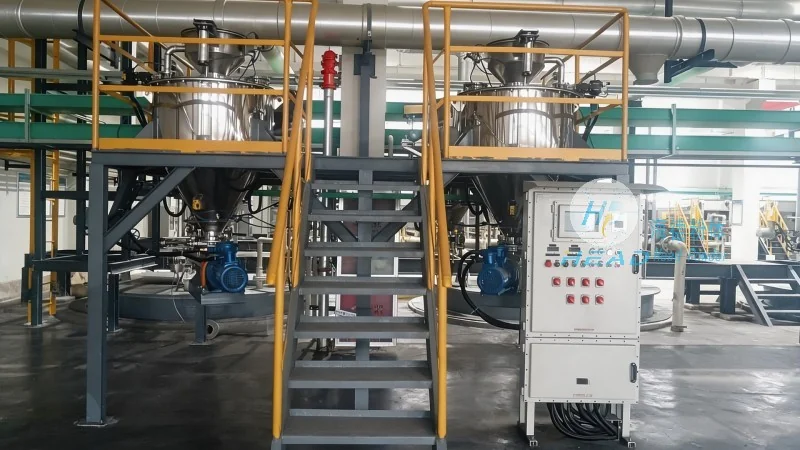
The versatility of vacuum powder pneumatic conveying systems makes them suitable for a variety of applications across different industries. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high purity standards, ensuring that the material remains free from contamination and degradation. In food processing, they handle ingredients like flour, sugar, and spices, maintaining the quality and safety of the final products. Chemical manufacturers utilize these systems for transporting powders such as catalysts, pigments, and reagents, where precise control over material handling is crucial. The benefits of using vacuum powder pneumatic conveying systems extend beyond material handling efficiency. The systems contribute to improved workplace safety by reducing dust exposure and eliminating the need for manual handling of bulk materials. They also enhance productivity by automating the material transport process, allowing for continuous operation without the need for frequent stops or manual adjustments. The energy efficiency of these systems, particularly with modern vacuum pump technologies, further reduces operational costs and environmental impact. Overall, the integration of vacuum powder pneumatic conveying systems into industrial processes leads to enhanced operational efficiency, product quality, and compliance with industry regulations. For example, in a food processing plant, the system can be integrated with existing production lines to transport raw materials directly to processing equipment, reducing downtime and increasing throughput. In a pharmaceutical facility, the system ensures that raw materials are handled in a sterile environment, meeting stringent regulatory requirements for drug manufacturing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top