For industrial applications involving the handling of nickel sulfate powder, a pneumatic conveying system offers an efficient and reliable method for material transport. This technology is particularly valuable in processes where dust control, material integrity, and operational flexibility are critical. The system operates by using a stream of air to transport the powder through a pipeline network, eliminating the need for mechanical components like conveyors or buckets that might cause material degradation or contamination.
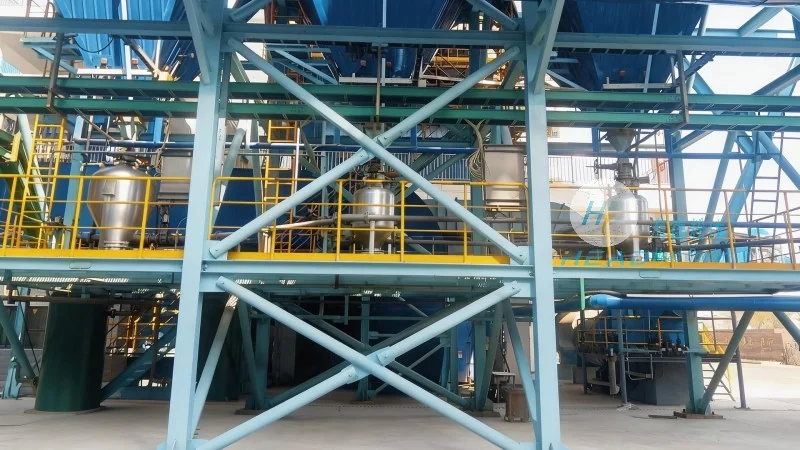
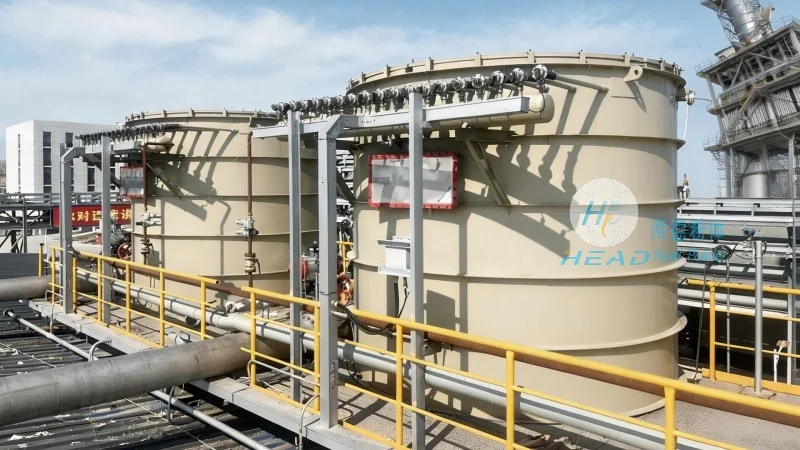
The core mechanism of a nickel sulfate powder pneumatic conveying system involves the generation of a high-velocity air stream within a pipeline. The system typically includes a blower or compressor that supplies the necessary air pressure and volume. As the air flows through the pipeline, it draws the nickel sulfate powder particles into the stream, creating a suspension of the material. The air velocity is maintained at a level sufficient to keep the powder particles suspended and prevent settling or blockages. The system may use either positive pressure (where air is forced into the pipeline) or negative pressure (where air is drawn out), depending on the specific application and layout requirements. The process ensures that the powder is transported from the source to the destination without direct contact with other surfaces, preserving the material's quality and reducing the risk of contamination.
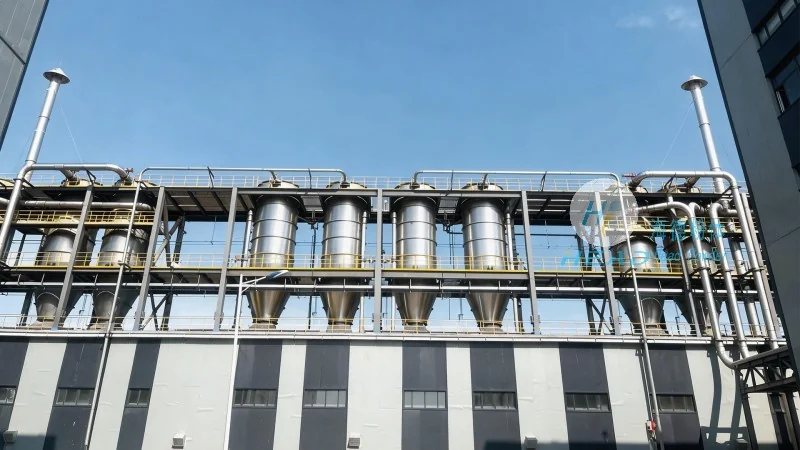
Several distinctive features make the pneumatic conveying system an ideal choice for handling nickel sulfate powder. Firstly, it provides excellent dust control, as the material is contained within the pipeline and the air stream, minimizing the release of fine particles into the environment. This is crucial for maintaining compliance with environmental regulations and ensuring workplace safety. Secondly, the system offers high material handling capacity, capable of transporting large volumes of powder efficiently over long distances. The flexibility of the system allows for easy integration into existing industrial setups, with the ability to add or modify pipeline sections as needed. Additionally, the system is designed to handle the specific properties of nickel sulfate, such as its fine particle size and potential for agglomeration, by optimizing the air velocity and pipeline design to prevent blockages and ensure smooth flow. The system also provides consistent material flow rates, which is essential for maintaining process stability and product quality in downstream operations.
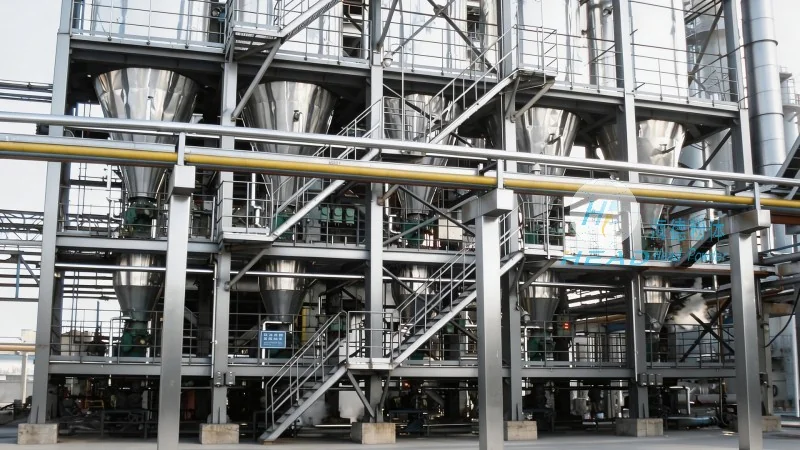
When implementing a nickel sulfate powder pneumatic conveying system, several factors must be considered to ensure optimal performance. The system's design must account for the powder's particle size distribution, moisture content, and flow characteristics to prevent issues like caking or bridging in the pipeline. Proper air flow management is critical to maintain the suspension of the powder and avoid pressure drops that could lead to system inefficiencies. The system also benefits from low maintenance requirements compared to traditional mechanical conveying systems, as there are fewer moving parts that could wear out or require replacement. This reduces operational costs and downtime. Furthermore, the system's ability to handle the material in a closed environment enhances product purity, which is vital for applications where the nickel sulfate is used in pharmaceuticals, batteries, or other high-purity industries. The overall benefits of the system include improved safety, reduced material loss, and enhanced process efficiency, making it a preferred solution for industrial powder handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top