Compound fertilizer powder pneumatic conveying systems are crucial in modern agricultural and industrial applications, designed to efficiently transport bulk powder materials like compound fertilizers. These systems offer a reliable and efficient solution for moving large volumes of fertilizer from production facilities to storage or distribution points. The technology behind these systems combines pneumatic principles with advanced engineering to ensure safe, clean, and high-performance material handling. This article explores the working principle and key features of such systems, highlighting their importance in optimizing fertilizer processing and logistics.
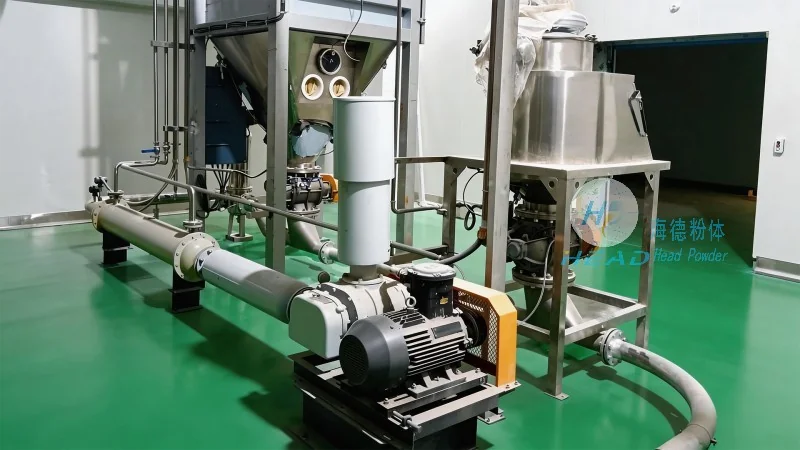
The core of a compound fertilizer powder pneumatic conveying system lies in its ability to use air as a medium to transport solid particles. The system typically operates under either positive pressure (pressure conveying) or negative pressure (suction conveying), depending on the application requirements and system design. In positive pressure systems, a blower or compressor generates high-pressure air that pushes the fertilizer particles through a network of pipes. The air and powder mixture travels through the pipeline, with the air providing the necessary force to move the material. In negative pressure systems, a vacuum pump creates a low-pressure environment that draws the powder into the system, often used for short-distance or low-volume transfers.
Key components of the system include a feeder, which meters and feeds the fertilizer into the conveying line; a conveying pipeline, which transports the material; a separator, which separates the air from the powder at the end of the line; and a filter or cyclone to capture any fine particles and return them to the system. The feeder ensures consistent material flow, preventing blockages or uneven distribution. The pipeline is usually made of durable materials like stainless steel or plastic, chosen for their resistance to corrosion and wear from the fertilizer particles. The separator uses centrifugal force to separate the air and powder, with the powder being collected and the air either vented or recycled. This closed-loop design minimizes dust emissions and maintains material quality.
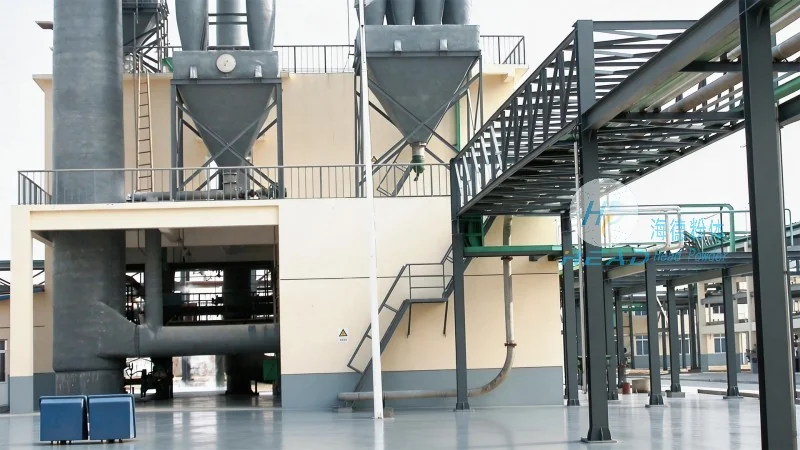
Compound fertilizer powder pneumatic conveying systems offer several advantages that make them ideal for industrial applications. One of the primary benefits is high efficiency, as they can transport large volumes of material quickly and continuously, reducing downtime and increasing production throughput. The systems are also energy-efficient compared to traditional methods like belt conveyors or manual handling, as they use air pressure to move the material rather than mechanical force. This results in lower operational costs and reduced energy consumption.
Another significant feature is the ability to handle a wide range of fertilizer types and particle sizes. Whether dealing with granular, prilled, or powdered fertilizers, the system can be adjusted to accommodate different characteristics. The flexible design allows for customization based on the specific needs of the fertilizer, including moisture content and particle size distribution. This adaptability makes the system suitable for various production scales, from small-scale farms to large industrial fertilizer plants.
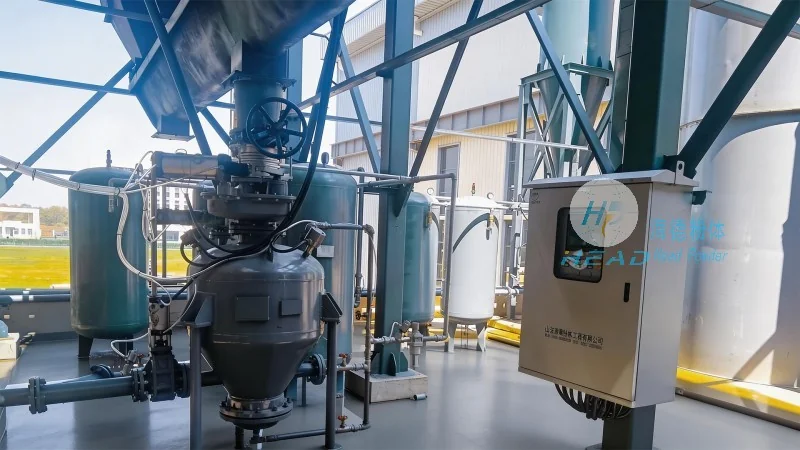
The system also provides a clean and hygienic handling environment, which is critical for maintaining the quality of the fertilizer. By using a closed system with sealed pipes and proper filtration, the risk of contamination from external sources is minimized. This is particularly important for fertilizers that are used in agricultural applications, where purity and consistency are essential for crop growth. Additionally, the system reduces dust generation, improving workplace safety and compliance with environmental regulations.
The compound fertilizer powder pneumatic conveying system is widely used in various stages of the fertilizer supply chain. In production facilities, it efficiently moves raw materials from storage silos to processing equipment, ensuring a steady supply of feedstock. During the manufacturing process, the system transports intermediate products between different processing units, such as from granulation to coating or packaging. At the storage and distribution level, the system moves finished fertilizer from the production line to storage silos or loading areas, facilitating smooth logistics operations.
For agricultural operations, the system can be used to transport fertilizer from storage facilities to application equipment, such as spreaders or applicators. This allows for precise and uniform distribution of nutrients, enhancing crop yields and reducing waste. The system's ability to handle large volumes and operate continuously supports the high demand for fertilizer during planting and maintenance seasons. By integrating the system into the overall logistics plan, companies can improve operational efficiency, reduce labor costs, and enhance overall productivity.
Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China, is a leading manufacturer and supplier of advanced powder handling and conveying systems. With years of experience in the industry, the company specializes in designing and manufacturing customized solutions for various powder materials, including compound fertilizers. HeadPowder's team of engineers and technicians works closely with clients to understand their specific needs and develop tailored systems that meet their operational requirements.
The company's facilities are equipped with state-of-the-art technology and quality control measures to ensure the highest standards of product performance and reliability. HeadPowder provides comprehensive technical support, including installation, commissioning, and maintenance services, to ensure that clients can maximize the benefits of their conveying systems. The company's commitment to innovation and customer satisfaction has earned it a reputation as a trusted partner in the fertilizer and powder handling industry. By leveraging its expertise and advanced engineering capabilities, Shandong HeadPowder Engineering Co., Ltd. continues to deliver high-quality solutions that enhance the efficiency and productivity of its clients' operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top