For industrial applications involving the handling of shredded paper powder, an efficient and reliable conveying system is crucial. The pneumatic conveying system designed specifically for shredded paper powder offers a solution that ensures smooth material transport while maintaining product integrity. This article explores the working principle and key features of such a system, highlighting its benefits for businesses in the paper processing and waste management sectors.
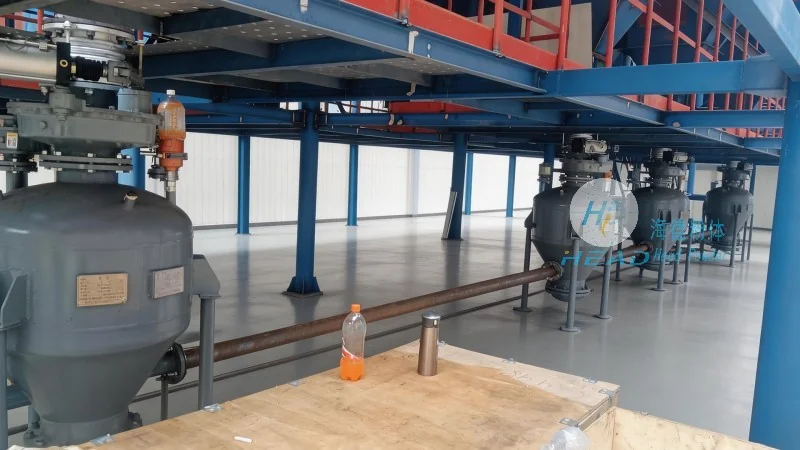
The core of a pneumatic conveying system for shredded paper powder lies in its ability to transport dry, fine particles through a pressurized or vacuum environment. The system typically operates by using air as the conveying medium, which is either supplied under pressure (positive pressure system) or drawn through the system (negative pressure system). In a positive pressure system, a blower or compressor generates compressed air that forces the shredded paper powder from the source (such as a hopper or storage bin) into the conveying line. The air and powder mixture travels through a network of pipes, often with bends and fittings, to the destination point, such as a processing unit or storage silo. The system may include components like rotary air locks, filters, and dust collectors to manage the air flow and prevent material loss or contamination. In the design of this system, Shandong HeadPowder Engineering Co., Ltd. (headpowder) focuses on optimizing the air flow and particle movement to ensure efficient and reliable transport. The system is engineered to handle the specific characteristics of shredded paper powder, including its fine particle size, low bulk density, and potential for static electricity. The design of the system ensures that the powder is conveyed without clogging or degradation, maintaining the quality of the material throughout the process.
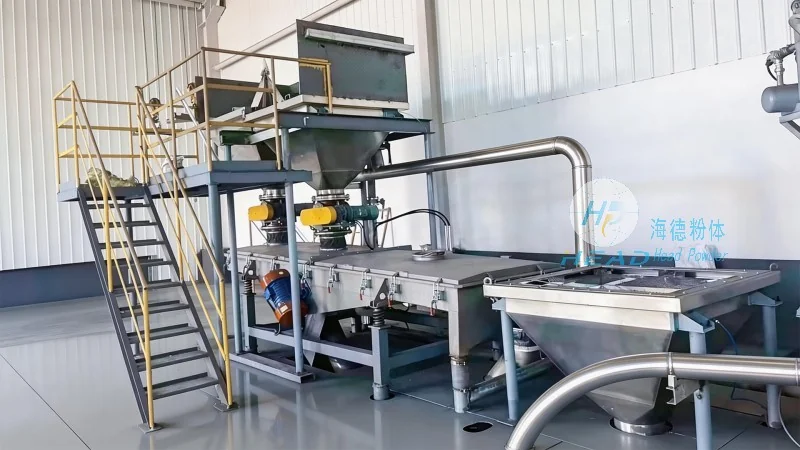
Several key features make the pneumatic conveying system for shredded paper powder an effective choice for industrial applications. Firstly, the system offers high efficiency in material transport, allowing for continuous and uninterrupted operation. This is particularly important for businesses that require a steady flow of shredded paper powder to their processing units. The system's ability to handle fine particles without clogging is a significant advantage, as it reduces downtime and maintenance costs. Additionally, the system is designed to maintain the integrity of the shredded paper powder, preventing it from being damaged or mixed with contaminants during transport. This is crucial for applications where the quality of the powder is critical, such as in the production of paper products or in waste management processes. The system also provides flexibility in terms of layout, as it can be configured to fit various plant designs and operational requirements. It can be integrated with existing equipment and adapted to different conveying distances and heights. Furthermore, the system is equipped with safety features to ensure proper operation and protect personnel from dust exposure and other hazards. These features include dust collection systems, pressure relief valves, and automatic shut-off mechanisms. The system's energy efficiency is another notable feature, as it minimizes energy consumption compared to traditional methods like bucket elevators or belt conveyors. This not only reduces operational costs but also contributes to environmental sustainability by lowering carbon emissions.
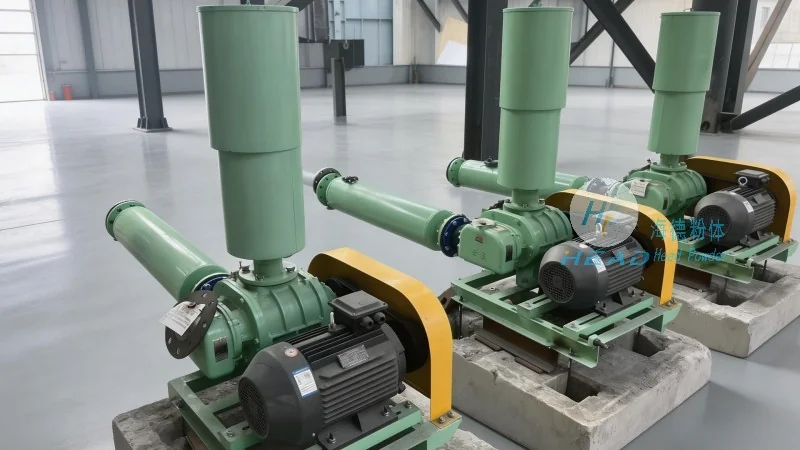
Implementing a pneumatic conveying system for shredded paper powder brings numerous benefits to businesses operating in the paper processing and waste management industries. The primary advantage is the improvement in operational efficiency, as the system allows for seamless material transport, reducing the time and labor required for manual handling. This leads to increased productivity and reduced production costs. The system also enhances product quality by ensuring that the shredded paper powder is conveyed without degradation or contamination, which is essential for maintaining the quality of the final products. For waste management companies, the system helps in the efficient handling of shredded paper, facilitating recycling processes and reducing the environmental impact of waste disposal. The system's reliability and low maintenance requirements contribute to long-term cost savings, as businesses can minimize downtime and repair expenses. Additionally, the system's adaptability allows it to be integrated into existing facilities, making it a viable option for companies looking to upgrade their material handling infrastructure without major disruptions. The environmental benefits of the system, such as reduced energy consumption and lower emissions, align with the growing emphasis on sustainability in industrial operations. This makes the system an attractive choice for businesses committed to eco-friendly practices and regulatory compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top