Barley malt is a critical ingredient in the brewing industry, and efficient material handling systems are essential for ensuring smooth production processes. The equipment designed for transporting barley malt must be reliable, durable, and capable of handling the specific characteristics of this raw material. This article explores the operation process and working principle of a specialized barley malt material handling system, highlighting its key components and how they contribute to optimal performance in industrial settings.
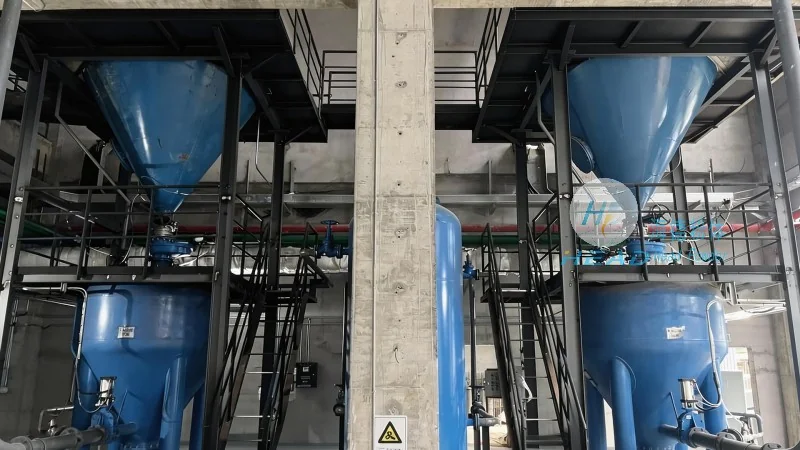
In the brewing sector, the proper handling of barley malt is vital for maintaining product quality and operational efficiency. Traditional methods of transporting malt, such as manual handling or basic conveyor systems, often fall short in meeting the demands of modern breweries. To address these challenges, specialized equipment like the barley malt material handling system from Shandong HeadPowder Engineering Co., Ltd. has been developed. This system integrates advanced technology and robust design to streamline the movement of malt from storage to processing areas, ensuring consistent and safe operation.
The barley malt material handling system consists of several critical components that work in tandem to achieve efficient material transport. The primary components include feed hoppers, conveyor belts, rotary valves, and control panels. Each component plays a specific role in the overall operation, contributing to the system's reliability and performance.
Feed hoppers are designed to store and feed barley malt into the system. They are typically made of stainless steel to prevent contamination and ensure durability. The hoppers are equipped with level sensors that monitor the malt level, preventing overfilling and ensuring a steady supply to the conveyor system. The conveyor belts, often made of food-grade materials, are responsible for transporting the malt horizontally or at slight inclines. These belts are equipped with tensioning mechanisms and drive systems to maintain consistent speed and prevent slippage.
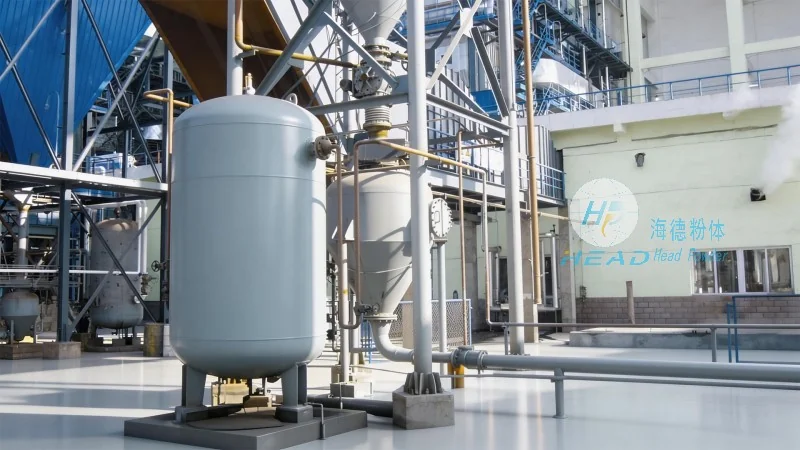
Rotary valves, also known as airlocks, are used to control the flow of malt from the hopper to the conveyor. They act as a seal to prevent dust and air from entering or exiting the system, maintaining a clean and controlled environment. The control panels, located at the operator's station, allow for real-time monitoring and adjustment of the system's parameters, including speed, flow rate, and alarm settings. This integration of components ensures that the system operates smoothly and efficiently, minimizing downtime and maximizing productivity.
The operation of the barley malt material handling system follows a systematic process that begins with the loading of malt into the feed hopper. Once the hopper is filled, the system automatically starts the conveyor belt, which transports the malt to the processing area. The rotary valve regulates the flow rate, ensuring a consistent and controlled delivery of malt to the next stage of the production process. The control panel allows operators to monitor the system's performance, adjust settings as needed, and receive alerts if any issues arise, such as blockages or low material levels.
During operation, the system maintains a clean and hygienic environment, which is crucial for maintaining the quality of the malt and the final product. The stainless steel construction of the components prevents corrosion and makes cleaning easier, adhering to industry standards for food processing. The system is also designed to be energy-efficient, reducing operational costs while maintaining high performance.
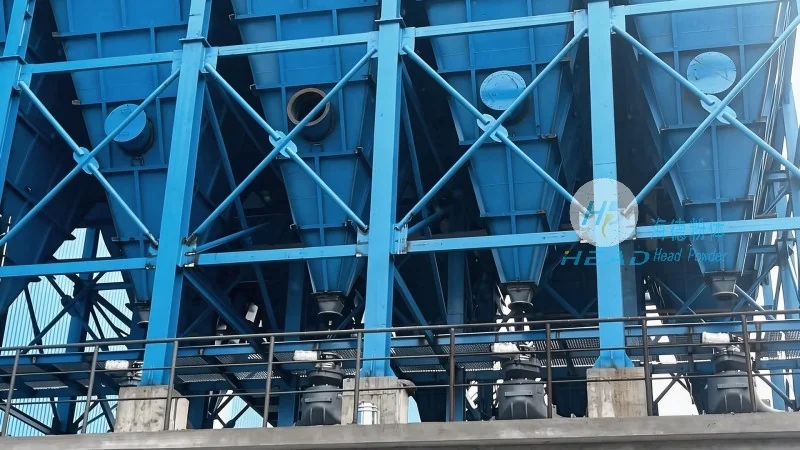
The working principle of the barley malt material handling system is based on mechanical and pneumatic systems that work together to transport the malt. The feed hopper provides the initial storage and feeding mechanism, while the conveyor belt moves the malt horizontally. The rotary valve controls the flow by using a rotating disc that opens and closes to allow the malt to pass through. The control panel manages the entire process, ensuring that all components operate in sync and that the system runs smoothly.
The system operates on the principle of gravity and mechanical force. The hopper's design allows the malt to flow under gravity into the conveyor belt, which then transports it to the processing area. The rotary valve uses air pressure to control the flow, ensuring that the malt moves at a controlled rate. The control panel uses sensors and feedback mechanisms to adjust the speed and flow rate, maintaining optimal performance. This combination of mechanical and pneumatic systems ensures that the barley malt is handled efficiently and safely, minimizing the risk of damage or contamination.
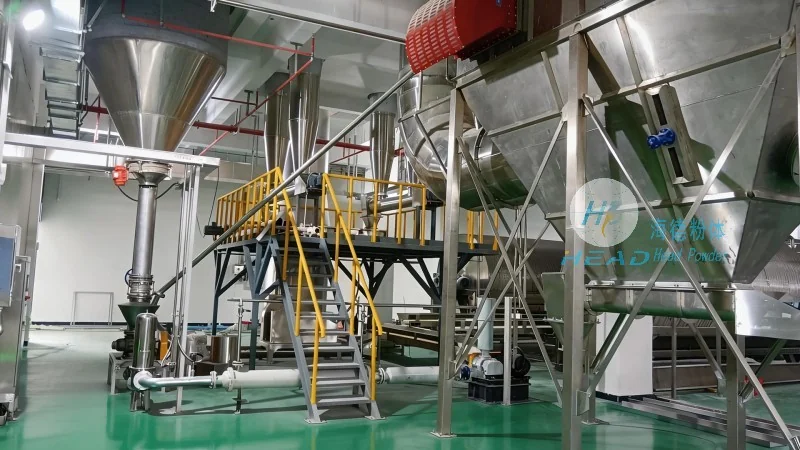
The barley malt material handling system from Shandong HeadPowder Engineering Co., Ltd. offers several benefits that enhance the efficiency and quality of malt handling in breweries. One of the key benefits is the improved productivity, as the system can handle large volumes of malt with minimal manual intervention. The system also ensures consistent flow rates, which is crucial for maintaining the quality of the malt and the final beer product. Additionally, the system is designed for easy maintenance and cleaning, reducing downtime and operational costs.
The system's robust construction and stainless steel components ensure durability and longevity, making it a reliable investment for breweries. The advanced control panel allows for real-time monitoring and adjustment, enabling operators to quickly address any issues that may arise. The system also complies with industry standards for food processing, ensuring that the malt is handled in a hygienic and safe manner. Overall, the barley malt material handling system is an essential piece of equipment for modern breweries, contributing to increased efficiency, product quality, and operational reliability.
In conclusion, the barley malt material handling system from Shandong HeadPowder Engineering Co., Ltd. is a sophisticated piece of equipment designed to streamline the transport of barley malt in brewing operations. Through its integrated components and advanced control systems, the system ensures efficient, safe, and hygienic handling of malt, contributing to the overall productivity and quality of the brewing process. As breweries continue to seek more efficient and reliable solutions for material handling, this system represents a valuable investment for maintaining competitiveness and meeting industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top