High-temperature fly ash material handling systems are essential for industrial facilities that generate fly ash as a byproduct of coal combustion. These systems are engineered to safely and efficiently transport hot fly ash from its source, such as a boiler or furnace, to storage or treatment facilities. The equipment within these systems operates under extreme conditions, requiring robust design and advanced technology to ensure reliability and performance. This article provides a comprehensive overview of the operation process and working principle of high-temperature fly ash material handling systems, highlighting key components and their functions to help readers understand how these systems contribute to the efficient management of fly ash.
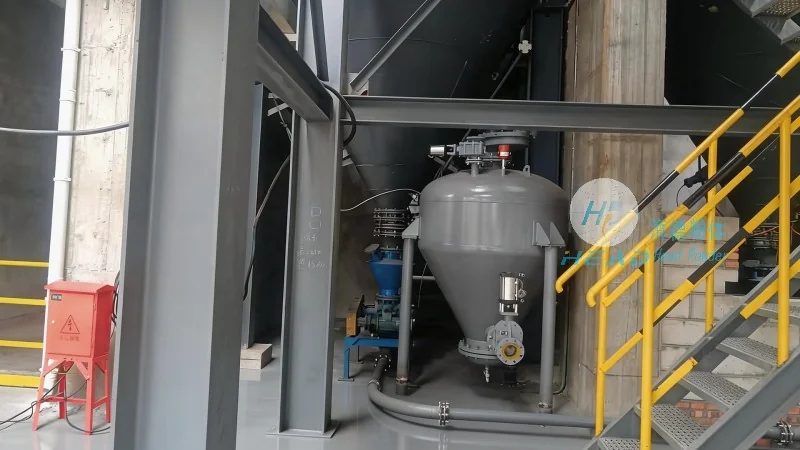
The high-temperature fly ash material handling system typically comprises several interconnected components, each playing a critical role in the overall operation. The primary components include feeders, conveyors, temperature control devices, and dust collection systems. Feeders are responsible for controlling the flow of fly ash from the source, ensuring a consistent and controlled feed rate. This is crucial for maintaining the stability of the conveyor system and preventing blockages or overloading. Conveyors, often in the form of high-temperature belt conveyors or pneumatic systems, transport the fly ash over long distances or to elevated positions. These conveyors are designed to withstand high temperatures and abrasive materials, with materials like stainless steel or heat-resistant alloys used in their construction. Temperature control devices, such as heat exchangers or cooling systems, regulate the temperature of the fly ash to prevent equipment damage and ensure safe handling. For instance, if the fly ash temperature exceeds a certain threshold, cooling mechanisms may be activated to reduce its temperature before further processing. Dust collection systems are integrated to capture and filter particulate matter, maintaining air quality and compliance with environmental regulations. These systems typically use baghouse or electrostatic precipitators to remove dust from the air stream, ensuring that the emissions are within permissible limits.
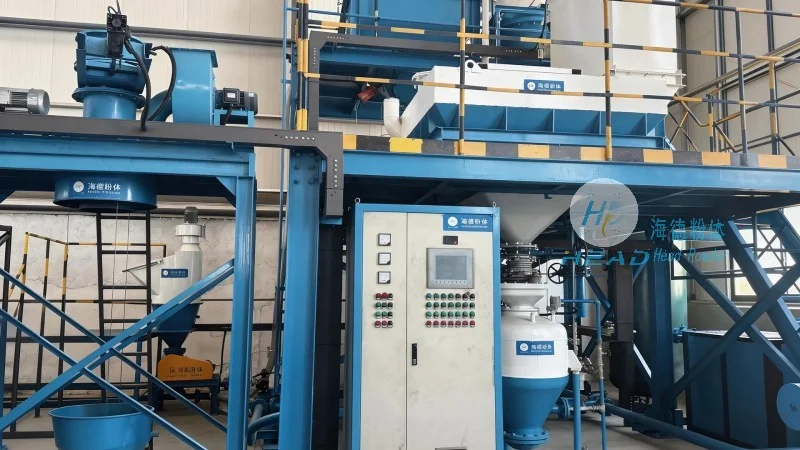
The operation process of the high-temperature fly ash material handling system begins with the collection of fly ash from the combustion source. The fly ash, which is typically at a high temperature (often exceeding 200°C), is first fed into a feeder. The feeder controls the flow rate, ensuring that the material is delivered to the conveyor at a steady pace. The conveyor then transports the fly ash to the next stage of the process, such as storage silos or treatment units. During transport, the system may include temperature monitoring and control mechanisms to maintain the fly ash at an optimal temperature range. For example, if the fly ash is too hot, cooling systems may be activated to reduce its temperature before further processing. The system also incorporates safety features, such as emergency stop mechanisms and temperature sensors, to prevent accidents and ensure the well-being of operators. These safety features are designed to shut down the system in case of abnormal conditions, such as overheating or blockages, protecting both the equipment and personnel from harm.
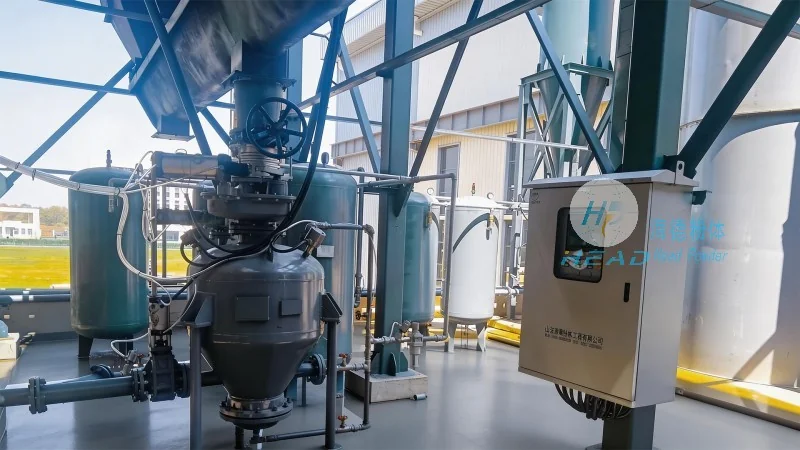
The working principle of the high-temperature fly ash material handling system is based on the principles of material flow and temperature control. The system operates by converting the thermal energy of the fly ash into mechanical energy through the use of conveyors and feeders. The feeders regulate the flow of material, while the conveyors move the material along the designated path. Temperature control is achieved through the integration of cooling systems and heat exchangers, which maintain the temperature of the fly ash within safe operating limits. The system also relies on dust collection technology to capture and filter particulate matter, ensuring that the air quality is maintained at acceptable levels. Overall, the working principle is designed to maximize efficiency, minimize energy consumption, and ensure the safe handling of high-temperature fly ash. The integration of sensors and control systems allows for real-time monitoring and adjustment of the process parameters, ensuring optimal performance and reducing downtime.
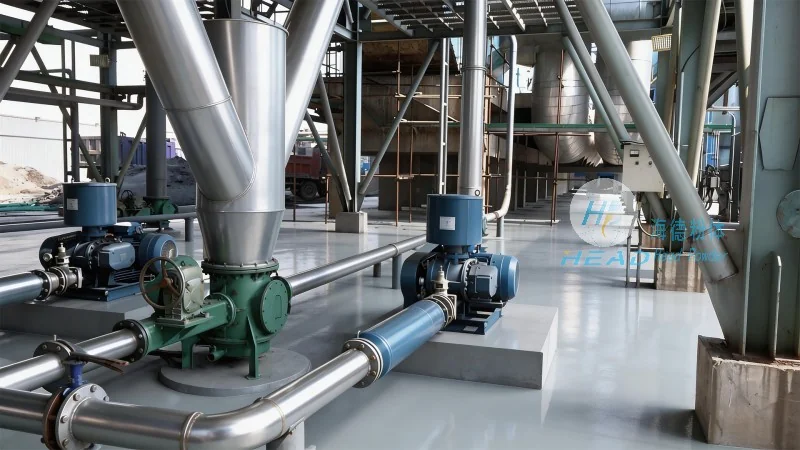
High-temperature fly ash material handling systems offer several advantages over traditional handling methods. These systems are designed to handle the extreme conditions associated with fly ash, such as high temperatures and abrasive properties. The use of robust materials and advanced technology ensures that the equipment can withstand the harsh environment, reducing maintenance costs and increasing operational reliability. Additionally, the systems are designed to be energy-efficient, with features such as variable speed drives and optimized conveyor designs that reduce energy consumption. The integration of dust collection systems also helps to improve air quality and comply with environmental regulations, reducing the environmental impact of the facility. Overall, the high-temperature fly ash material handling system is a critical component in the efficient and safe management of fly ash, contributing to the overall sustainability of industrial operations. By implementing these systems, facilities can improve their operational efficiency, reduce costs, and minimize their environmental footprint, making them a valuable investment for any industrial facility.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top