For industrial applications involving the handling of powdered edible salt, the efficiency and reliability of material transport systems are critical factors that can significantly impact production processes and operational costs. A powdered edible salt pneumatic conveying system is a specialized solution designed to address these challenges by utilizing air as the medium for transporting bulk material. This article will explore the working principle and key features of such a system, providing insights into how it operates and the advantages it offers in the context of food processing and material handling industries.
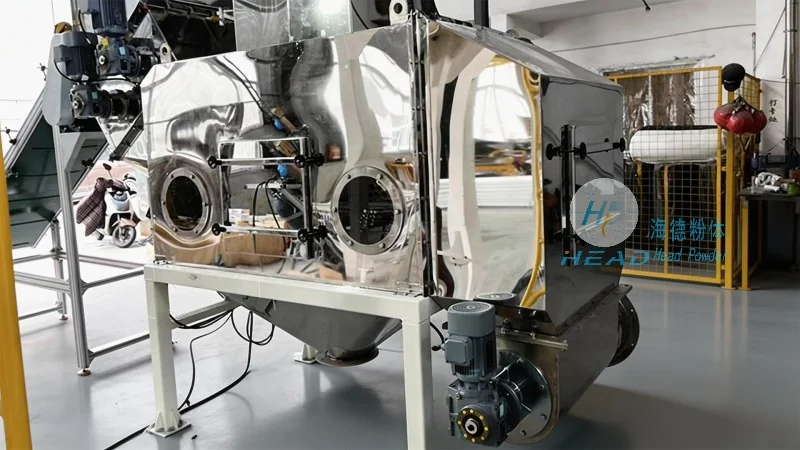
Pneumatic conveying systems are widely used in various industries for the transport of dry powders, granules, and other bulk materials. In the case of powdered edible salt, these systems are engineered to meet stringent hygiene standards while ensuring the integrity and quality of the product. The system typically consists of several components, including a hopper for material storage, a conveyor line, and a control system that manages the air flow and material movement. The design is tailored to handle the specific properties of edible salt, such as its fine particle size, moisture content, and the need for contamination-free handling.
The core mechanism of a powdered edible salt pneumatic conveying system relies on the principles of fluidization and air movement. The process begins with the material being fed from a hopper into a conveying line. As compressed air is introduced into the system, it creates a low-pressure zone that draws the powdered salt into the air stream. This air-salt mixture is then transported through the pipeline to the destination point, such as a storage silo or processing unit. The system may employ different conveying modes, including dilute phase and dense phase, depending on the specific requirements of the application. Dilute phase conveying uses higher air velocities to move the material quickly, while dense phase conveying employs lower velocities and higher air pressure to ensure gentle handling and minimize product degradation.
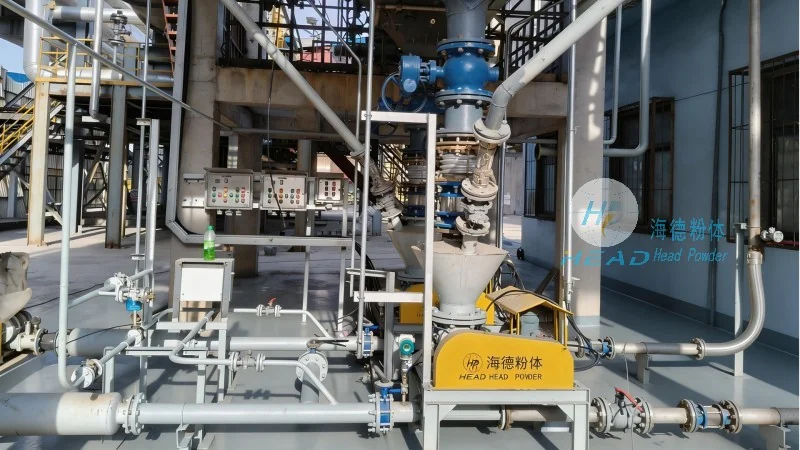
Several key features distinguish a powdered edible salt pneumatic conveying system from traditional methods like belt conveyors or bucket elevators. Firstly, the system offers a completely enclosed and sanitary design, which is essential for food-grade applications. The absence of moving parts in contact with the product reduces the risk of contamination and ensures compliance with regulatory standards. Secondly, the system provides high efficiency in terms of material transport, as it can move large volumes of powdered salt over long distances with minimal energy consumption compared to other methods. This efficiency is particularly beneficial for large-scale production facilities where continuous material flow is required. Thirdly, the system is highly flexible and can be easily integrated into existing production lines. It can handle varying flow rates and can be adjusted to accommodate different batch sizes or production schedules. Additionally, the system is low maintenance, as it has fewer mechanical components that are prone to wear and tear, resulting in lower operational costs and reduced downtime.
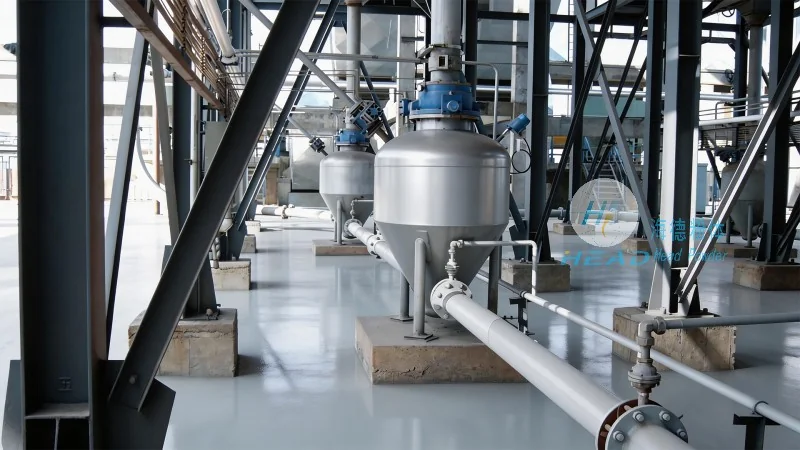
When implementing a powdered edible salt pneumatic conveying system, several factors must be considered to ensure optimal performance and compliance with industry regulations. The system must be designed to handle the specific characteristics of edible salt, such as its particle size distribution, moisture content, and flowability. The air quality is also critical, as any contaminants in the air can affect the purity of the product. Therefore, the system typically includes filtration and drying components to maintain air purity. Furthermore, the system must meet the requirements of food safety regulations, such as those set by the FDA or other relevant authorities. This includes the use of stainless steel components, easy-to-clean surfaces, and proper sealing to prevent cross-contamination. The system is also designed to be compatible with other processing equipment, such as mixers, classifiers, and packaging machines, allowing for seamless integration into the overall production workflow.
In conclusion, a powdered edible salt pneumatic conveying system is a highly effective and reliable solution for the transport of bulk edible salt in industrial settings. By leveraging the principles of pneumatic conveying, the system offers numerous advantages, including high efficiency, low maintenance, and compliance with stringent hygiene standards. The working principle, which involves the use of compressed air to move the material through an enclosed pipeline, ensures gentle handling and minimal product degradation. The key features of the system, such as its sanitary design, flexibility, and low energy consumption, make it an ideal choice for food processing applications. As the demand for efficient and safe material handling solutions continues to grow, the powdered edible salt pneumatic conveying system remains a vital component in modern industrial operations, providing a robust and sustainable approach to handling powdered edible salt.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top