HeadPowder, a leading provider of industrial conveying solutions, specializes in dust and powder handling systems. This article explores the fundamental working principles and key features of these systems, which are essential for efficient material transport in various industrial applications.
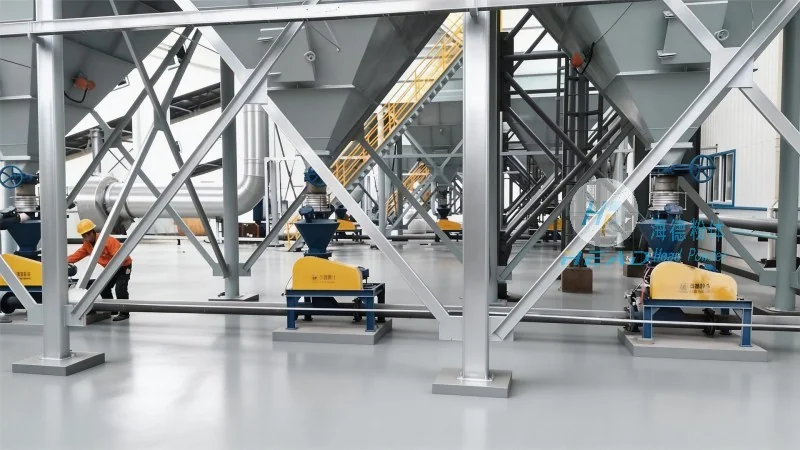
Dust and powder conveying systems are designed to transport dry bulk materials, such as powders, granules, and fine particles, from one location to another. The core working principle typically involves the use of air or mechanical forces to move the material through a pipeline or conveyor. For instance, in pneumatic conveying systems, compressed air is used to create a flow that propels the powder particles through the system. This method is widely used due to its ability to handle fine and abrasive materials without causing excessive wear or contamination. The system comprises several key components, including a material feed hopper, a conveying line, and a discharge mechanism. The feed hopper ensures a consistent supply of material, while the conveying line transports the powder under controlled pressure and flow rates. The discharge mechanism then releases the material at the destination point, often with the aid of a rotary valve or similar device to regulate the output.
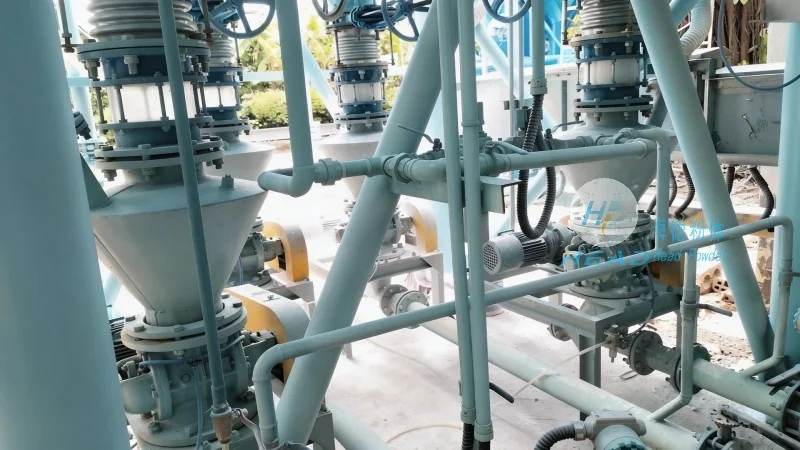
HeadPowder's dust powder conveying systems are characterized by several distinct features that enhance their performance and reliability. One of the primary features is the high efficiency in material transport, which minimizes downtime and maximizes production throughput. The systems are engineered to handle a wide range of material types, from fine powders to coarse granules, ensuring versatility across different industrial sectors. Another notable feature is the enhanced safety and cleanliness. By utilizing enclosed systems and controlled air flow, these conveyors prevent dust emissions and protect both the environment and personnel from exposure to hazardous materials. Additionally, the systems are designed for low maintenance and durability, with robust components that can withstand the rigors of continuous operation. This reliability is crucial for maintaining consistent production quality and reducing operational costs over time.
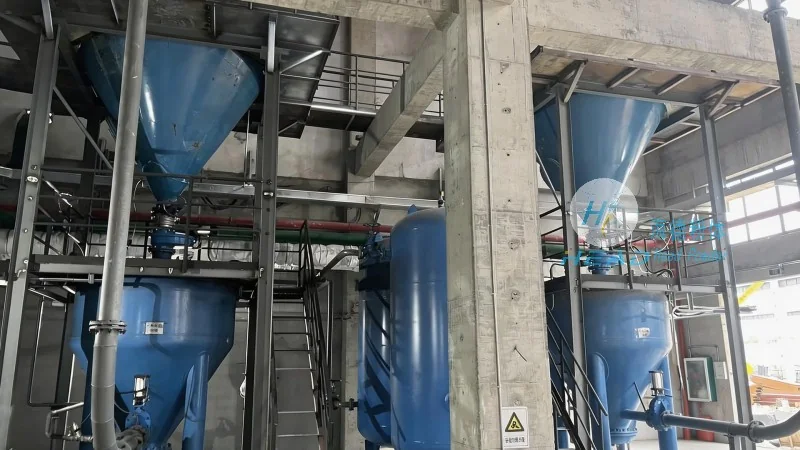
The working principle and features of dust powder conveying systems make them indispensable in numerous industrial applications. In the chemical industry, these systems are used to transport raw materials and finished products, ensuring a seamless flow from processing to packaging. In the food industry, they are employed to handle powders like flour and sugar, maintaining hygiene standards and preventing contamination. The pharmaceutical sector also relies on such systems for the safe and efficient transport of active ingredients and other powders. The benefits extend beyond material handling; these systems contribute to improved workplace safety by reducing dust-related health risks and environmental pollution. Furthermore, the energy efficiency of modern conveying systems, particularly those with optimized air flow and reduced pressure losses, helps lower operational costs and align with sustainability goals.
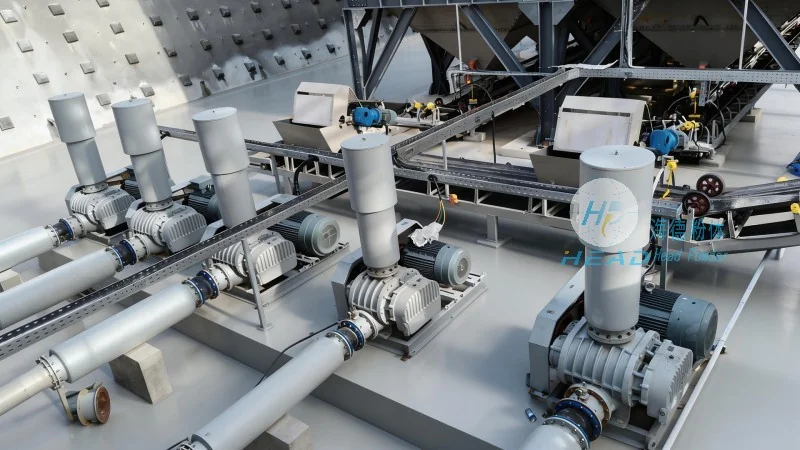
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted manufacturer of dust powder conveying systems. With a focus on innovation and quality, the company provides tailored solutions that meet the specific needs of various industries. The working principles and features discussed highlight the advanced technology and reliability that define HeadPowder's products. By investing in these systems, industries can achieve enhanced efficiency, safety, and sustainability in their material handling processes. As a leading provider, HeadPowder continues to advance the capabilities of dust and powder conveying technology, supporting the growth and success of its clients in a competitive global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top