Quartz stone powder, a common material in industrial applications, often requires efficient and reliable transport methods. Pneumatic conveying is a widely used technique for handling such powders, offering advantages over traditional methods like belt conveyors or bucket elevators. This article explores the working principle and key characteristics of quartz stone powder pneumatic conveying systems, highlighting how they enhance operational efficiency and material handling capabilities.
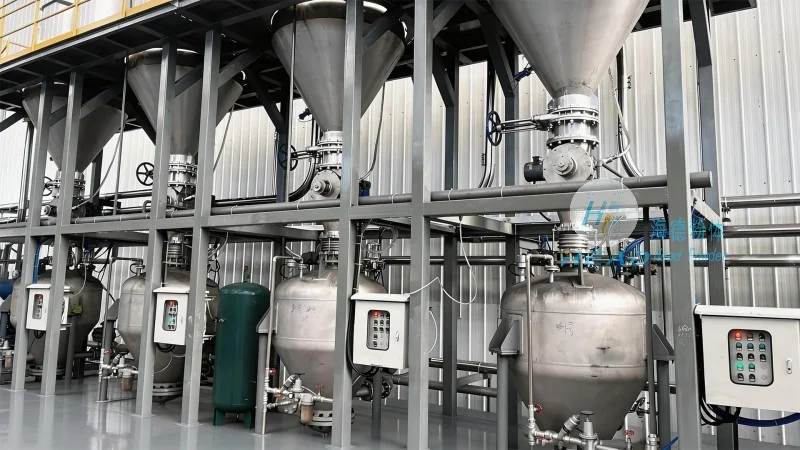
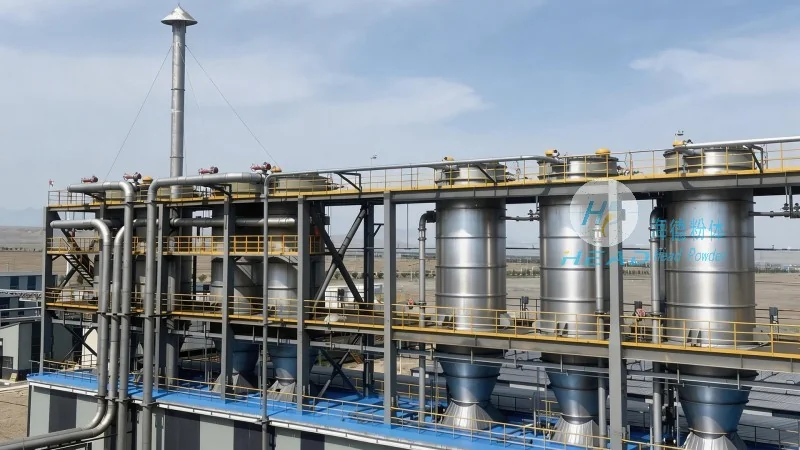
The core of a quartz stone powder pneumatic conveying system lies in the use of air as the conveying medium. The process typically involves several key components: a material hopper, a rotary valve or feeder, a conveying line, and a receiver or silo. The material is first fed into the system through the hopper and feeder, where it is then introduced into the conveying line under pressure. Air is then introduced, creating a flow that carries the powder particles through the pipeline. The system can operate in either positive pressure (where air is blown into the line) or negative pressure (where air is drawn out), depending on the specific application and material characteristics. The air velocity within the line is critical, as it must be sufficient to lift and transport the powder without causing excessive wear or degradation of the material. The system's design ensures that the powder is transported smoothly and efficiently, minimizing the risk of blockages or material loss.
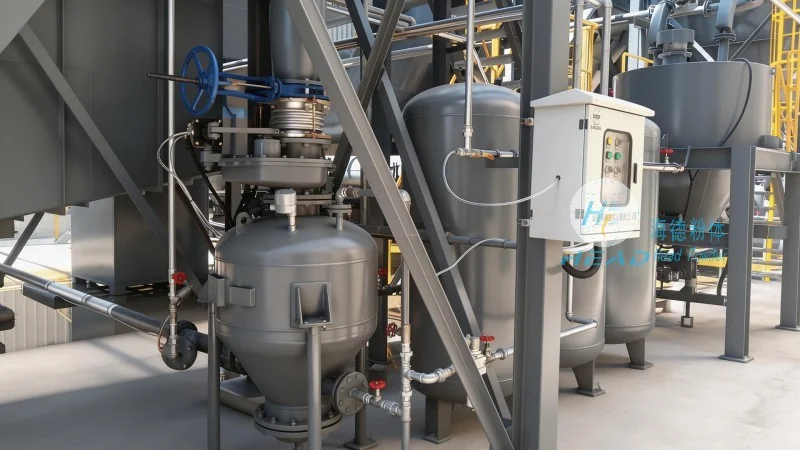
Several distinct characteristics define the performance of quartz stone powder pneumatic conveying systems, making them suitable for a wide range of industrial applications. First, the system offers high flexibility in terms of layout and installation. Unlike traditional mechanical conveyors, pneumatic systems can be easily reconfigured to accommodate changes in production processes or facility layouts. This adaptability is particularly valuable in industries where production lines are frequently modified or expanded. Second, pneumatic conveying systems provide excellent material handling capabilities, especially for fine powders like quartz stone. The air flow helps to prevent agglomeration and clumping, ensuring that the powder remains in a free-flowing state throughout the transport process. This is crucial for maintaining the quality and consistency of the material, which is essential for downstream processing steps. Third, the system is highly effective in preventing contamination and cross-contamination. The enclosed pipeline design and controlled air flow minimize the risk of dust exposure and contamination from external sources, making it suitable for applications where material purity is critical, such as in pharmaceutical or food processing industries. Fourth, pneumatic conveying systems are generally more energy-efficient compared to mechanical alternatives, particularly for long-distance or high-volume transport. The use of air as the conveying medium reduces the need for heavy machinery and moving parts, resulting in lower operational costs and reduced maintenance requirements.
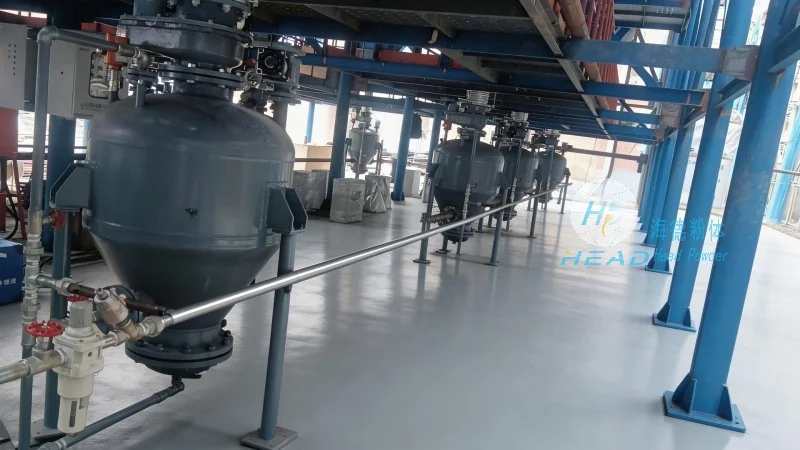
Quartz stone powder pneumatic conveying systems are widely used in various industrial sectors, including mining, construction, and manufacturing. In the mining industry, these systems are used to transport crushed quartz stone from processing plants to storage facilities or for further processing. The high efficiency and reliability of the system ensure that material is moved quickly and without interruption, supporting continuous production operations. In the construction industry, quartz stone powder is often used as a raw material for concrete and other building materials. Pneumatic conveying allows for the efficient transport of the powder from storage silos to mixing plants, reducing downtime and improving production throughput. In manufacturing, the system is used in the production of ceramics, glass, and other materials that require high-purity quartz stone. The ability to maintain material purity and prevent contamination is critical in these applications, and pneumatic conveying systems excel in meeting these requirements. Overall, the benefits of quartz stone powder pneumatic conveying systems include improved operational efficiency, reduced labor costs, and enhanced product quality, making them a preferred choice for many industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top