The pneumatic conveying system for cement and fly ash operates by utilizing air as the primary medium to transport bulk materials through a closed pipeline system. The process begins with the material being stored in a hopper, from which it is fed into the pipeline via a feeder. The feeder ensures a consistent flow rate of the material into the system. Simultaneously, a blower or air compressor generates high-velocity air that is introduced into the pipeline at the inlet. This air flow creates a pressure differential that lifts and propels the particles through the pipeline. The conveying mode, whether dilute phase (where particles are suspended in the air) or dense phase (where particles are in a slurry-like state), is determined by the material's characteristics and the required conveying distance. Dilute phase conveying is typically used for short to medium distances and for materials with low to moderate moisture content, as it offers high transport efficiency and low energy consumption. Dense phase conveying, on the other hand, is suitable for longer distances and for materials with higher moisture content or larger particle sizes, as it provides better control over the material flow and reduces the risk of particle degradation. The pipeline network includes various components such as bends, elbows, and valves, which are designed to minimize pressure loss and maintain stable flow. At the receiving end, the material is separated from the air using a cyclone separator or other dedusting equipment. The separated material is then collected in a receiving hopper, ready for further processing or use.
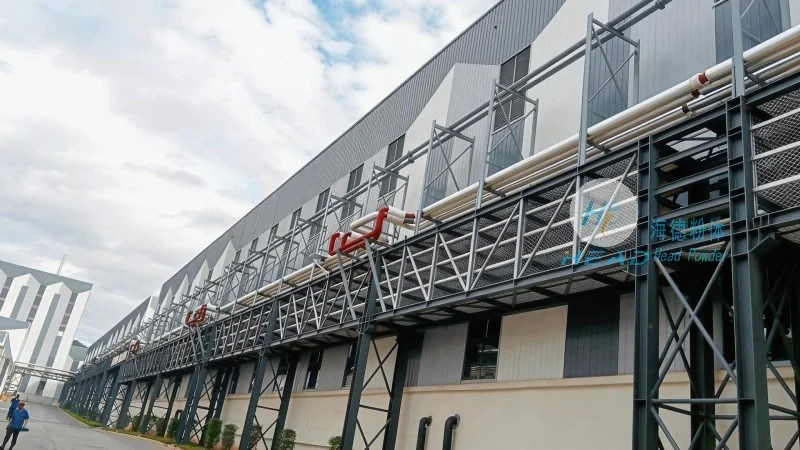
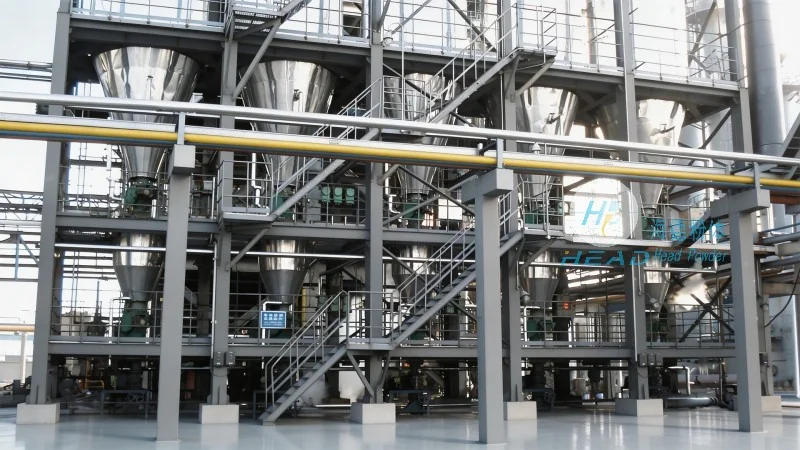
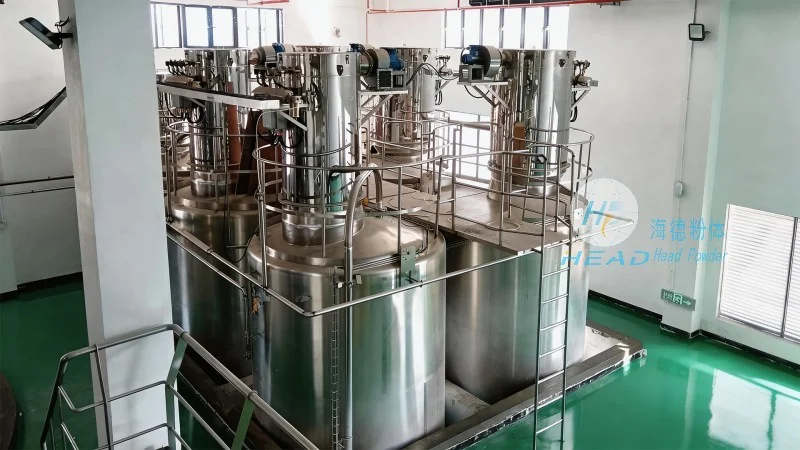
The cement and fly ash pneumatic conveying system possesses several distinct characteristics that contribute to its effectiveness in industrial applications. One of the primary advantages is its high degree of automation, which reduces the need for manual labor and enhances operational efficiency. The system can be integrated seamlessly with other production processes, such as cement grinding or fly ash processing, to form a continuous material flow. Another notable feature is its excellent dust control capabilities. By enclosing the material within the pipeline, the system minimizes dust emissions, improving workplace safety and reducing environmental impact. The system is also flexible in terms of layout, allowing it to be adapted to various plant configurations, including vertical or horizontal conveying. It can handle a wide range of particle sizes and moisture contents, making it suitable for different types of cement and fly ash. Additionally, the system is relatively compact compared to traditional belt conveyors, saving valuable space in the plant. The use of air as the conveying medium enables the transport of materials over long distances without the need for multiple transfer points, which can be costly and inefficient with other methods. Finally, the system is easy to maintain and has low operational costs, as it requires minimal moving parts and energy consumption, leading to long-term cost savings.
In the cement industry, the pneumatic conveying system is widely utilized for transporting raw materials such as limestone, clay, and iron ore from storage silos to the grinding mills. This efficient transport method ensures a consistent supply of raw materials, which is crucial for maintaining production rates. For fly ash, the system is employed to transport the ash from power plants to cement plants, where it is used as a supplementary cementitious material. This not only reduces the environmental impact of fly ash disposal but also enhances the performance of the cement product. The benefits of using this system in these applications include improved productivity, reduced labor costs, and enhanced product quality. The enclosed transport also prevents contamination of the material with external elements, ensuring consistent quality. Furthermore, the system contributes to a cleaner and safer working environment by minimizing dust emissions and reducing the risk of material spillage. The flexibility of the system allows it to be customized to meet the specific needs of different plants, ensuring optimal performance and efficiency. Overall, the pneumatic conveying system for cement and fly ash is a reliable and efficient solution for material transport in industrial settings, offering significant advantages over traditional methods.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top