For industries dealing with rare earth powders, the efficiency and safety of material handling systems are paramount. Pneumatic conveying systems offer a solution for transporting these fine materials, but they present unique challenges, particularly concerning dust leakage. This article explores effective strategies and best practices to prevent dust leakage in pneumatic conveying systems when handling rare earth powders, ensuring operational safety and compliance with environmental standards.
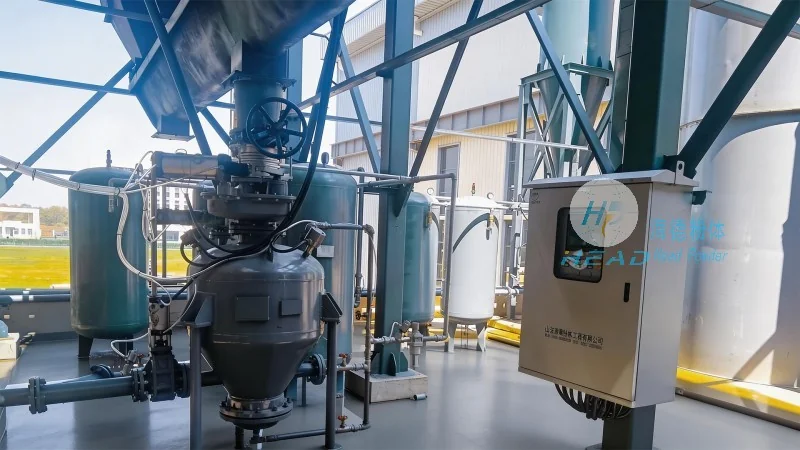
Rare earth powders are known for their fine particle size and high reactivity, which can exacerbate dust formation and leakage during transportation. Unlike bulkier materials, these powders can easily escape through system joints, seals, and even the conveying lines if not properly managed. The health risks associated with rare earth dust inhalation, combined with environmental regulations, make it essential to implement robust dust control measures. A well-designed pneumatic conveying system must address these challenges to maintain a safe working environment and avoid costly downtime or regulatory penalties.
Several critical components and design features contribute to minimizing dust leakage in pneumatic conveying systems for rare earth powders. First, the selection of appropriate equipment is crucial. High-quality, dust-tight valves, such as rotary airlocks and slide gates, are essential to prevent material escape at transfer points. These components are engineered to maintain a consistent pressure seal, ensuring that the material remains contained within the system. Additionally, the use of flexible, yet durable, hoses and tubing with reinforced seals is vital. These hoses must be capable of withstanding the abrasive nature of rare earth powders while maintaining a tight seal to prevent air or material leakage.
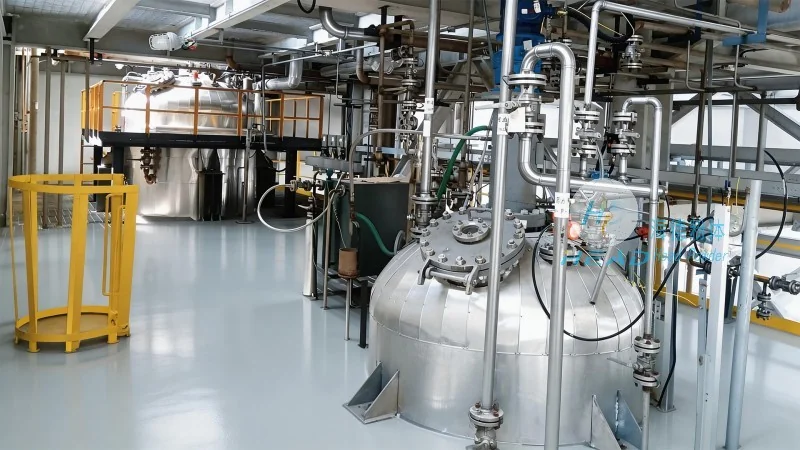
Another critical aspect is the system's overall pressure management. Maintaining a consistent positive pressure throughout the conveying line helps to keep the material contained and prevents external air from entering the system, which could carry dust particles out. This is often achieved through the use of pressure regulators and filters that ensure the system operates within optimal pressure ranges. Regular maintenance of these components is also essential to prevent wear and tear that could compromise the system's integrity over time.
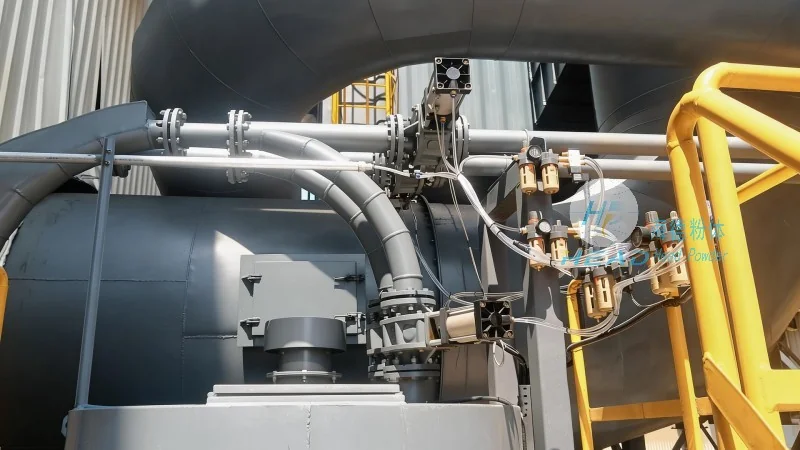
Advanced sealing technologies play a pivotal role in preventing dust leakage. For instance, the implementation of double-seal or multi-seal systems in critical areas, such as the connection points between the hopper and the conveying line, provides an additional layer of protection. These seals work by creating a barrier that prevents material from escaping even under pressure fluctuations. Enclosure systems, such as dust collection hoods and containment enclosures, are also effective in capturing any stray dust particles that may escape. These enclosures are designed to capture and filter the air, ensuring that no dust is released into the surrounding environment. The use of high-efficiency particulate air (HEPA) filters in these systems further enhances the filtration efficiency, ensuring that the air released is clean and safe.
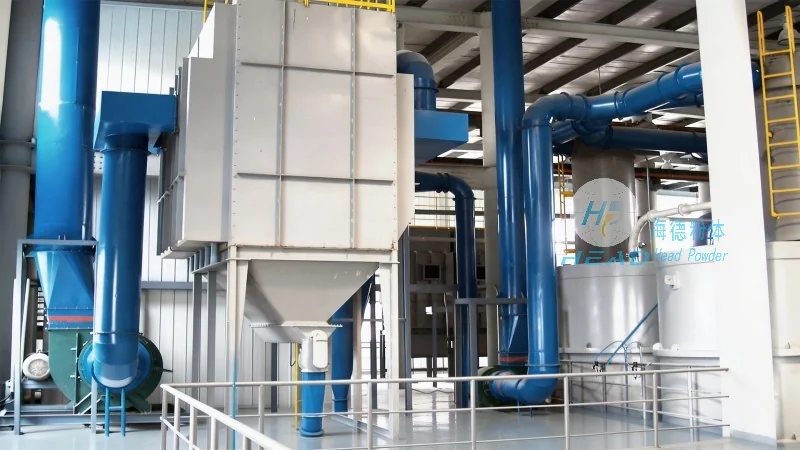
Preventing dust leakage is not a one-time setup but an ongoing process that requires regular maintenance and monitoring. Routine inspections of all system components, including seals, valves, and hoses, are necessary to identify and address any potential issues before they escalate. This includes checking for signs of wear, such as cracks or fraying in hoses, and replacing them as needed. Additionally, monitoring the system's pressure and flow rates can help detect any anomalies that may indicate a leak. Implementing a preventive maintenance schedule, as recommended by manufacturers like Shandong HeadPowder Engineering Co., Ltd., ensures that the system remains in optimal condition, reducing the risk of dust leakage and extending its operational lifespan.
Preventing dust leakage in pneumatic conveying systems for rare earth powders is a multifaceted challenge that requires a combination of proper equipment selection, advanced sealing technologies, and diligent maintenance. By addressing these aspects, industries can ensure the safe and efficient handling of rare earth powders, protecting both their workforce and the environment. Companies like Shandong HeadPowder Engineering Co., Ltd., with their expertise in engineering and manufacturing pneumatic conveying systems, offer tailored solutions that meet the specific needs of rare earth powder handling, helping businesses maintain compliance and operational excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top