HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems for various industrial applications. This article delves into the working principle and key characteristics of pneumatic conveying systems specifically tailored for the transportation of pulverized coke and stone powder, highlighting the technical aspects and operational advantages that make such systems efficient and reliable.
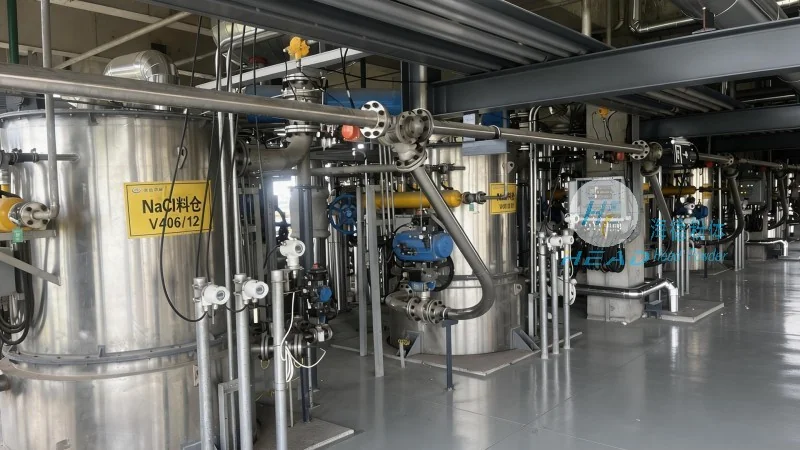
The core of pneumatic conveying systems lies in the use of air or gas as the conveying medium to transport bulk materials like pulverized coke and stone powder. The process typically involves several key components and steps. First, the material is fed into a hopper or feeder, where it is then introduced into a pipeline. Simultaneously, a fan or blower generates a flow of air within the pipeline, creating a pressure differential that propels the material forward. The material is suspended in the air stream, allowing it to be transported over long distances without the need for mechanical components like belts or buckets. The system can operate under either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out, creating a vacuum). For applications involving pulverized coke and stone powder, positive pressure systems are commonly preferred due to their ability to handle abrasive materials and prevent dust emissions effectively. The air velocity within the pipeline is carefully controlled to ensure that the material particles remain suspended and do not settle or cause blockages. This controlled air flow, combined with the material's properties such as particle size, density, and moisture content, determines the optimal conveying velocity and pressure requirements. The system's design, including the size of the pipeline, the type of air mover, and the feeding mechanism, is tailored to match the specific characteristics of the material being transported, ensuring efficient and consistent performance.
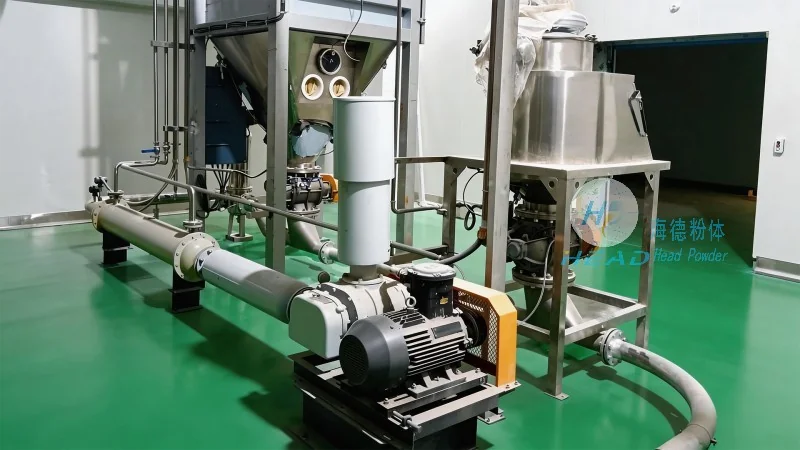
Several distinct characteristics define the performance and advantages of pneumatic conveying systems used for pulverized coke and stone powder. First, the system offers a high degree of flexibility in terms of layout and installation. Unlike traditional mechanical conveying systems, pneumatic conveyors can be easily reconfigured or expanded to accommodate changes in production needs or facility expansions. This adaptability is particularly valuable in industrial settings where processes may evolve over time. Second, pneumatic conveying provides excellent material handling capabilities, especially for fine or abrasive powders. The air stream effectively suspends the particles, preventing them from coming into direct contact with the pipeline walls, which reduces wear and tear and extends the system's lifespan. This is crucial for materials like pulverized coke and stone powder, which can be highly abrasive and corrosive. Third, the system is highly efficient in terms of energy consumption and operational costs. By using air as the conveying medium, the system minimizes the need for moving parts, reducing maintenance requirements and operational downtime. The energy required to transport the material is directly proportional to the air flow rate and pressure, allowing for precise control and optimization. Fourth, pneumatic conveying systems are effective in controlling dust emissions. The enclosed pipeline design and the use of air to transport the material prevent dust from being released into the environment, which is essential for maintaining workplace safety and compliance with environmental regulations. This is particularly important for materials like pulverized coke and stone powder, which can generate significant dust during handling. Fifth, the system offers consistent and reliable material flow. The controlled air flow and the design of the feeding mechanism ensure that the material is conveyed at a steady rate, minimizing variations in flow rate and preventing overloading or underloading of downstream equipment. This consistency is critical for processes that require precise material delivery, such as in chemical or pharmaceutical applications.
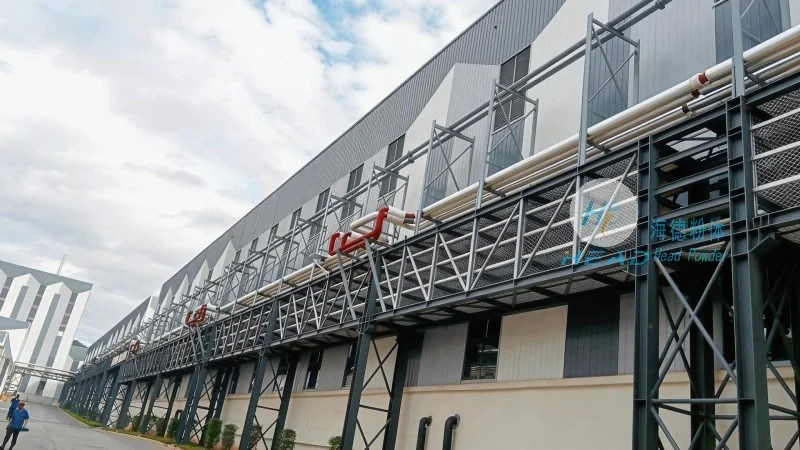
When designing a pneumatic conveying system for pulverized coke and stone powder, several technical considerations must be taken into account to ensure optimal performance and longevity. The first consideration is the material's physical properties, including particle size distribution, density, and moisture content. These properties directly impact the air velocity and pressure required for effective conveying. For example, finer particles may require higher air velocities to remain suspended, while larger or denser particles may need higher pressure to overcome resistance. The system's design must account for these variations to avoid blockages or inefficient transport. Second, the system's layout and the distance to be covered are critical factors. The length and diameter of the pipeline, as well as the number of bends and fittings, affect the pressure drop and energy consumption. Longer distances or more complex layouts may require additional air movers or larger pipeline diameters to maintain the required air velocity. Third, the choice of air mover is essential. Fans or blowers with sufficient capacity and pressure rating are needed to generate the required air flow. The type of air mover (e.g., centrifugal, positive displacement) is selected based on the system's operating conditions and the material's characteristics. Fourth, the feeding mechanism is a key component. Proper feeding ensures that the material is introduced into the pipeline at a consistent rate and without causing blockages. Feeding devices such as rotary valves, screw feeders, or pressure feeders are used to control the material flow and maintain system stability. Fifth, the system's control and monitoring features are important for maintaining optimal performance. Sensors and control systems can monitor air pressure, flow rate, and material level, allowing for real-time adjustments and preventing system failures. This proactive monitoring helps to minimize downtime and ensure consistent operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top