Refractory material pneumatic conveying systems are essential industrial equipment used for the efficient transport of bulk materials, particularly in industries such as ceramics, steel, and construction. These systems utilize air or other gases to move refractory powders and granules from one location to another, offering advantages like reduced labor costs, improved safety, and enhanced process control. The core of these systems lies in their design, which must account for material properties, flow rates, and operational efficiency to ensure reliable performance.
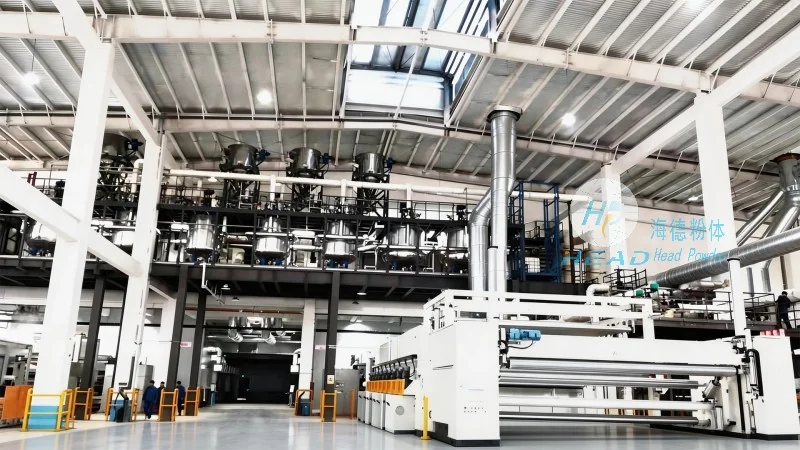
The design of a refractory material pneumatic conveying system involves several critical principles that ensure optimal operation. First, the system must be tailored to the specific characteristics of the refractory material, including its particle size, density, and moisture content. For example, materials with high moisture or abrasive properties may require specialized components like high-quality seals and wear-resistant pipelines to prevent degradation and maintain efficiency. Second, the system's capacity and flow rate must be matched to the production requirements. This involves calculating the required air velocity and pressure to achieve the desired material transport speed without causing excessive pressure drops or material degradation. Third, the system design considers the overall layout and space constraints of the facility, ensuring that the conveying lines are integrated seamlessly with existing processes. Additionally, safety and maintenance considerations are integral, with features like pressure relief valves and regular inspection points to ensure safe and reliable operation.
A typical refractory material pneumatic conveying system consists of several key components, each playing a vital role in the material transport process. The main components include a material hopper or feeder, an air compressor or blower, a conveying line (often with bends and elbows), and a receiver or discharge hopper. The process begins with the material being fed from the hopper into the conveying line. The air compressor then generates the necessary pressure to move the material through the line. As the air and material mixture travels, the material is carried by the air stream, and the system's design ensures that the material remains suspended and moves efficiently. The conveying line may include features like pulse jets or rotary valves to control the flow and prevent blockages. The receiver at the end of the line collects the conveyed material, and the system may include filters or cyclones to separate any residual material from the air before it is discharged to the environment.
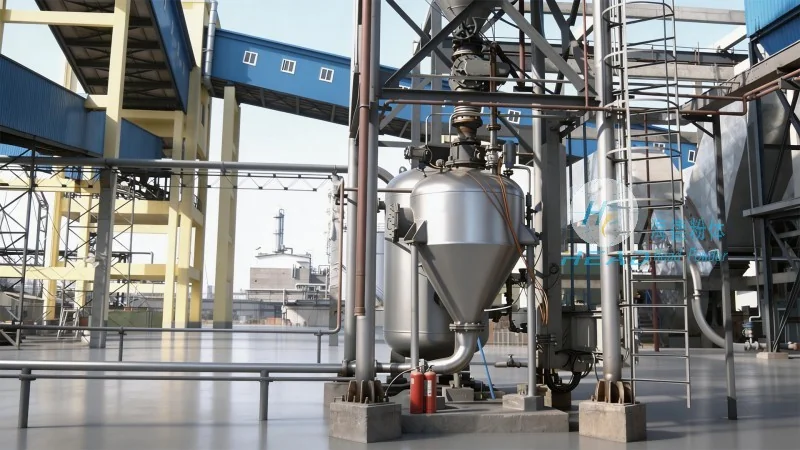
Implementing a refractory material pneumatic conveying system offers numerous benefits for industrial operations. One of the primary advantages is the reduction in labor costs, as automated systems eliminate the need for manual handling of bulk materials. This not only saves on labor expenses but also minimizes the risk of workplace injuries associated with manual material transport. Additionally, these systems enhance process safety by reducing exposure to dust and other airborne particles, which can be hazardous to workers. The automated nature of the system also improves process control, allowing for precise control over material flow rates and delivery times, which is crucial for maintaining consistent product quality. Furthermore, the compact design of many pneumatic conveying systems allows for efficient use of space, making them suitable for facilities with limited floor space. Finally, the systems are generally low-maintenance, with components designed for durability and long service life, reducing downtime and maintenance costs over time.
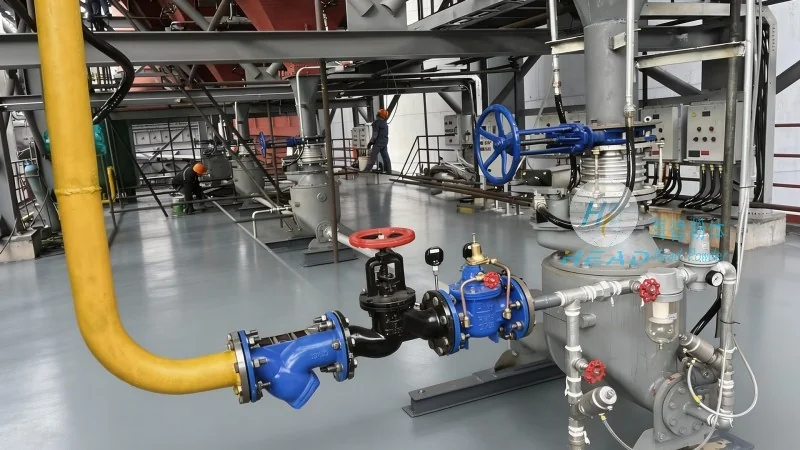
Refractory material pneumatic conveying systems are widely used in various industrial applications where the transport of bulk materials is critical. In the ceramics industry, these systems are used to transport raw materials like clay and feldspar from storage to processing lines. In the steel industry, they are employed to move refractory materials used in furnace linings and other components. The construction industry also utilizes these systems for transporting refractory aggregates and powders used in building materials. Additionally, in the chemical industry, they may be used to convey specialized refractory materials for industrial processes. The versatility of these systems makes them suitable for a wide range of applications, from small-scale operations to large-scale industrial facilities.
HeadPowder, a prominent company in the field of refractory material handling, specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder provides comprehensive solutions that meet the specific requirements of each client. The company's headquarters is located in Shandong, China, where it leverages advanced technology and expertise to develop cutting-edge equipment. HeadPowder's team of engineers and technicians work closely with clients to understand their operational needs and design systems that optimize material transport efficiency while ensuring safety and reliability. The company's commitment to quality is evident in its use of premium materials and rigorous testing processes, ensuring that each system meets the highest industry standards. Whether for new installations or system upgrades, HeadPowder offers reliable solutions that enhance operational efficiency and reduce costs for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top