What is a Pharmaceutical Pneumatic Conveying System? What are its Design Principles?
Release time:2026-09-14 10:53:57
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
Pharmaceutical pneumatic conveying systems are critical equipment in the pharmaceutical manufacturing industry, designed to transport powders and bulk materials safely and efficiently. These systems utilize air or other gases to move materials from one location to another, ensuring compliance with stringent regulatory standards. The design principles behind these systems are intricate, balancing performance, safety, and regulatory adherence.
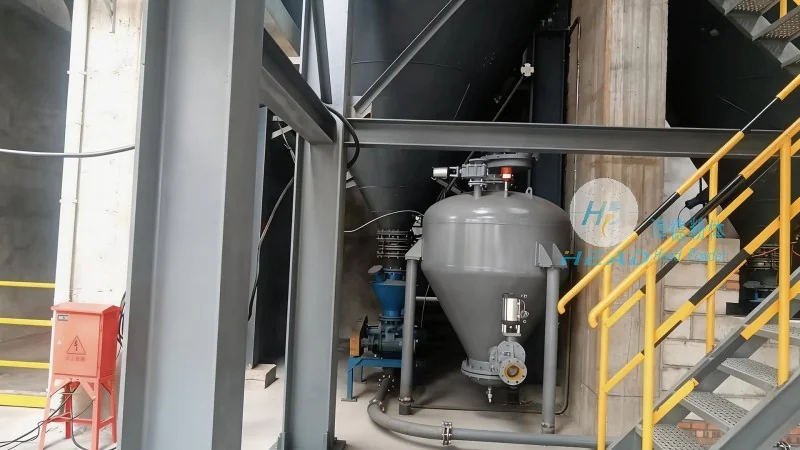
Understanding Pharmaceutical Pneumatic Conveying Systems
A pharmaceutical pneumatic conveying system is a closed-loop system that uses compressed air or other gases to transport powders, granules, or other bulk materials. Unlike traditional mechanical conveyors, which rely on physical contact and friction, pneumatic systems operate by creating a pressure differential to move materials through a pipeline. This method is particularly advantageous in pharmaceutical applications where contamination control, product integrity, and hygiene are paramount.
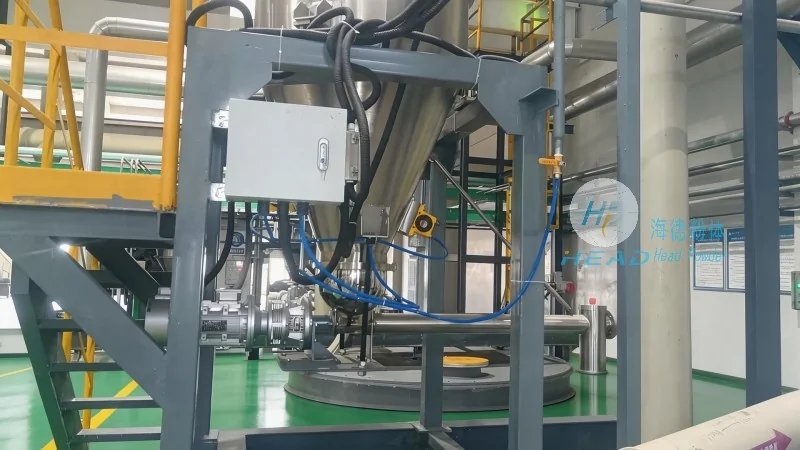
Key Design Principles for Pharmaceutical Pneumatic Conveying
The design of a pharmaceutical pneumatic conveying system is governed by several critical principles to ensure optimal performance and compliance with industry regulations. These principles include:
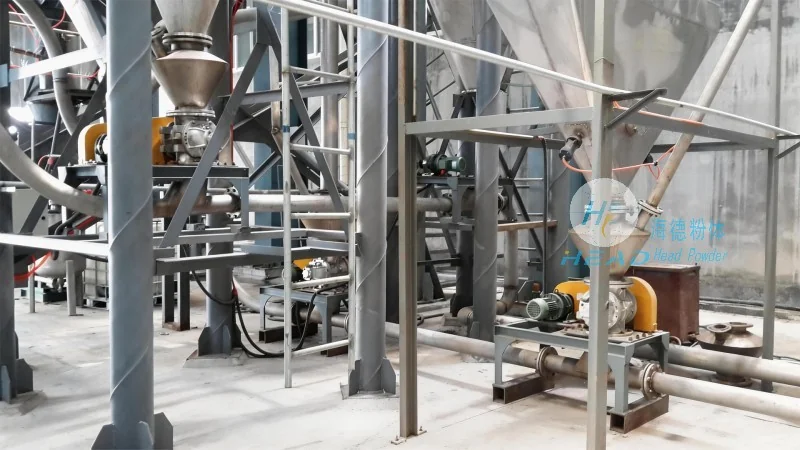
- Material Compatibility: The system components, such as pipes, valves, and filters, must be made from materials that are compatible with pharmaceutical powders. Common materials include stainless steel, PTFE, and food-grade plastics to prevent contamination and ensure product purity.
- Hygienic Design: All parts of the system are designed to be easy to clean and maintain, with smooth surfaces and minimal dead zones where particles can accumulate. This is crucial for preventing cross-contamination and ensuring that the system meets cGMP (current Good Manufacturing Practices) standards.
- Pressure and Flow Control: Precise control of air pressure and flow rate is essential to maintain consistent material transport. This ensures that the material is conveyed at the right speed and without causing degradation or segregation of the powder. Advanced control systems are often integrated to monitor and adjust these parameters in real-time.
- Filter and Dust Collection: To prevent product loss and maintain air quality, the system includes high-efficiency filters and dust collection systems. These components capture any particles that escape the conveying line, ensuring that the air discharged is clean and that the product remains pure throughout the process.
- Safety and Explosion Prevention: Pharmaceutical facilities often handle materials that could be combustible or explosive. Therefore, the design incorporates safety features such as explosion-proof valves, pressure relief devices, and flame arrestors to prevent accidents and protect personnel and equipment.
Components of a Pharmaceutical Pneumatic Conveying System
A typical pharmaceutical pneumatic conveying system consists of several key components, each playing a vital role in the overall operation. These components include:
- Feeder: The feeder is responsible for feeding the material into the conveying line at a controlled rate. It ensures that the material is introduced smoothly and without causing blockages or uneven flow.
- Pipeline: The pipeline is the main conduit through which the material and air travel. It is typically made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of pharmaceutical powders and maintain hygiene.
- Compressor and Air Treatment: The compressor provides the necessary pressure to move the material through the pipeline. The air treatment system, including filters and dryers, ensures that the air used is clean and free of contaminants that could affect the product.
- Control Valves: These valves regulate the flow of air and material, allowing for precise control over the conveying process. They can be automated to adjust to changes in material feed or system pressure.
- Receiver: The receiver is the final destination where the material is deposited. It is designed to be easy to clean and maintain, with features such as a discharge valve and a dust collection system to prevent product loss.
- Filter and Dust Collector: As mentioned earlier, this component is essential for capturing any particles that escape the conveying line and ensuring that the air discharged is clean. It may include a bag filter or a cartridge filter, depending on the system design.
Advantages of Pharmaceutical Pneumatic Conveying Systems
Pharmaceutical pneumatic conveying systems offer several advantages over traditional mechanical conveyors, making them the preferred choice in many pharmaceutical applications:
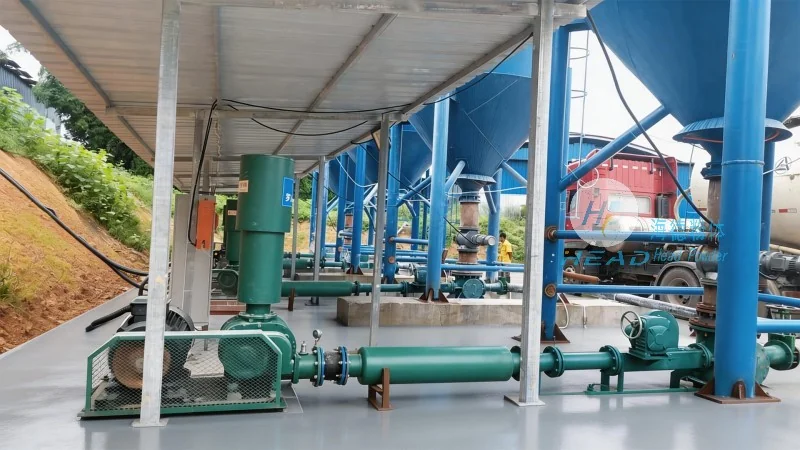
- Non-Contact Transport: Since the material is conveyed without physical contact, there is no risk of cross-contamination or product degradation from friction or abrasion.
- Flexibility and Scalability: These systems can be easily reconfigured or expanded to accommodate changes in production volume or product types, making them suitable for both small-scale and large-scale manufacturing.
- Space Efficiency: Pneumatic systems can be installed in tight spaces, as they do not require large, bulky equipment or extensive floor space.
- Reduced Labor and Maintenance: Automated control systems and easy-to-clean components reduce the need for manual labor and frequent maintenance, lowering operational costs.
- Compliance with Regulations: The design principles and components of these systems are specifically tailored to meet the stringent regulatory requirements of the pharmaceutical industry, ensuring that products are manufactured in a safe and compliant manner.
Conclusion
Pharmaceutical pneumatic conveying systems are sophisticated pieces of equipment that play a crucial role in the pharmaceutical manufacturing process. Their design principles, which prioritize material compatibility, hygiene, and safety, ensure that they can effectively transport powders and bulk materials while maintaining product integrity and regulatory compliance. As the pharmaceutical industry continues to evolve, these systems will remain essential for meeting the demands of modern manufacturing, providing reliable and efficient solutions for transporting sensitive materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
