For those in the food processing industry, understanding the role and design of pneumatic conveying systems for food additives is crucial. These systems are essential for efficiently transporting various food additives, such as flavorings, colorings, and preservatives, from storage to processing equipment. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and supplying high-quality pneumatic conveying systems tailored to the unique needs of the food industry.
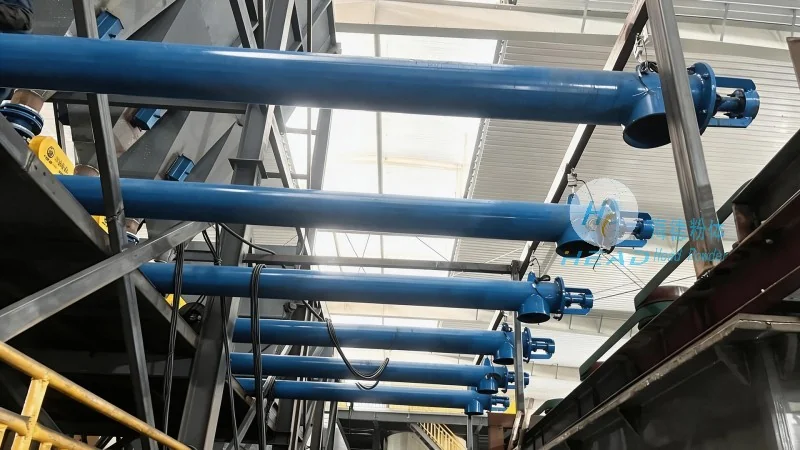
A pneumatic conveying system uses air or gas to transport bulk materials like food additives through a pipeline. Unlike mechanical conveyors, which rely on physical contact and movement, pneumatic systems offer a non-contact method that minimizes product contamination and damage. This makes them ideal for handling sensitive food additives that require strict hygiene and quality control. The system typically consists of a hopper for material storage, a blower or compressor to generate airflow, a pipeline network, and a receiver or processing unit to collect the conveyed material.
Several critical components work together to ensure the smooth operation of a food additive pneumatic conveying system. The hopper, often made of stainless steel, serves as the storage vessel for the food additive. It is designed to maintain the material's quality and prevent moisture or contamination. The blower or compressor provides the necessary air pressure to move the material through the pipeline. The pipeline network, usually constructed from food-grade materials like stainless steel or PTFE, ensures the material is transported efficiently and hygienically. The receiver or processing unit collects the conveyed additive and may include features like filtration or separation to maintain product purity.
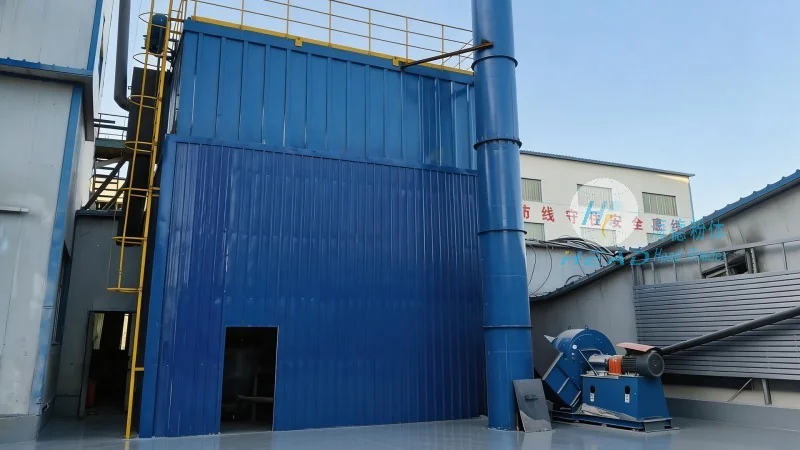
The design of a food additive pneumatic conveying system must adhere to several key principles to ensure efficiency, safety, and compliance. One of the primary principles is maintaining a consistent airflow rate. This ensures that the material is conveyed at a uniform speed, preventing blockages or uneven distribution. The system must also be designed to handle the specific properties of the food additive, such as its particle size, density, and moisture content. For example, fine powders like colorings or flavorings may require higher air velocities to prevent settling or clogging in the pipeline. Additionally, the system must incorporate proper filtration and cleaning mechanisms to prevent material buildup and maintain hygiene standards.
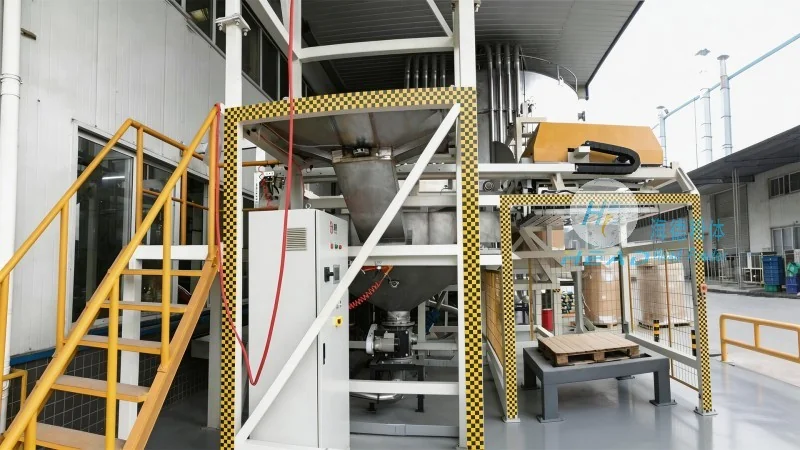
Food additive pneumatic conveying systems must comply with various industry regulations and standards to ensure food safety and quality. These standards often include requirements for material contact surfaces, such as using stainless steel or other food-grade materials to prevent contamination. The system must also be designed to minimize the risk of cross-contamination between different food additives. This may involve using separate pipelines or cleaning procedures for each additive. Furthermore, the system should include monitoring and control features to track the flow rate, pressure, and temperature, ensuring that the process remains within safe and efficient parameters.
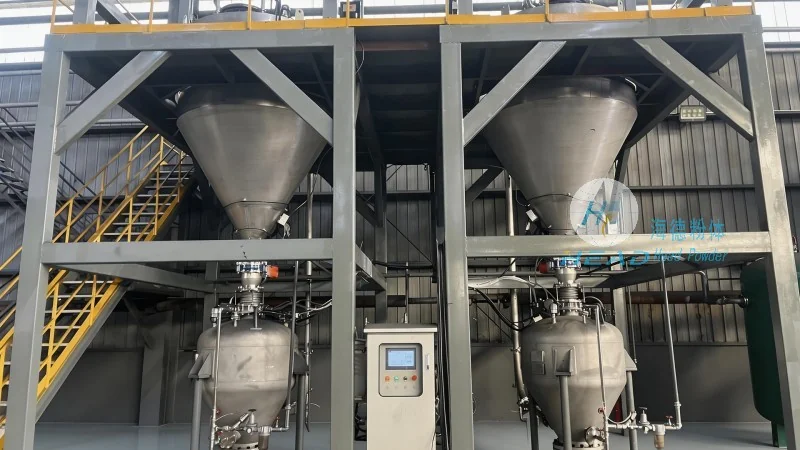
Implementing a pneumatic conveying system for food additives offers several benefits for food processing facilities. One of the main advantages is improved efficiency and productivity. By automating the material transport process, the system reduces labor costs and minimizes downtime caused by manual handling. Additionally, pneumatic systems offer better hygiene and cleanliness compared to mechanical conveyors, as they do not require physical contact with the product. This helps maintain the quality and safety of the food additive, which is critical for consumer trust and regulatory compliance. Another benefit is the flexibility of the system, which can be easily adjusted to handle different types of food additives or varying production volumes.
In conclusion, food additive pneumatic conveying systems are essential equipment for modern food processing facilities. Their design, based on principles of efficient airflow, material handling, and hygiene, ensures that food additives are transported safely and effectively. By adhering to industry standards and incorporating advanced components, these systems provide significant benefits in terms of efficiency, safety, and product quality. For companies in the food industry, investing in a well-designed pneumatic conveying system is a strategic decision that supports long-term success and compliance with regulatory requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top