Quartz powder, a widely used industrial material, often requires efficient and reliable transportation methods for processing and distribution. Pneumatic conveying is a key technology in this regard, offering a solution that minimizes dust, enhances safety, and improves operational efficiency. This article provides an overview of the working principles of quartz powder pneumatic conveying, along with its classification and practical applications.
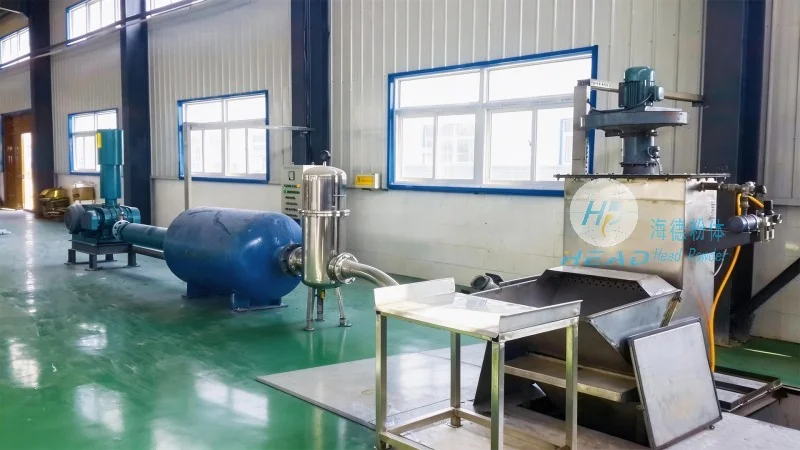
HeadPowder, a leading company in the field, specializes in engineering solutions for material handling. Based in Shandong, China, the company leverages advanced technology to address the unique challenges of transporting quartz powder. The fundamental principle of pneumatic conveying involves using air or gas to move solid particles through a pipeline system. This method is particularly suitable for quartz powder due to its fine particle size and the need to prevent contamination and loss during transport.
The core mechanism of pneumatic conveying for quartz powder relies on the creation of a pressure differential between the conveying line and the ambient environment. In a typical system, a blower or compressor generates the necessary airflow, which is then directed into the pipeline. The quartz powder is introduced into the system, either by gravity feed or through a feeder, and is entrained by the moving air stream. The air-particle mixture travels through the pipeline to the destination point, where the particles are separated from the air using a separator or cyclone. The separated air is then recirculated or vented, while the quartz powder is collected in a hopper or storage tank.
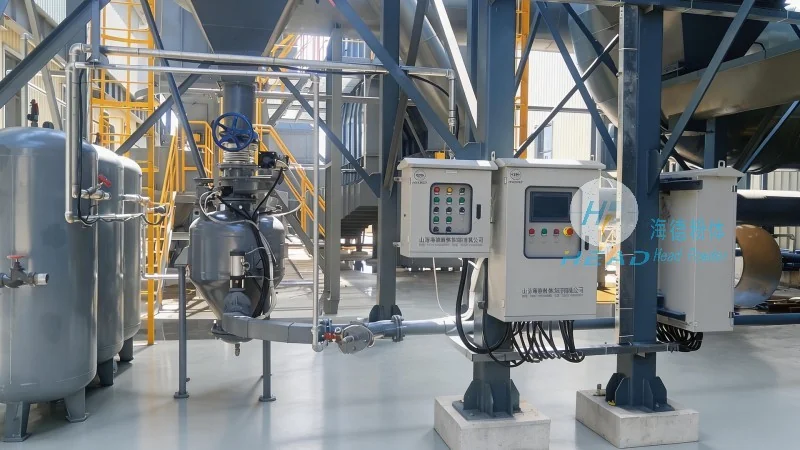
Pneumatic conveying systems for quartz powder are generally classified into two main categories: dilute-phase and dense-phase systems. Dilute-phase systems operate at higher velocities, typically 20-30 meters per second, and are suitable for short distances or low particle loads. These systems are efficient for transporting fine powders like quartz over moderate distances. Dense-phase systems, on the other hand, operate at lower velocities (5-15 meters per second) and higher particle concentrations, making them ideal for longer distances or when handling larger particle sizes. The choice between these systems depends on factors such as the distance to be covered, the particle size distribution, and the required material handling capacity.
Several critical components are essential for the effective operation of quartz powder pneumatic conveying systems. These include the air supply unit (blower or compressor), the feeder (which controls the powder flow rate), the pipeline system (usually made of stainless steel or other corrosion-resistant materials to prevent contamination), the separator (to separate powder from air), and the collection equipment (such as hoppers or silos). Each component plays a vital role in ensuring the system operates smoothly and efficiently. For instance, the feeder must be designed to handle the specific characteristics of quartz powder, such as its flowability and potential for bridging, to maintain consistent material flow. The separator must be efficient in capturing the fine particles, minimizing loss and ensuring product purity.
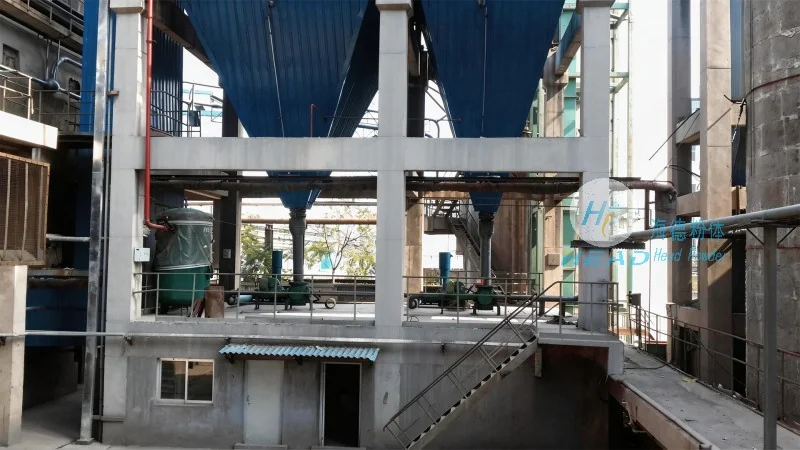
The application of pneumatic conveying in quartz powder handling spans various industries. In the manufacturing of glass and ceramics, quartz powder is a primary raw material, and efficient transport is crucial for maintaining production continuity. The system ensures that the powder is delivered to the production line without contamination, which is critical for product quality. In the construction industry, quartz powder is used in concrete and mortar formulations, and pneumatic conveying facilitates the precise mixing of ingredients, improving the consistency and durability of the final products. Additionally, in the pharmaceutical and food industries, where purity is paramount, pneumatic conveying systems are preferred as they prevent cross-contamination and maintain the integrity of the material.
Compared to traditional methods like bucket elevators or belt conveyors, pneumatic conveying offers several advantages for quartz powder transport. One of the most significant benefits is the elimination of dust and the reduction of environmental hazards. Since the material is contained within the pipeline, there is minimal exposure to the air, which is particularly important for fine powders that can cause respiratory issues. Additionally, pneumatic conveying systems are more flexible and can be easily reconfigured to adapt to changes in production needs. They also require less floor space compared to other bulk material handling systems, making them suitable for facilities with limited space. Furthermore, the system can handle a wide range of particle sizes and flow rates, providing versatility in material handling.
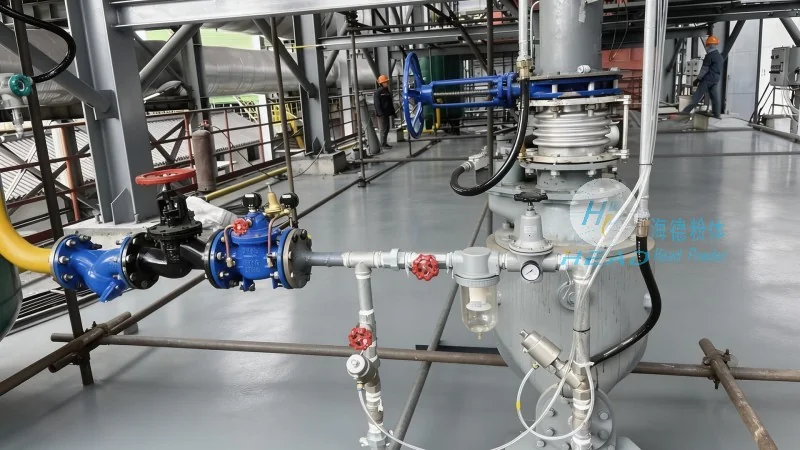
Despite its advantages, pneumatic conveying of quartz powder also presents certain challenges. One of the main issues is the potential for particle agglomeration or bridging in the feeder or pipeline, which can lead to blockages and system downtime. To mitigate this, proper design of the feeder and the use of anti-bridging devices are essential. Another challenge is the wear and tear on the pipeline and components due to the abrasive nature of quartz powder. Regular maintenance and the use of wear-resistant materials are necessary to extend the system's lifespan. Additionally, the energy consumption of the system, particularly in dense-phase operations, can be higher than other methods, which may impact operational costs. However, advancements in technology, such as more efficient blowers and optimized system designs, have helped to reduce these challenges and improve overall performance.
Pneumatic conveying is a highly effective and versatile method for transporting quartz powder, offering numerous benefits over traditional bulk handling techniques. By understanding the working principles and classification of these systems, as well as the key components and applications, industries can make informed decisions to enhance their material handling processes. HeadPowder, with its expertise and commitment to quality, continues to provide innovative solutions that meet the evolving needs of the quartz powder industry. The adoption of pneumatic conveying not only improves operational efficiency but also contributes to a safer and more sustainable industrial environment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top