Phosphate Powder Pneumatic Conveying: Working Principles and Application Classifications
Release time:2026-09-14 10:39:54
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
Phosphate fertilizer is a critical component in modern agriculture, and the efficient handling of phosphate powder through pneumatic conveying systems is essential for optimizing production processes. This article introduces the fundamental working principles and various application classifications of phosphate powder pneumatic conveying systems, with a focus on the solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
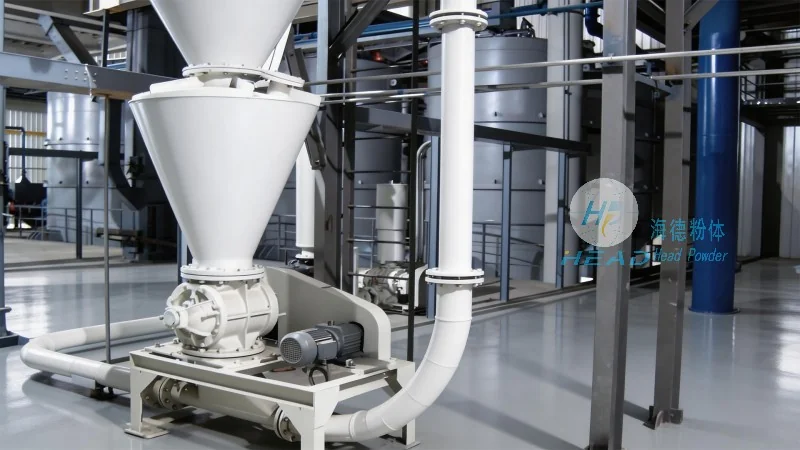
The Core Working Principle of Phosphate Powder Pneumatic Conveying
Pneumatic conveying systems utilize air as the medium to transport phosphate powder from one location to another. The core principle involves creating a pressure differential between the conveying line and the ambient environment. In positive pressure systems, compressed air is introduced at the discharge end of the pipeline, generating a pressure higher than the surrounding air. This pressure difference forces the phosphate powder to move along the pipeline. Conversely, negative pressure systems operate by creating a vacuum at the intake end, drawing the powder into the pipeline as air is drawn through. The choice between positive and negative pressure depends on factors such as material properties, distance, and system complexity.
Classification of Phosphate Powder Pneumatic Conveying Systems
Phosphate powder pneumatic conveying systems can be broadly classified into several types based on their operational principles and design. The primary classifications include:
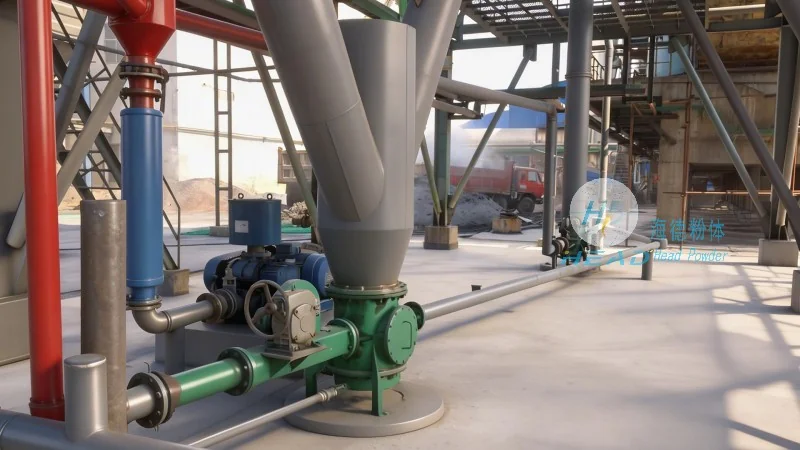
- Positive Pressure Conveying: This system uses compressed air to push the phosphate powder through the pipeline. It is suitable for short to medium distances and is effective for handling materials that are prone to caking or have high moisture content. The positive pressure system ensures that the material is continuously pushed forward, reducing the risk of blockages.
- Negative Pressure Conveying: In this system, a vacuum is created at the intake end, drawing the phosphate powder into the pipeline. Negative pressure systems are ideal for long-distance conveying and are commonly used when the material is to be transported to a central collection point. They are also less likely to cause dust emissions compared to positive pressure systems.
- Combined (Positive-Negative) Conveying: This hybrid system combines elements of both positive and negative pressure systems. It typically uses a positive pressure section for the initial transport and a negative pressure section for the final delivery, optimizing efficiency for complex conveying routes.
Application Scenarios in the Phosphate Industry
Phosphate powder pneumatic conveying systems are widely applied across various stages of the phosphate production and processing chain. Key application scenarios include:
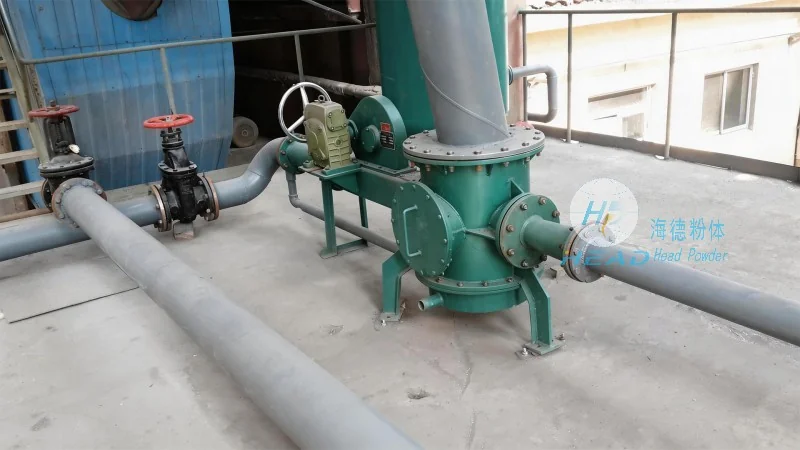
- Raw Material Handling: From the initial reception of phosphate ore to the crushing and grinding stages, pneumatic conveying systems efficiently transport raw materials to storage silos or processing units. This ensures a continuous flow of feedstock for subsequent chemical processing.
- Intermediate Storage and Transfer: After processing, phosphate powders are often stored in large silos. Pneumatic conveying systems facilitate the transfer of material between silos, ensuring that the right blend of nutrients is available for downstream packaging or blending operations.
- Packaging Line Integration: In the final stages of production, phosphate powders are conveyed to packaging lines where they are filled into bags or containers. The precision and reliability of pneumatic conveying systems are crucial for maintaining product quality and preventing contamination.
Technical Advantages of HeadPowder's Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of the phosphate industry. Our solutions are engineered to address the challenges of handling fine, abrasive, and moisture-sensitive phosphate powders. Key technical advantages include:
- Efficient Material Transfer: Our systems are designed to minimize material loss and ensure consistent flow rates, even for challenging materials like phosphate powders.
- Low Maintenance and Durability: High-quality components and robust construction ensure long-term reliability, reducing downtime and maintenance costs.
- Customization and Scalability: HeadPowder offers tailored solutions that can be scaled to meet the evolving demands of phosphate production facilities, from small-scale operations to large industrial plants.
With a strong presence in China, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise to deliver reliable and efficient pneumatic conveying solutions for the global phosphate industry. By understanding the specific requirements of each client, we provide systems that enhance productivity, reduce operational costs, and ensure compliance with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
