Wheat flour pneumatic conveying is a critical technology in the food processing industry, enabling efficient and safe transportation of wheat flour from storage to processing or packaging areas. Understanding its working principles and classification applications is essential for optimizing production lines and ensuring product quality. This article provides an in-depth overview of the fundamental mechanisms behind pneumatic conveying for wheat flour, along with its various classification systems and practical applications.
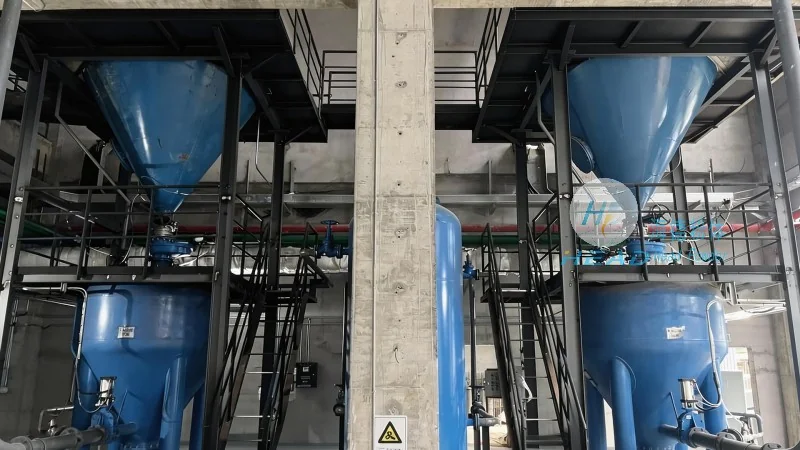
The core principle of pneumatic conveying for wheat flour involves the use of air to transport the material through a pipeline system. This method relies on the creation of a pressure differential or vacuum to move the flour particles. There are two primary modes of operation: pressure conveying and vacuum conveying. In pressure conveying, compressed air is used to push the flour through the pipeline, while vacuum conveying uses a vacuum to draw the material from the source. The choice between these modes depends on factors such as the distance to be covered, the volume of material to be transported, and the required system pressure. The system typically consists of a hopper, a conveying line, a separator, and a receiver. The hopper holds the wheat flour, and the conveying line transports it to the receiver. The separator removes any air or dust from the conveying stream, ensuring that the flour reaches the receiver in a clean and dry state. The working principle also involves the use of appropriate air velocities to prevent material deposition or blockages in the pipeline. For wheat flour, which is a fine powder, maintaining a consistent air velocity is crucial to avoid clogging and ensure smooth operation. The system's design must consider the specific properties of wheat flour, such as its particle size, moisture content, and flowability, to optimize performance.
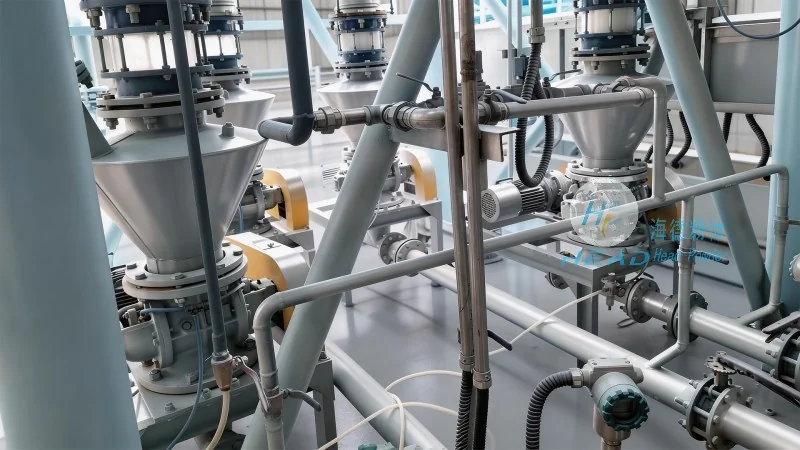
Wheat flour pneumatic conveying systems are classified based on several key factors, including the conveying method, the pressure used, and the application. The main classifications are pressure conveying, vacuum conveying, and mixed conveying. Pressure conveying systems use positive pressure to move the material, typically operating at pressures between 0.5 to 2 bar. These systems are suitable for short to medium distances and high-volume transport. Vacuum conveying systems, on the other hand, use negative pressure to draw the material from the source, operating at pressures below atmospheric. They are ideal for long-distance transport and handling of lighter materials. Mixed conveying systems combine both pressure and vacuum elements, offering flexibility in handling different materials and distances. Within these classifications, there are further subcategories based on the type of air flow, such as dilute phase and dense phase conveying. Dilute phase conveying uses low air-to-material ratios, resulting in high velocity and low pressure drop. It is commonly used for short distances and fine powders like wheat flour. Dense phase conveying, conversely, uses high air-to-material ratios, resulting in low velocity and high pressure drop. This method is suitable for long distances and bulk materials, as it reduces the risk of material degradation and blockages. The classification also considers the system's configuration, such as single-line or multi-line systems, and the presence of additional components like cyclones or filters. Each classification has its advantages and limitations, and the selection depends on the specific requirements of the wheat flour processing facility.
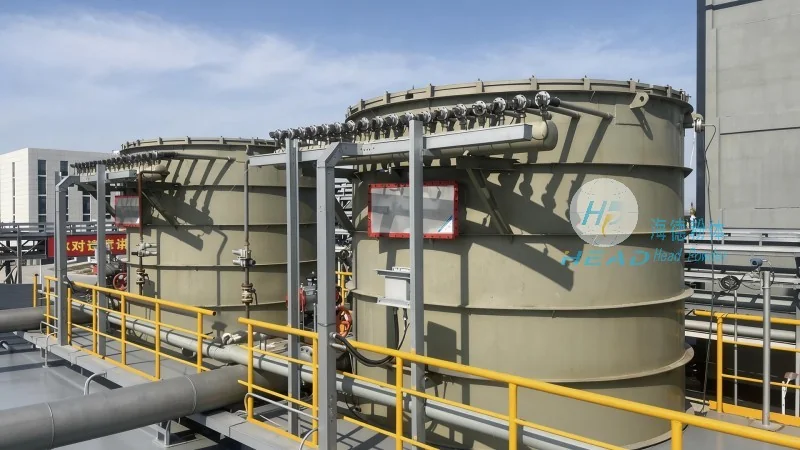
Wheat flour pneumatic conveying is widely used in various stages of wheat flour processing and handling. In the milling industry, it is used to transport wheat flour from the storage silos to the blending and packaging areas. This ensures a continuous and efficient flow of material, reducing downtime and labor costs. The system is also employed in the production of baked goods, where wheat flour is conveyed to mixers or ovens. In the food industry, pneumatic conveying is used to transport wheat flour to ingredient storage or processing lines, ensuring that the material is handled hygienically and safely. Another application is in the packaging of wheat flour, where the flour is conveyed from the production line to the packaging machines. The system's ability to maintain a clean and dry environment is crucial in food processing, as it prevents contamination and ensures product quality. Additionally, pneumatic conveying is used in the handling of wheat flour for distribution, where the material is transported from the mill to the end-users or distribution centers. The technology is also applied in the recycling and reprocessing of wheat flour, where the material is conveyed from waste streams to reprocessing equipment. The versatility of pneumatic conveying makes it suitable for a wide range of applications, from small-scale operations to large industrial facilities.
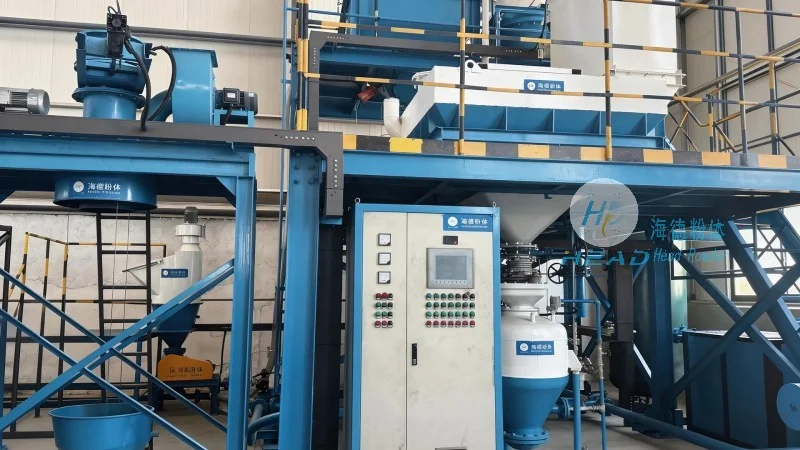
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems for wheat flour and other fine powders. The company specializes in designing, manufacturing, and installing customized conveying solutions tailored to the specific needs of food processing industries. With a focus on quality and innovation, headpowder provides a range of products, including pressure and vacuum conveying systems, dilute and dense phase systems, and advanced separation equipment. The company's products are designed to meet the highest standards of hygiene and safety, ensuring compliance with industry regulations. Headpowder's team of engineers and technicians has extensive experience in the design and implementation of pneumatic conveying systems, and they work closely with clients to develop solutions that optimize production efficiency and reduce operational costs. The company's facilities are equipped with state-of-the-art technology and testing equipment, allowing for the development of high-performance and reliable systems. Headpowder's commitment to customer satisfaction and product excellence has made it a trusted partner for many food processing companies worldwide. The company's headquarters is located in Shandong, China, where it has a strong presence in the industry and access to a skilled workforce and advanced manufacturing capabilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top