Activated carbon powder material conveying lines are specialized systems designed to transport fine powders like activated carbon efficiently and safely. These lines are crucial in industrial applications where handling such powders is essential, such as in chemical processing, environmental treatment, and pharmaceutical manufacturing. The design of these conveying systems must address unique challenges posed by activated carbon's properties, including its fine particle size, potential for dust generation, and the need for contamination control.
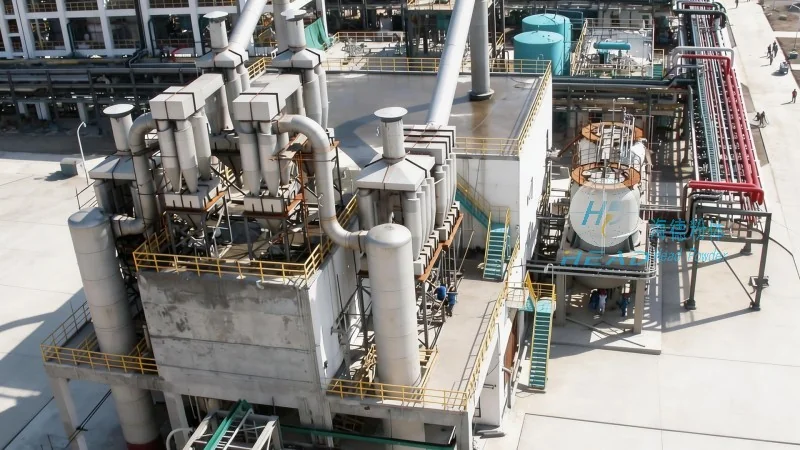
At the core of an activated carbon powder conveying line are several key components that work in tandem to ensure smooth operation. The primary components include a hopper or feeder for material storage and discharge, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), and a control system for regulating flow and pressure. Each component is selected based on the specific characteristics of the activated carbon being handled, including particle size distribution, moisture content, and bulk density. For instance, a screw conveyor may be preferred for dry, free-flowing activated carbon, while a pneumatic conveyor might be more suitable for fine powders that are prone to dusting or require dust control measures.
The design principles of activated carbon powder conveying lines focus on maximizing efficiency, minimizing material loss, and ensuring operational safety. One critical principle is the prevention of dust accumulation and release, which is achieved through proper sealing of hoppers, feeders, and conveyor sections. This is often accomplished using airtight enclosures and dust collection systems to capture any airborne particles. Another key principle is the optimization of flow rates to match the material's bulk density and flow characteristics. Overly high flow rates can lead to blockages or increased wear on components, while too low a rate may result in inefficient use of the system. Engineers typically conduct thorough material testing to determine the optimal conveying velocity and pressure drop for the specific activated carbon being processed.
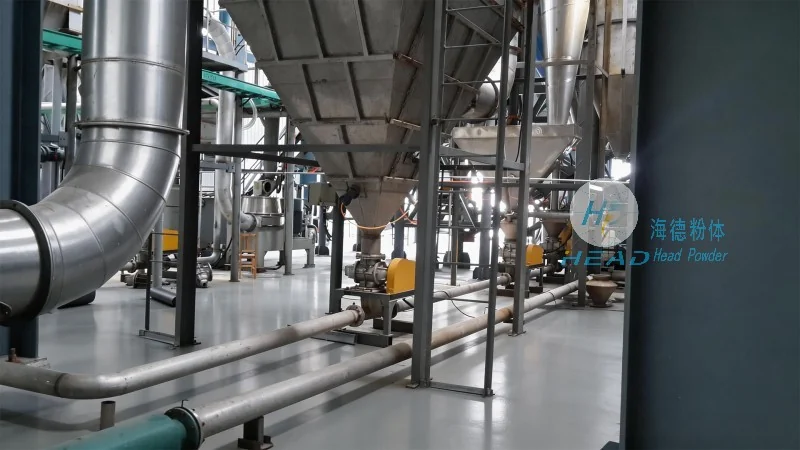
Implementing an activated carbon powder conveying line offers several advantages for industrial operations. Firstly, it enhances process efficiency by automating the material handling process, reducing manual labor and associated errors. This automation also improves consistency in material delivery, ensuring that downstream processes receive a uniform feed of activated carbon. Secondly, these systems help maintain product quality by minimizing exposure to contaminants and preventing cross-contamination between different batches of activated carbon. The enclosed design of many conveying lines also reduces the risk of dust exposure for operators, contributing to a safer working environment. Additionally, by streamlining material transport, these systems can reduce overall operational costs through lower energy consumption and reduced maintenance needs compared to traditional manual handling methods.
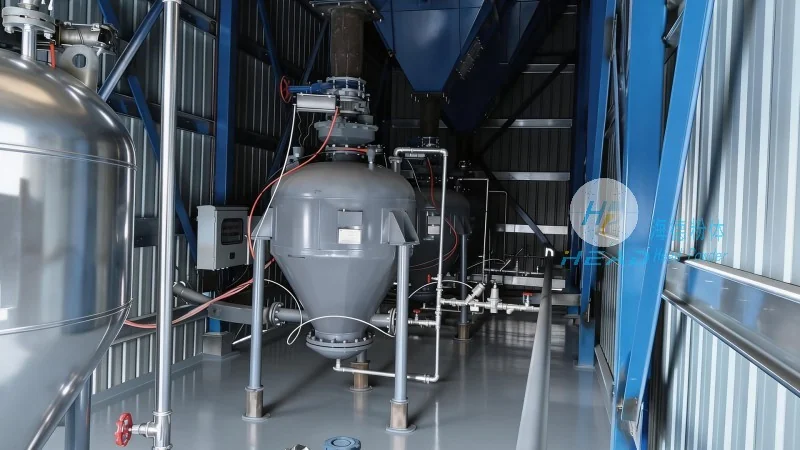
Activated carbon powder conveying lines are widely used in various industrial applications where activated carbon is a critical component. In the chemical industry, these systems are used to transport activated carbon for adsorption processes, such as removing impurities from liquids or gases. In environmental treatment facilities, they help move activated carbon for water and air purification, ensuring effective filtration and treatment. The pharmaceutical industry also relies on such systems for handling activated carbon in drug manufacturing processes, where precision and contamination control are paramount. Each application requires a tailored conveying system design to meet specific operational requirements, such as the need for sterile conditions or the handling of high-purity activated carbon.
Activated carbon powder material conveying lines are essential equipment in industries that rely on activated carbon for their processes. The design and implementation of these systems require careful consideration of the material's properties and the operational goals of the facility. By adhering to established design principles and utilizing appropriate components, manufacturers can ensure efficient, safe, and reliable material handling. The benefits of these systems, including improved efficiency, product quality, and operational safety, make them a valuable investment for any industrial operation dealing with activated carbon powders. As technology advances, ongoing research and development continue to refine the design of these conveying systems, further enhancing their performance and adaptability to meet the evolving needs of industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top