For industrial applications that require precise and efficient handling of bioenzyme materials, a specialized system known as a bioenzyme material handling conveyor is often employed. This equipment is designed to transport various bioenzyme products, such as enzymes used in biotechnology, pharmaceuticals, and food processing, with minimal risk of contamination and optimal preservation of product integrity. The design principles behind these conveyors are centered on maintaining sterile conditions, controlling temperature, and ensuring smooth, continuous movement of the materials through the processing pipeline.
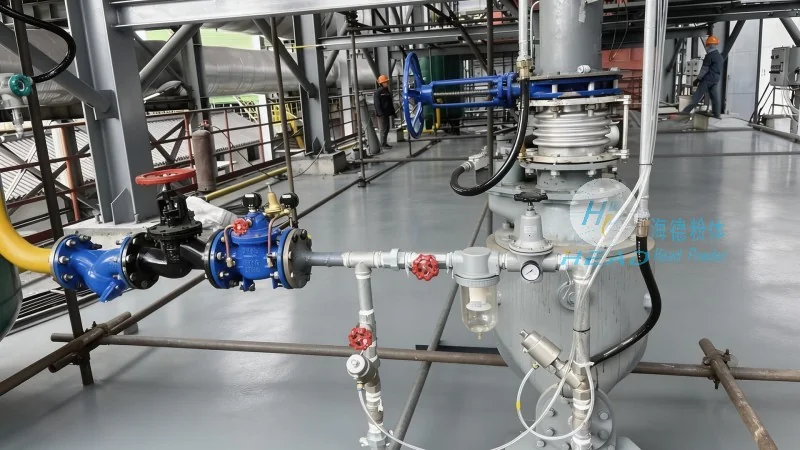
The bioenzyme material handling conveyor typically consists of several key components that work in tandem to achieve efficient material transport. The primary elements include a conveyor belt or chain system, which serves as the main transport medium, and a series of supports or rollers that keep the belt or chain in proper alignment and reduce friction. Additionally, the system may incorporate specialized sealing mechanisms and cleaning ports to maintain a sterile environment and facilitate regular maintenance. The control system, often integrated with sensors and automation technology, monitors the conveyor's operation, ensuring consistent speed and proper material flow. These components are carefully selected and engineered to meet the specific requirements of bioenzyme handling, where contamination control and product quality are paramount.
The design principles of a bioenzyme material handling conveyor are guided by several critical factors that ensure the system operates effectively and safely. First, the system must maintain a sterile environment throughout the material transport process. This is achieved through the use of materials that are resistant to microbial growth, such as stainless steel, and through the implementation of sealing techniques that prevent airborne contaminants from entering the conveyor. Temperature control is another essential design principle, as many bioenzyme products are sensitive to temperature fluctuations. The conveyor may be equipped with heating or cooling elements to maintain a stable temperature, ensuring that the enzymes remain active and functional. Furthermore, the design emphasizes gentle handling of the materials to prevent degradation or denaturation. This is accomplished by using smooth conveyor surfaces and adjustable speed controls that minimize mechanical stress on the bioenzyme products. The overall design also prioritizes ease of cleaning and maintenance, with features like removable parts and automated cleaning cycles that help maintain the system's sterility and operational efficiency.
Bioenzyme material handling conveyors are widely used in various industries where bioenzyme products are processed and transported. In the pharmaceutical industry, these systems are crucial for moving enzymes used in drug manufacturing, ensuring that the products remain sterile and intact during transport. In the food processing sector, they are employed to handle enzymes used in baking, brewing, and dairy production, maintaining the quality and safety of the final products. The benefits of using such conveyors include improved product quality, reduced contamination risks, and enhanced operational efficiency. By maintaining a controlled environment and minimizing human contact with the materials, the system helps to ensure that the bioenzyme products meet stringent quality standards. Additionally, the automation and monitoring features of these conveyors contribute to consistent performance and reduced downtime, making them a valuable asset for any facility that handles bioenzyme materials.
In summary, a bioenzyme material handling conveyor is a specialized piece of equipment designed to efficiently and safely transport bioenzyme materials while maintaining their integrity and sterility. The design principles behind these systems focus on contamination control, temperature regulation, and gentle handling, all of which are critical for preserving the quality of bioenzyme products. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing and supplying high-quality bioenzyme material handling conveyors tailored to the specific needs of various industries. With a commitment to precision engineering and customer satisfaction, HeadPowder ensures that their systems meet the highest standards of performance and reliability. Located in Shandong, China, the company leverages its expertise to deliver innovative solutions that enhance the efficiency and safety of bioenzyme material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top