Small bag dust-free feeding stations represent a critical advancement in powder handling technology, designed to streamline the transfer of bulk powders from sealed bags into processing systems while maintaining stringent cleanliness and safety standards. These machines are indispensable in industries such as pharmaceuticals, food processing, chemicals, and cosmetics, where the integrity of the material and the health of operators are paramount. The following exploration will delve into the fundamental working principles and distinctive features of this specialized equipment, providing a comprehensive understanding of its role in modern industrial operations.
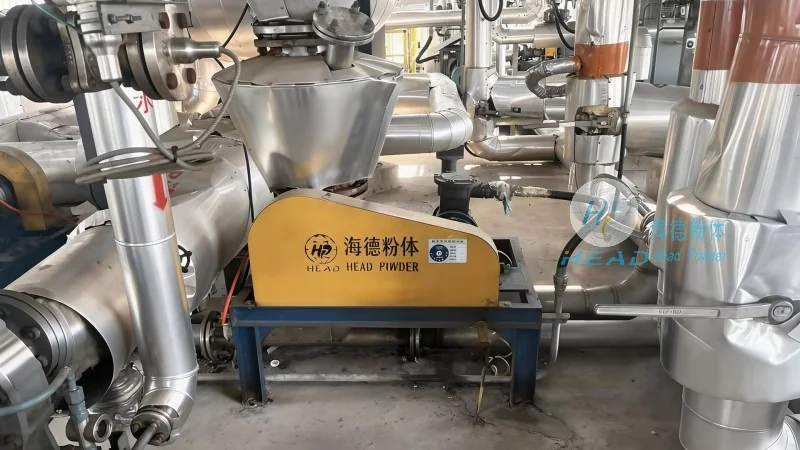
The operational mechanism of a small bag dust-free feeding station is centered on an automated, sealed system that minimizes dust generation and ensures efficient powder transfer. The process typically begins with the placement of a sealed bag onto a designated platform or hopper. Subsequently, an integrated vacuum or pressure differential system is activated, drawing the powder from the bag into a collection hopper or directly into a downstream conveyor. Many models incorporate pre-filter or dust collection components to capture any particles that may escape during the transfer, thereby maintaining a clean environment. The machine is engineered to accommodate a wide variety of powders, including fine powders, granules, and materials with varying moisture contents, adapting to the diverse requirements of different applications. This adaptability is achieved through adjustable parameters such as suction speed, pressure levels, and bag opening mechanisms, allowing operators to customize the process for optimal performance.
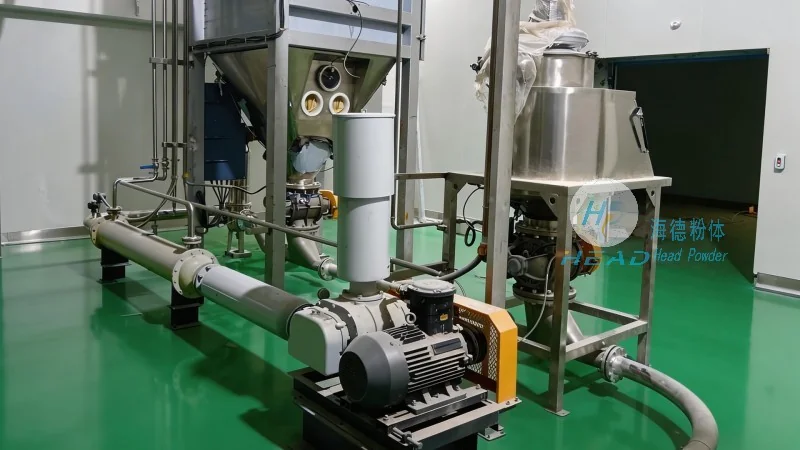
Several key features define the effectiveness and reliability of small bag dust-free feeding stations, making them suitable for demanding industrial environments. The most critical feature is the dust-free operation, which is achieved through sealed housing and integrated filtration systems. This not only safeguards the product from contamination but also preserves a clean working environment, reducing the risk of cross-contamination and ensuring compliance with industry regulations. Another prominent feature is the level of automation, ranging from semi-automatic to fully automated systems. Fully automated models can handle multiple bags without manual intervention, enhancing efficiency and reducing labor costs. The equipment also includes adjustable parameters such as suction speed, pressure, and bag opening methods, enabling customization for different powder types and bag sizes. Additionally, safety features like emergency stop buttons, overload protection, and interlocks are standard, preventing accidental exposure to dust or mechanical hazards. The design is often compact and modular, facilitating easy integration into existing production lines and adaptability to various facility layouts.
Small bag dust-free feeding stations are employed across a broad spectrum of industrial applications where bulk powder handling is essential. In the pharmaceutical industry, they are used to transfer active pharmaceutical ingredients (APIs) and excipients into mixing and processing equipment, ensuring the final product meets stringent purity and quality standards. In the food industry, these machines handle ingredients like flour, sugar, and spices, maintaining food safety and preventing contamination. The chemical industry relies on them to transfer raw materials and intermediates, while the cosmetics industry uses them for powders like pigments and fillers. The benefits of utilizing this equipment include improved product quality through reduced contamination, increased operational efficiency via automation, and enhanced operator safety by minimizing exposure to dust and hazardous materials. Furthermore, the equipment reduces material waste by ensuring accurate and complete transfer from the bag, minimizing losses and associated costs. These advantages make small bag dust-free feeding stations a valuable investment for businesses seeking to optimize their powder handling processes.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of specialized powder handling equipment, including small bag dust-free feeding stations. The company is headquartered in Shandong, China, and has established a strong reputation for producing high-quality, reliable equipment tailored to the needs of various industries. HeadPowder’s engineering and manufacturing processes focus on durability, efficiency, and ease of maintenance, ensuring long-term performance and customer satisfaction. The company provides comprehensive support, including technical assistance, installation services, and after-sales support, to help customers maximize the benefits of their equipment. With a commitment to innovation and customer-centric solutions, HeadPowder continuously develops new technologies to meet the evolving demands of the powder handling industry. Their expertise and dedication to quality have made them a trusted partner for businesses seeking reliable powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top