For industries dealing with hydroxide cobalt powder, efficient and reliable handling equipment is crucial. The hydroxide cobalt powder conveyor, a specialized device designed for transporting this specific material, plays a vital role in various production processes. This article will explore the working principle and key features of such conveyors, providing insights into their functionality and benefits.
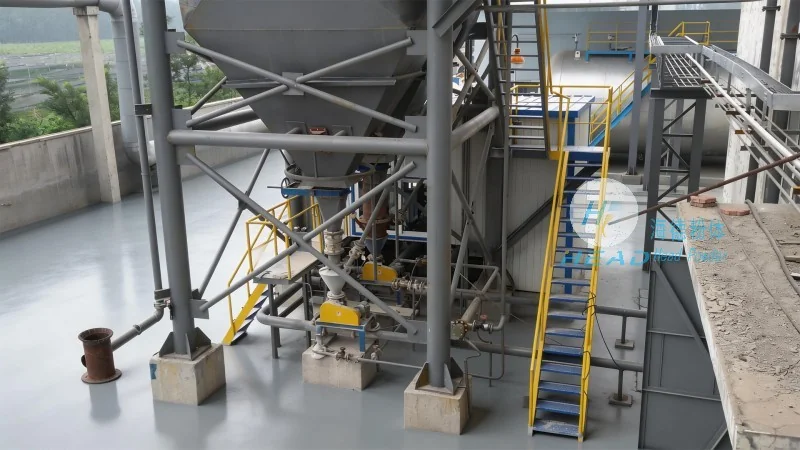
The hydroxide cobalt powder conveyor operates based on principles that ensure safe and efficient material transport. Typically, these systems utilize a combination of mechanical components and control mechanisms to move the powder from one location to another. The process begins with the feeding of hydroxide cobalt powder into the conveyor system. The powder is then conveyed through a series of components, such as belts, screws, or pneumatic tubes, depending on the design of the conveyor. The mechanical action, whether through friction or pressure, moves the powder along the designated path. Additionally, the conveyor may incorporate features like vibration or agitation to prevent clogging and ensure uniform flow. The control system, often integrated with sensors and automation, monitors the flow rate and adjusts the operation as needed to maintain optimal performance. This systematic approach ensures that the hydroxide cobalt powder is transported with minimal loss and maximum efficiency.
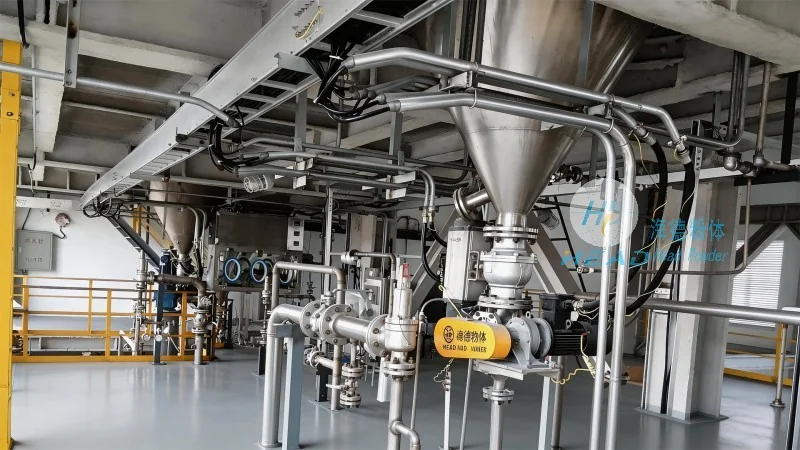
Several key features distinguish hydroxide cobalt powder conveyors from other handling equipment. Firstly, their design is tailored to handle the specific properties of hydroxide cobalt powder, which may include high moisture content or fine particle size. The materials used in the construction of the conveyor, such as corrosion-resistant metals or specialized coatings, protect against chemical reactions and ensure durability. Secondly, the conveyor systems are equipped with advanced sealing mechanisms to prevent dust leakage and maintain a clean working environment. This is particularly important in industries where dust control is a regulatory requirement. Thirdly, the conveyors often include features for easy maintenance and cleaning, such as removable components and self-cleaning designs. This reduces downtime and operational costs. Furthermore, the integration of sensors and monitoring systems allows for real-time tracking of the powder flow, enabling quick detection of any issues and prompt maintenance. These features collectively enhance the performance and reliability of the conveyor, making it suitable for continuous production environments.
Hydroxide cobalt powder conveyors are widely used in various industrial applications, particularly in the battery manufacturing and chemical processing sectors. In battery production, these conveyors are essential for transporting hydroxide cobalt, a critical component in lithium-ion batteries. The efficient handling of this material ensures consistent quality and reduces production delays. In chemical processing, the conveyors facilitate the movement of hydroxide cobalt between different processing stages, such as drying, grinding, and mixing. The benefits of using these conveyors include improved productivity, reduced labor costs, and enhanced safety due to minimized manual handling of the powder. Additionally, the consistent flow of material helps maintain the quality of the final product, as any variations in the powder's characteristics can affect the performance of the end product. The reliability of the conveyor system also contributes to overall operational efficiency, as it minimizes interruptions and ensures a steady supply of material to downstream processes.
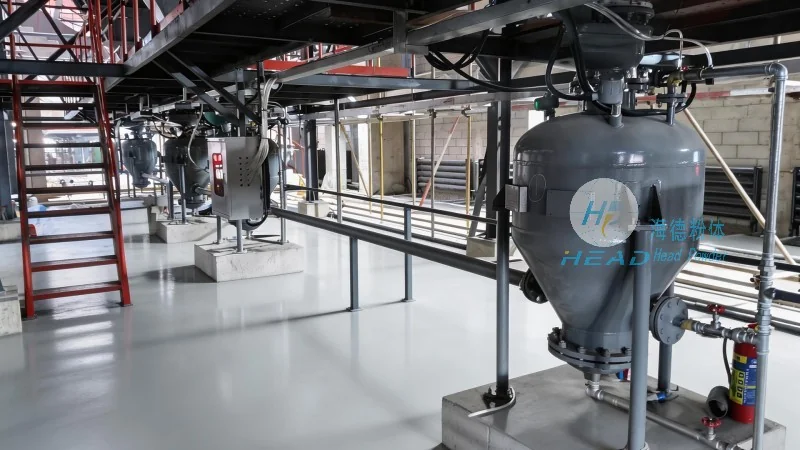
In conclusion, hydroxide cobalt powder conveyors are sophisticated equipment designed to handle the unique challenges of transporting hydroxide cobalt powder. Their working principle, which combines mechanical and control systems, ensures efficient and safe material transport. The key features, including specialized construction, sealing mechanisms, and monitoring systems, enhance their performance and reliability. These conveyors play a crucial role in industrial settings, particularly in battery and chemical manufacturing, by improving productivity and maintaining product quality. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing high-quality hydroxide cobalt powder conveyors that meet the specific needs of various industries. With their expertise and commitment to quality, the company ensures that clients receive reliable and efficient equipment for their material handling requirements. HeadPowder, as the company is commonly known, is dedicated to delivering solutions that enhance operational efficiency and support the growth of their clients' businesses.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top