Calcium nitrite powder conveyors are specialized industrial equipment engineered to facilitate the efficient and safe transportation of calcium nitrite powder, a chemical compound with significant applications in sectors like corrosion inhibition, food preservation, and water treatment. As a reactive and potentially hazardous material, the handling of calcium nitrite powder requires precise control and specialized equipment to mitigate risks such as dust explosion, material degradation, and operational inefficiencies. The design and operation of these conveyors are tailored to address the unique properties of calcium nitrite, including its flowability, reactivity, and the need for sealed, dust-free environments. This equipment plays a critical role in ensuring consistent material flow, maintaining product integrity, and enhancing overall process safety in industrial settings.
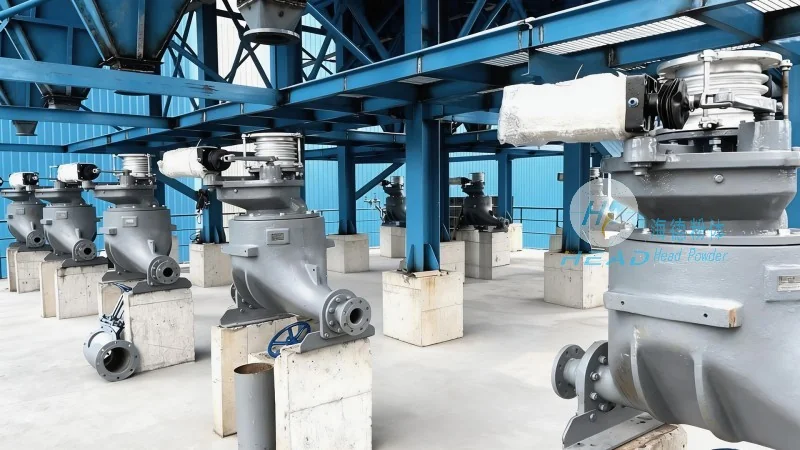
HeadPowder, the manufacturer behind these calcium nitrite powder conveyors, is a leading engineering company based in Shandong, China. Specializing in powder handling and conveying systems, HeadPowder has built a reputation for delivering high-quality, customized solutions tailored to the diverse needs of the chemical, food, and water treatment industries. The company’s headquarters, located in Shandong, serves as a hub for research, development, and manufacturing, leveraging local expertise and advanced technology to produce reliable equipment. HeadPowder’s commitment to innovation, quality, and customer satisfaction is reflected in its comprehensive product line, which includes a range of conveyors designed to handle various powder types, including calcium nitrite. The company’s engineering team works closely with clients to understand their specific requirements and develop solutions that optimize performance, reduce costs, and enhance safety.
The working principle of calcium nitrite powder conveyors typically involves a combination of mechanical and pneumatic components working in tandem to move the powder from a source to a destination. The process generally begins with a feed hopper or silo that stores the calcium nitrite powder, ensuring a continuous supply of material. From the hopper, the powder is transferred to a conveyor system, which can be either a screw conveyor or a pneumatic conveyor, depending on the application. For screw conveyors, the mechanism relies on a rotating screw (or auger) that pushes the powder forward through a closed tube. The speed of the screw can be adjusted to control the flow rate, allowing for precise regulation of the material's movement. In pneumatic conveyors, air pressure is used to create a flow of the powder through a pipeline. The system includes a blower or compressor that generates the necessary air pressure, and the powder is carried along with the air stream. For calcium nitrite, the conveyor must be designed to handle the powder's characteristics, such as its tendency to generate dust and its potential for caking. The system also incorporates control mechanisms, such as variable frequency drives (VFDs) and pressure sensors, to monitor and adjust the flow rate and pressure, ensuring smooth operation and preventing blockages or material loss. Additionally, safety features like emergency stop buttons and overload protection are integrated to safeguard operators and equipment.
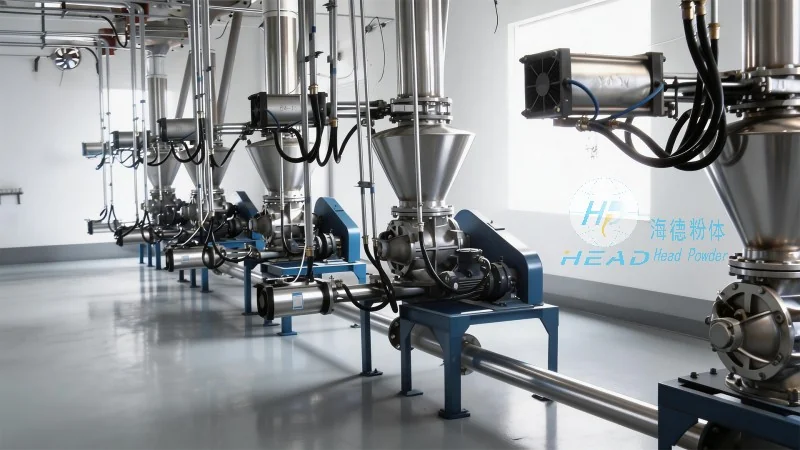
Calcium nitrite powder conveyors from HeadPowder are distinguished by several key features that enhance their performance, reliability, and safety. One of the primary features is the use of durable, corrosion-resistant materials, such as stainless steel (e.g., 304 or 316), to withstand the chemical properties of calcium nitrite and prevent material degradation or equipment failure. The equipment is also constructed with sealed systems and dust-tight designs to minimize the release of powder into the environment, ensuring compliance with occupational health and safety regulations. Another critical feature is the integration of advanced control systems, including PLC (Programmable Logic Controller) technology, which allows for precise regulation of the conveyor's speed, pressure, and flow rate. These controls adapt to changes in the powder's characteristics or process requirements, maintaining optimal performance. The conveyors are equipped with safety features like emergency stop buttons, overload protection, and interlocks to prevent accidents and ensure the safety of operators. Energy efficiency is also a key consideration, with designs optimized to reduce power consumption while maintaining high throughput. Additionally, the equipment is designed for easy maintenance, with accessible components and modular construction that simplifies repairs and replacements. These features collectively contribute to the overall effectiveness and longevity of the calcium nitrite powder conveyors, making them a preferred choice for industrial applications.
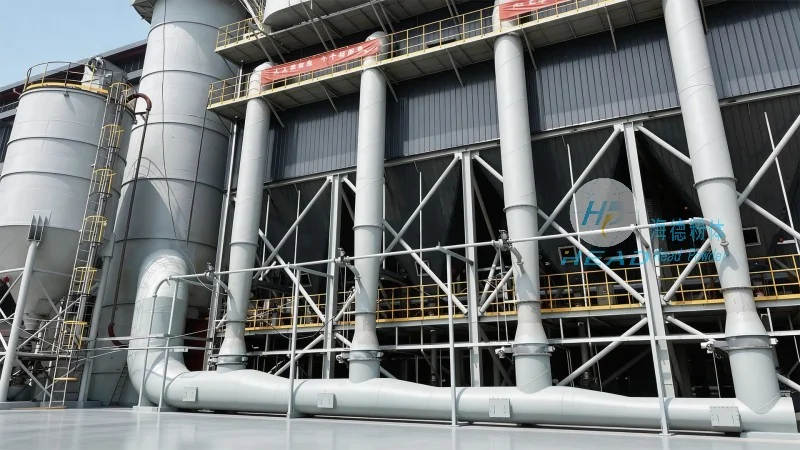
The calcium nitrite powder conveyors are widely utilized in various industrial applications where the efficient handling of calcium nitrite is essential. In the chemical industry, these conveyors are used in the production of calcium nitrite-based products, such as corrosion inhibitors and other chemical intermediates. The equipment facilitates the transport of raw materials and finished products, ensuring consistent quality and reducing material loss. In the food industry, calcium nitrite is used as a preservative in meat products, and the conveyors help in the precise handling of this ingredient, maintaining its purity and preventing contamination. The water treatment industry also relies on calcium nitrite powder conveyors to transport the chemical for corrosion control in water systems, ensuring the longevity of infrastructure and the safety of water supplies. The benefits of using these conveyors include improved process efficiency, reduced downtime, and enhanced safety. The equipment's ability to handle the powder's properties ensures consistent flow and prevents issues like blockages or dust explosions. The durability and corrosion resistance of the materials used in the conveyor systems contribute to long-term reliability and lower maintenance costs. Overall, the calcium nitrite powder conveyors from HeadPowder provide a reliable and efficient solution for the transportation of calcium nitrite powder, supporting the smooth operation of industrial processes and meeting the stringent requirements of various industries.
In conclusion, calcium nitrite powder conveyors are essential equipment for the safe and efficient handling of calcium nitrite powder in industrial applications. The working principle, which combines mechanical and pneumatic components with advanced control systems, ensures precise and reliable material transport. Key features such as corrosion-resistant materials, sealed designs, and safety mechanisms enhance performance and safety. HeadPowder, with its headquarters in Shandong, China, has established itself as a leading provider of these conveyors, offering customized solutions tailored to the needs of various industries. The use of these conveyors not only improves process efficiency but also reduces risks associated with handling reactive materials like calcium nitrite. As industrial demands for safe and efficient powder handling continue to grow, calcium nitrite powder conveyors remain a critical component in ensuring the smooth operation of industrial processes and meeting the stringent requirements of various industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top