Coal ash, a byproduct of coal combustion, is a valuable resource that requires efficient handling and transportation. Coal ash powder conveyors are specialized equipment designed to transport this fine material safely and effectively. These systems are widely used in industrial settings, particularly by companies like Shandong HeadPowder Engineering Co., Ltd., which specializes in providing advanced material handling solutions for power plants and other facilities.
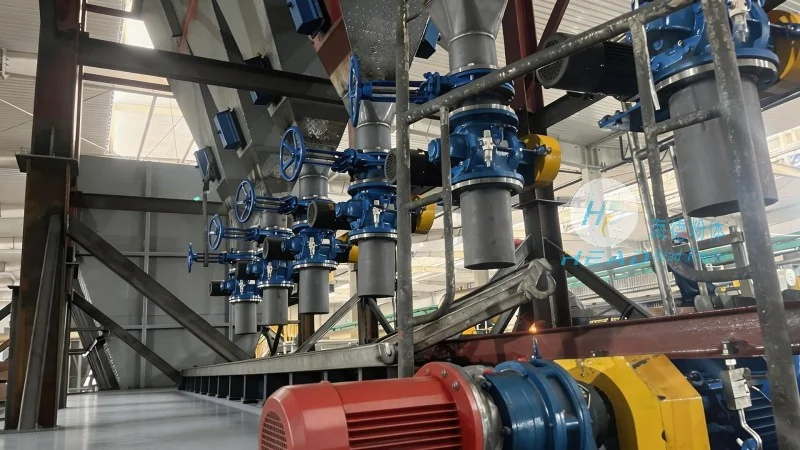
Coal ash powder conveyors are essential equipment used in power plants and other industrial facilities to transport coal ash from storage areas to processing or disposal sites. These systems are engineered to handle the unique properties of coal ash, such as its fine particle size, abrasive nature, and potential moisture content. The primary goal of these conveyors is to ensure reliable, low-maintenance operation while minimizing environmental impact. Shandong HeadPowder Engineering Co., Ltd., based in China, is a leading manufacturer of such equipment, known for their innovative designs and commitment to quality.
The operation of coal ash powder conveyors typically involves a combination of mechanical and sometimes pneumatic components. The most common type is the screw conveyor, which uses a rotating helical screw to move the material forward. As the screw rotates, it pushes the coal ash through the conveyor tube, maintaining a consistent flow rate. This design is particularly effective for handling dry coal ash, as it prevents clogging and ensures smooth transport. For more challenging applications, such as transporting wet or sticky coal ash, pneumatic conveyors may be employed. These systems use air pressure to create a flow of material through a pipeline. The coal ash is suspended in the air stream and transported to the destination. Pneumatic conveyors offer flexibility in layout and can handle longer distances, but they require more energy and may be less efficient for very fine particles.
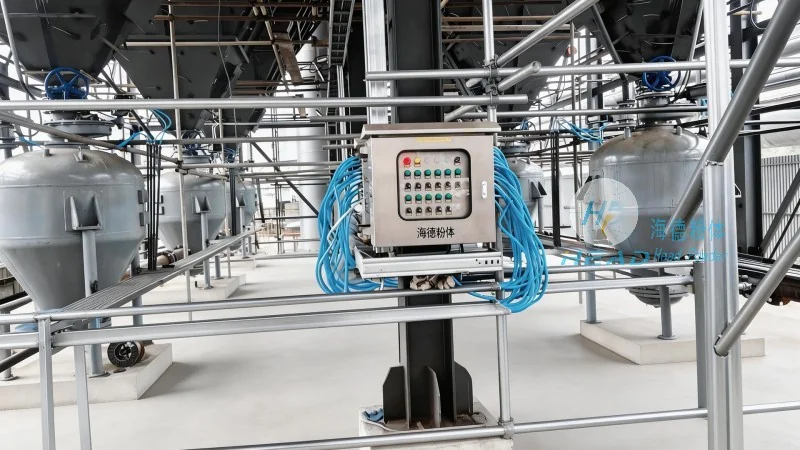
Coal ash powder conveyors are designed with several features that enhance their performance and reliability. One of the most important features is the material of construction. High-quality, corrosion-resistant materials, such as stainless steel or special alloys, are used to withstand the abrasive nature of coal ash and prevent wear and tear. This ensures a longer service life and reduces maintenance costs. The company, Shandong HeadPowder Engineering Co., Ltd., utilizes advanced materials in their designs to meet the demanding requirements of coal ash handling. Another critical feature is the sealing system. Coal ash can be dusty and potentially hazardous, so effective sealing is essential to prevent leakage and protect the environment. Advanced sealing technologies, including double-flanged seals and air-tight connections, are used to maintain a safe and clean operation. This also helps to comply with environmental regulations and reduce the risk of dust exposure for personnel.
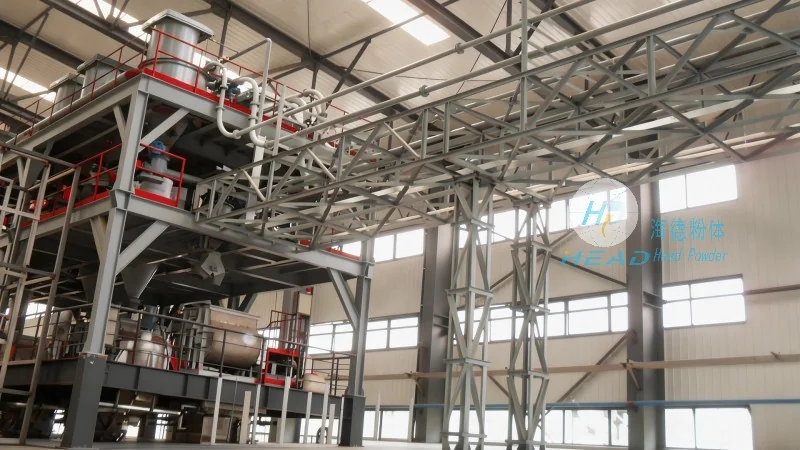
Efficiency and energy consumption are also key considerations. Modern coal ash powder conveyors are designed to operate with minimal energy input while maintaining high throughput. Variable speed drives and optimized screw designs help to adjust the conveyor speed according to the material flow, reducing energy waste. Additionally, the use of high-efficiency motors and proper maintenance schedules ensures optimal performance over time. Shandong HeadPowder Engineering Co., Ltd. focuses on energy-efficient solutions to help their clients reduce operational costs and environmental footprint.
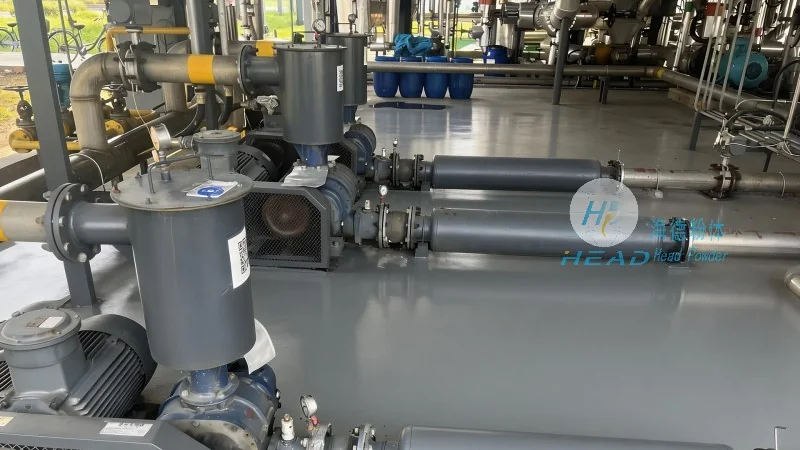
Coal ash powder conveyors are widely used in various industrial applications, including power generation, cement production, and waste management. Their ability to handle large volumes of coal ash efficiently makes them indispensable in these sectors. The benefits of using these conveyors include improved safety, reduced labor costs, and enhanced environmental compliance. By automating the transport process, facilities can minimize manual handling, which reduces the risk of accidents and exposure to hazardous materials. Furthermore, the efficient transport of coal ash allows for better utilization of this resource. Coal ash can be used as a raw material in cement production, reducing the need for natural aggregates and contributing to sustainable construction practices. The conveyors play a crucial role in making this process feasible by ensuring the material is transported reliably and in the right condition.
In conclusion, coal ash powder conveyors are sophisticated equipment that play a vital role in the management of coal ash. Their working principle, which combines mechanical and pneumatic technologies, allows for efficient and reliable transport of fine materials. The key features, including robust construction, effective sealing, and energy-efficient operation, ensure that these conveyors meet the demanding requirements of industrial applications. By understanding the working principle and features of these systems, facilities can make informed decisions about their material handling strategies, ultimately leading to improved operational efficiency and environmental sustainability. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of advanced coal ash powder conveyors, providing solutions that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top