Quartz powder, a widely used raw material in various industrial applications, often requires efficient and reliable transport solutions to ensure smooth production processes. The pneumatic conveying system has emerged as a preferred method for handling quartz powder due to its advantages in terms of hygiene, safety, and operational flexibility. This article provides a comprehensive overview of the quartz powder pneumatic conveying system, exploring its components, working principles, and practical applications.
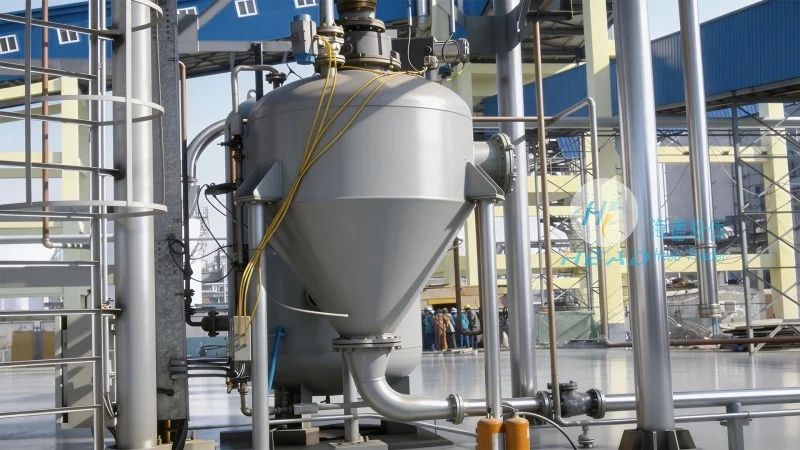
The quartz powder pneumatic conveying system consists of several critical components that work in tandem to achieve effective material transport. The primary components include the hopper, feeder, air compressor, conveying line, and receiver. The hopper serves as the storage container for the quartz powder, ensuring a consistent feed supply. The feeder, typically a rotary valve or a screw feeder, regulates the flow of powder into the conveying line. The air compressor generates the necessary air pressure to move the powder particles through the system. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the powder and air mixture. Finally, the receiver collects the delivered quartz powder, separating it from the air.
The operation of a quartz powder pneumatic conveying system is based on the principle of air movement and particle suspension. In a positive pressure system, the air compressor forces compressed air into the conveying line, creating a pressure differential that propels the quartz powder particles along with the air. The powder is suspended in the air stream, allowing it to travel through the system without clogging. In contrast, a negative pressure system draws air and powder from the hopper into the receiver, creating a vacuum that pulls the material. Both systems are designed to handle different material characteristics and operational requirements, with positive pressure systems being more common for long-distance and high-capacity applications.
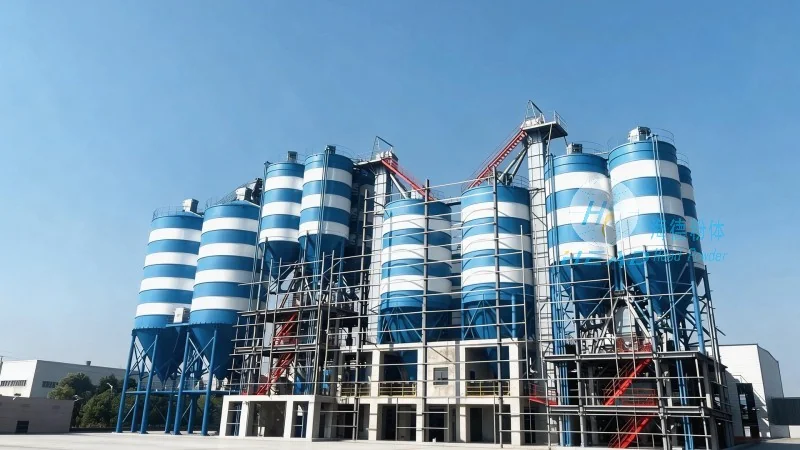
Implementing a pneumatic conveying system for quartz powder offers numerous benefits that enhance operational efficiency and product quality. One of the key advantages is the ability to maintain a dust-free environment, which is crucial for maintaining product purity and ensuring compliance with industrial hygiene standards. Unlike mechanical conveying methods, which may generate dust and cause contamination, pneumatic systems minimize particle loss and reduce the risk of cross-contamination. Additionally, pneumatic conveying allows for precise control over the flow rate and pressure, enabling operators to adjust the system according to production needs. This flexibility is particularly valuable in industries where quartz powder is used in sensitive applications, such as pharmaceuticals or food processing.
The quartz powder pneumatic conveying system is widely utilized across various industries, including ceramics, glass manufacturing, and chemical processing. In the ceramics industry, for example, quartz powder is used as a raw material for producing tiles and sanitaryware. The pneumatic system efficiently transports the powder from storage to the production line, ensuring consistent quality and reducing downtime. In glass manufacturing, quartz powder is essential for glass composition, and the conveying system helps maintain the purity of the material, which is critical for achieving the desired optical properties. Similarly, in chemical processing, the system aids in the transport of quartz powder used in the production of silica-based products, ensuring a continuous supply to reactors and processing units.
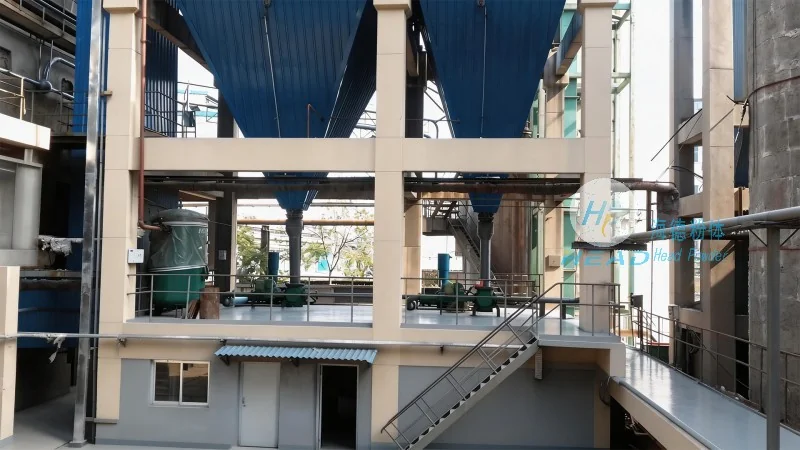
When designing and installing a quartz powder pneumatic conveying system, several factors must be considered to ensure optimal performance and longevity. The first consideration is the material characteristics of the quartz powder, including particle size, density, and moisture content. These factors influence the selection of the feeder type and the air pressure required for effective conveying. For instance, fine quartz powders may require higher air velocities to prevent clogging, while larger particles may need lower velocities to maintain stability. Another critical factor is the system layout, which should be designed to minimize pressure losses and ensure smooth material flow. Proper sealing of components, such as the hopper and feeder, is essential to prevent air leakage and maintain system efficiency. Additionally, regular maintenance and cleaning are necessary to prevent the buildup of powder residue, which can affect system performance over time.
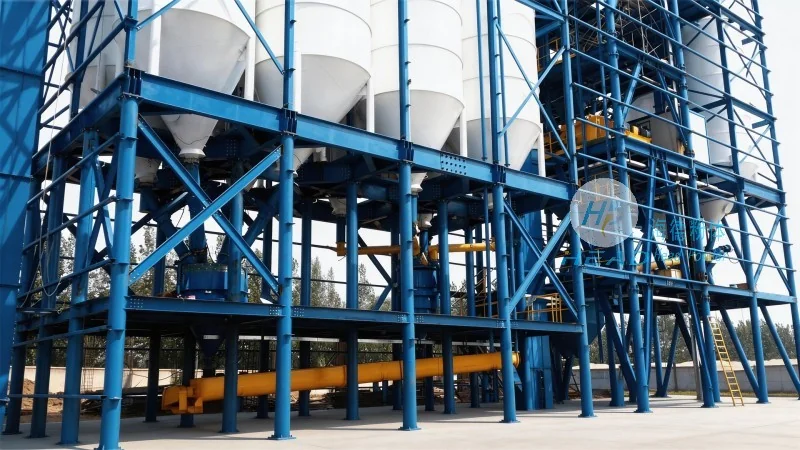
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, has successfully implemented quartz powder pneumatic conveying systems for numerous clients. One notable case involved a ceramics manufacturer in China that faced challenges with traditional mechanical conveying methods, which resulted in dust accumulation and product contamination. By installing a customized positive pressure pneumatic system, the company was able to achieve a dust-free environment and improve product quality. The system was designed to handle large volumes of quartz powder, with a capacity of 10 tons per hour, and included features such as automatic feeding and pressure monitoring. The client reported a significant reduction in maintenance costs and an increase in production efficiency, highlighting the effectiveness of the system. This case study demonstrates the practical benefits of pneumatic conveying for handling quartz powder and the expertise of Shandong HeadPowder in delivering tailored solutions.
In conclusion, the quartz powder pneumatic conveying system is a highly effective and reliable solution for transporting quartz powder in industrial applications. By leveraging the principles of air movement and particle suspension, the system offers advantages such as dust-free operation, precise control, and flexibility. As industries continue to demand higher quality and efficiency in their production processes, the adoption of advanced pneumatic conveying systems will likely increase. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technology, providing customized solutions that meet the specific needs of clients. With its expertise in system design and installation, the company continues to contribute to the advancement of quartz powder handling in various industrial sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top