Phosphate fertilizer powder pneumatic conveying systems represent a critical technology in the modern fertilizer industry, designed to efficiently transport fine powders like phosphate over long distances with minimal loss and high reliability. This system is particularly essential for the handling of phosphatic materials, which are often sensitive to moisture and require precise control during transport. The following sections provide a detailed overview of the key components, operational principles, and practical applications of such systems, tailored for professionals in the fertilizer processing sector.
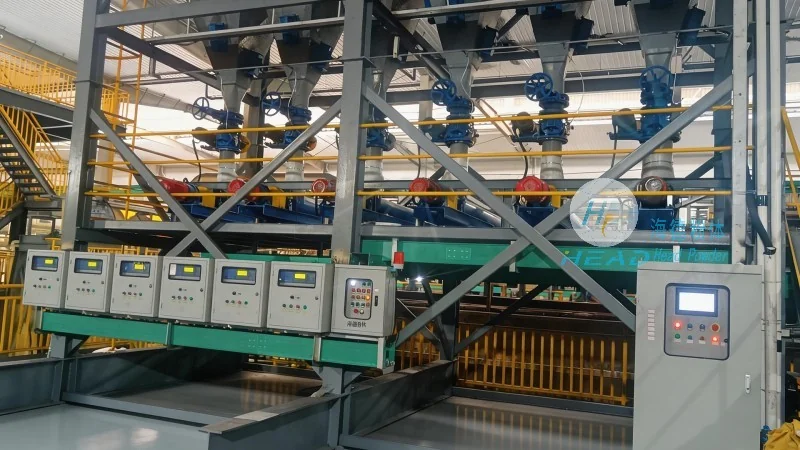
The core components of a phosphate fertilizer powder pneumatic conveying system include the material hopper, feeder, conveying line, and receiver. The material hopper serves as the storage vessel, holding the phosphate powder in a controlled environment to prevent moisture absorption and agglomeration. A rotary or vibratory feeder then meters the powder at a consistent rate into the conveying line. The conveying line itself is typically made of stainless steel or other corrosion-resistant materials to accommodate the chemical properties of phosphate fertilizers. The system may employ either positive or negative pressure modes, with positive pressure systems using a blower to force air and powder through the line, while negative pressure systems use a vacuum to draw the material. The receiver is the final storage or processing container, where the phosphate powder is deposited after transport.
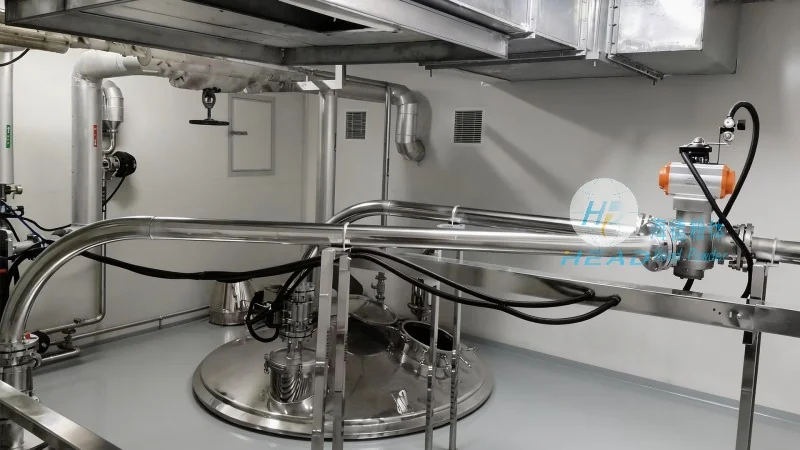
The operational principle of a pneumatic conveying system involves the suspension of phosphate powder particles in a stream of air, creating a slurry-like mixture that can be transported through pipelines. The efficiency of this process depends on several factors, including the particle size distribution of the phosphate powder, the air velocity within the conveying line, and the system's pressure differential. For fine phosphate powders, maintaining an appropriate air-to-solid ratio is crucial to prevent blockages and ensure smooth flow. The system's design must also account for the potential for particle segregation or agglomeration, which can impact downstream processing steps. Advanced control systems are often integrated to monitor and adjust parameters such as air pressure, flow rate, and material feed rate in real-time, optimizing the conveying efficiency and minimizing energy consumption.
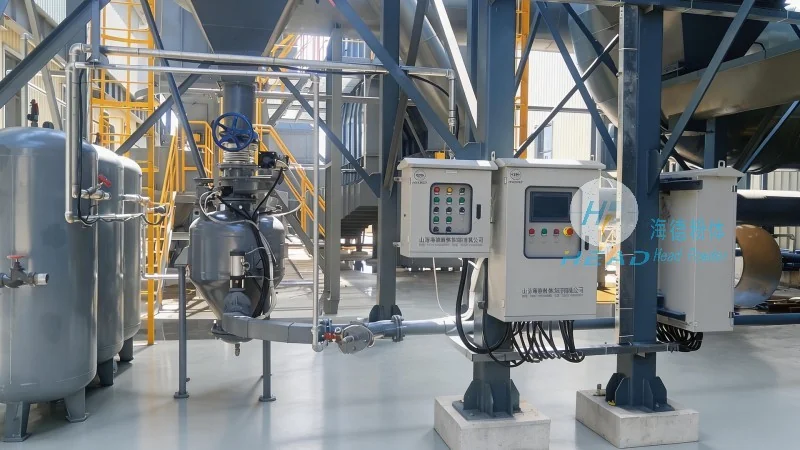
Phosphate fertilizer powder pneumatic conveying systems are widely used in various stages of fertilizer production, from raw material handling to final product packaging. In the raw material stage, these systems efficiently transport phosphate ore or concentrate from storage silos to grinding mills. During the grinding process, the fine phosphate powder is conveyed to mixing and blending units, where it is combined with other nutrients and additives. The system's ability to handle fine powders with minimal degradation makes it ideal for maintaining product quality and consistency. Additionally, in the packaging and distribution phase, pneumatic conveying systems can transport finished phosphate fertilizer products to storage tanks or loading facilities, ensuring a seamless supply chain. The reliability and scalability of these systems make them a preferred choice for both small-scale and large-scale fertilizer operations.
Implementing a phosphate fertilizer powder pneumatic conveying system offers several advantages, including high transport capacity, reduced material handling costs, and improved safety compared to traditional methods like bucket elevators or belt conveyors. The systems are also relatively compact, allowing for installation in confined spaces within fertilizer plants. However, challenges such as system maintenance, pressure drop management, and the prevention of material buildup in pipelines remain critical considerations. Regular maintenance, including cleaning and inspection of the conveying line and components, is essential to ensure long-term system performance. Additionally, the selection of appropriate materials for the conveying line and components is vital to resist corrosion from the acidic nature of phosphate fertilizers.
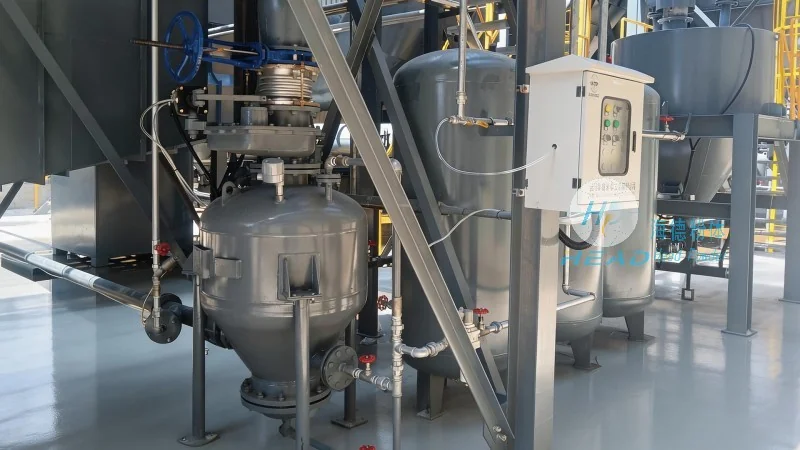
Phosphate fertilizer powder pneumatic conveying systems play a pivotal role in enhancing the efficiency and sustainability of modern fertilizer production. By providing a reliable and efficient means of transporting fine phosphate powders, these systems contribute to improved product quality, reduced operational costs, and enhanced safety in fertilizer processing facilities. As the fertilizer industry continues to evolve, the adoption of advanced pneumatic conveying technologies will remain essential for meeting the growing demand for high-quality phosphate fertilizers. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd., with their focus on tailored solutions for phosphate powder handling, underscores the importance of specialized engineering in optimizing material transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top