Wheat flour pneumatic conveying systems represent a sophisticated and efficient method for transporting bulk materials, particularly in the food processing industry. This technology has become increasingly vital for businesses dealing with wheat flour, as it offers a range of advantages over traditional mechanical conveying methods. In this article, we will delve into the intricacies of such systems, exploring their design, functionality, and practical applications.
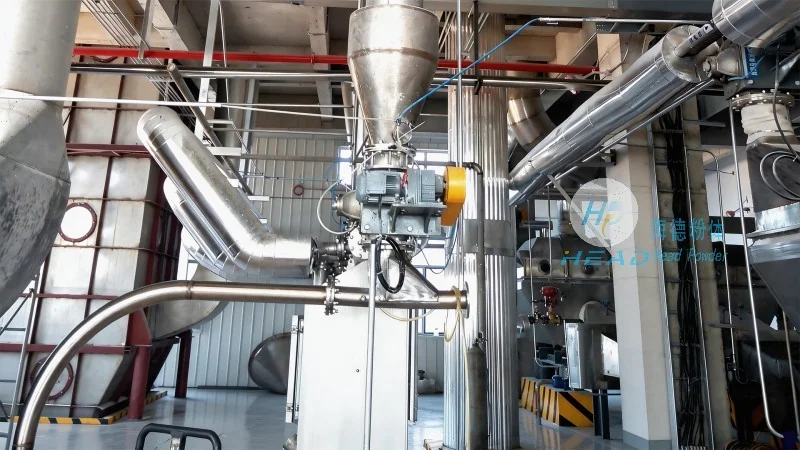
Pneumatic conveying systems operate by using air or other gases to transport bulk materials through a network of pipes. The core principle involves creating a pressure differential to move the material from the source to the destination. There are primarily two types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push the material, while vacuum systems use a vacuum to pull it. For wheat flour, which is a fine, powdery substance, pressure systems are often preferred due to their ability to handle high volumes and maintain product quality.
At the heart of any pneumatic conveying system are several critical components that work in tandem to ensure smooth operation. The main components include the hopper or feed bin, which holds the wheat flour; the conveyor itself, which may consist of a series of pipes and ducts; the air mover, which provides the necessary pressure or vacuum; and the control system, which regulates the flow and pressure. Additionally, there are often accessories such as filters, cyclones, and dust collectors to maintain air quality and prevent product contamination. These components are meticulously designed to handle the unique properties of wheat flour, including its fine particle size and potential for static buildup.
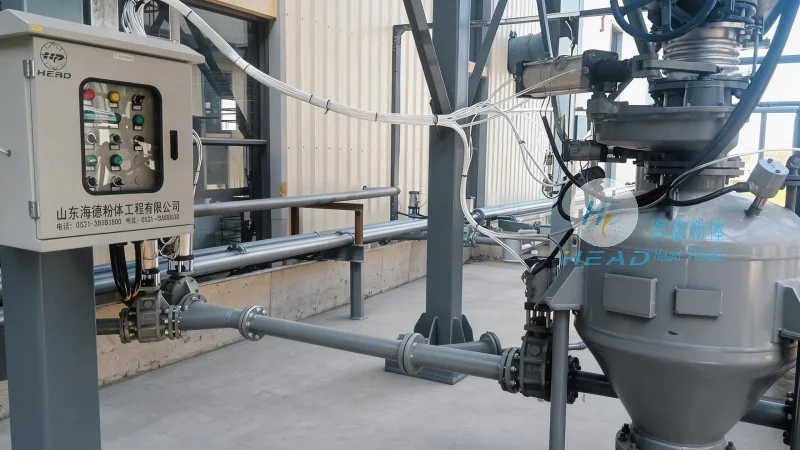
Implementing a pneumatic conveying system for wheat flour offers numerous benefits that enhance operational efficiency and product integrity. One of the most significant advantages is the reduction in product degradation. Unlike mechanical systems that may cause friction and heat buildup, pneumatic conveying minimizes these factors, preserving the quality and freshness of the flour. Additionally, these systems are highly flexible, allowing for easy reconfiguration and expansion as production needs change. They also reduce labor costs by automating the material handling process and minimizing the need for manual handling, which can be hazardous with fine powders. Furthermore, pneumatic conveying systems are more hygienic and easier to clean, which is crucial for food-grade applications where compliance with regulatory standards is paramount.
Wheat flour pneumatic conveying systems are widely used across various stages of the food production process. In milling operations, they efficiently transport raw wheat to the grinding mills and then move the resulting flour to storage silos. During packaging, these systems can deliver flour directly to filling machines, ensuring a continuous and clean supply. In bakeries and food processing plants, they are used to transfer flour from storage to production lines, maintaining a consistent flow of raw material. The versatility of pneumatic conveying makes it suitable for both large-scale industrial operations and smaller commercial bakeries, adapting to different production capacities and layouts.
Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing customized pneumatic conveying systems tailored to specific customer needs. Their expertise lies in integrating these systems with existing facilities, ensuring seamless operation without disrupting current production processes. The engineers at HeadPowder work closely with clients to assess their unique requirements, such as the volume of flour to be handled, the distance of transport, and the desired level of automation. By leveraging advanced engineering and material science, they develop solutions that optimize performance while minimizing energy consumption and maintenance costs. This customized approach ensures that each system is optimized for the specific application, providing long-term benefits and reliability.
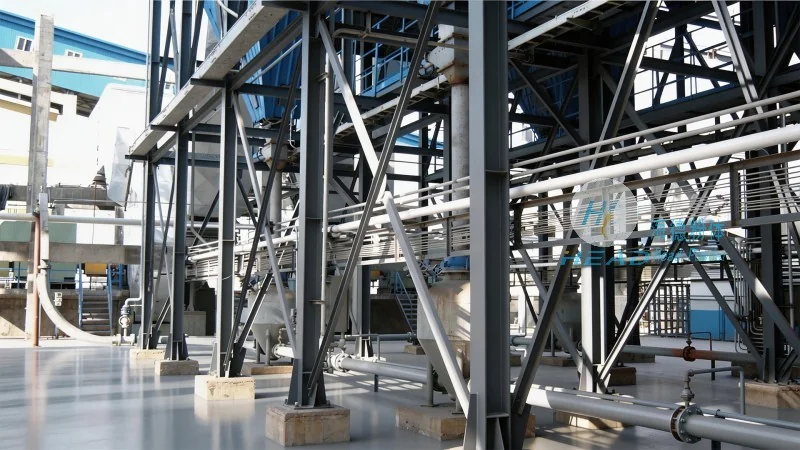
Proper maintenance is essential to ensure the longevity and efficiency of a wheat flour pneumatic conveying system. Regular cleaning of the pipes, filters, and cyclones is crucial to prevent clogging and maintain air quality. The air mover, typically a blower or fan, requires periodic inspection to ensure it operates within optimal parameters. Additionally, checking for any signs of wear and tear on components like elbows and bends helps in identifying potential issues before they escalate. HeadPowder provides comprehensive maintenance services and spare parts support to their clients, ensuring that systems remain in top condition. By adhering to a regular maintenance schedule, businesses can extend the lifespan of their equipment, reduce downtime, and maintain consistent product quality.
Wheat flour pneumatic conveying systems have revolutionized the way bulk materials are handled in the food industry. By combining efficiency, hygiene, and flexibility, these systems offer a superior alternative to traditional mechanical methods. As the demand for high-quality wheat flour continues to grow, the importance of reliable and effective conveying systems becomes increasingly critical. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing innovative solutions that meet the evolving needs of the industry, ensuring that businesses can operate efficiently while maintaining the highest standards of product quality and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top