Rice husk ash, a byproduct of rice processing, is widely used in construction, agriculture, and other industries due to its unique properties. Efficient handling and transportation of this material are crucial for optimizing production processes and ensuring quality. The rice husk ash material handling equipment is specifically designed to address these needs, offering reliable solutions for various industrial applications.
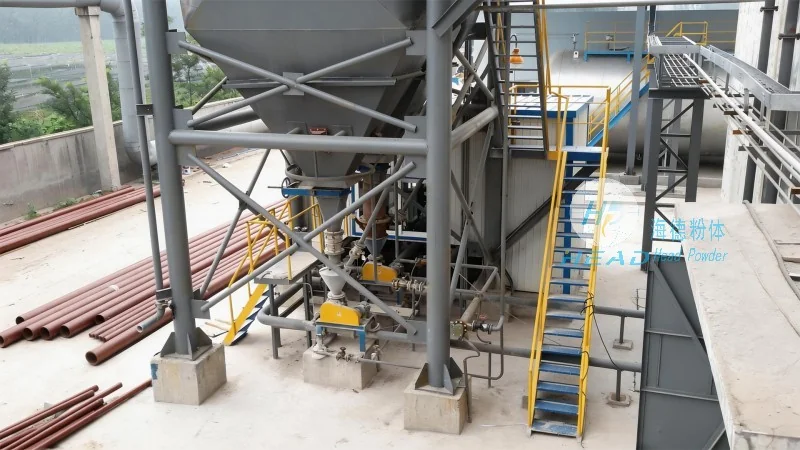
The design of rice husk ash material handling equipment is centered on several key principles to ensure efficiency, safety, and durability. These principles include material flow optimization, minimal dust generation, and ease of maintenance. The equipment typically consists of components such as feeders, conveyors, and storage systems, each tailored to handle the specific characteristics of rice husk ash. For instance, the feeders are designed to evenly distribute the material, preventing blockages and ensuring consistent flow. The conveyors, often using belt or screw mechanisms, are selected based on the material's density and abrasiveness. Additionally, the design incorporates dust control measures, such as sealed enclosures and filtration systems, to maintain a clean working environment and comply with environmental regulations.
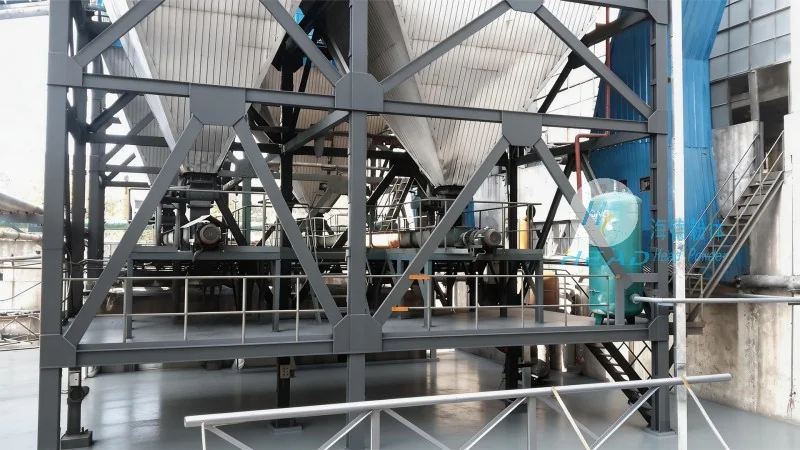
The operation of rice husk ash material handling equipment involves a systematic process that ensures smooth material transfer from the source to the destination. The process begins with the material being fed into the system, usually through a hopper or a loading hopper. The feeder then regulates the flow rate, controlling the amount of material that enters the conveyor. The conveyor transports the material to the storage or processing area, where it is either stored in silos or transferred to other equipment for further processing. The entire system is equipped with sensors and control mechanisms to monitor the flow rate, detect blockages, and adjust the operation as needed. This automation ensures that the equipment operates efficiently and safely, minimizing downtime and maximizing productivity.
Implementing rice husk ash material handling equipment offers numerous benefits for industrial operations. Firstly, it significantly improves the efficiency of material handling, reducing the time and labor required for transporting the material. The equipment's design minimizes material loss and contamination, ensuring that the quality of the rice husk ash is maintained throughout the process. Additionally, the dust control features help create a safer working environment, reducing the risk of respiratory issues and other health hazards associated with handling fine powders. The equipment's durability and low maintenance requirements also contribute to long-term cost savings, making it a cost-effective solution for industries that rely on rice husk ash. Furthermore, the equipment's adaptability allows it to be integrated into existing production lines, providing a seamless transition to more efficient material handling processes.
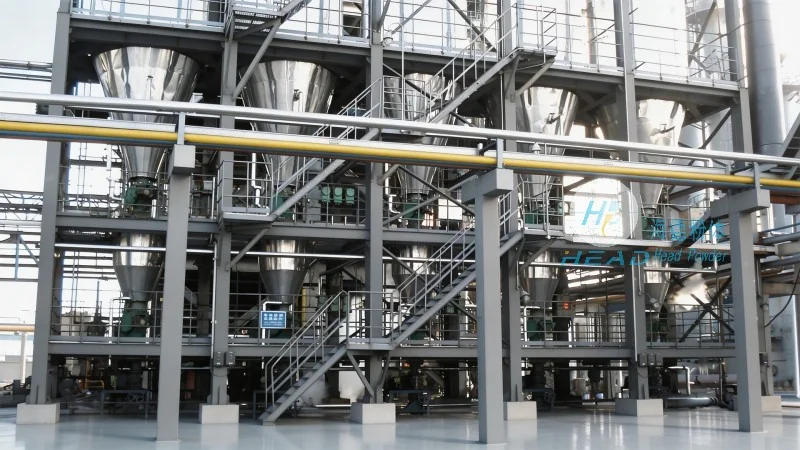
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of material handling equipment, specializing in solutions for various industrial applications. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for industries that require reliable and efficient material handling systems. The company's products, including rice husk ash material handling equipment, are designed to meet the specific needs of its clients, ensuring optimal performance and durability. HeadPowder's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering high-quality solutions that enhance operational efficiency and productivity. The company's headquarters is located in Shandong, China, where it continues to develop and manufacture advanced material handling equipment for global markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top