Dust-free automatic material handling conveyors are advanced industrial systems engineered to transport materials efficiently while maintaining a controlled, dust-free environment. These systems are crucial in industries where contamination control is paramount, such as pharmaceutical manufacturing, electronics assembly, and food processing. The primary goal of these conveyors is to ensure that materials are moved without introducing or spreading dust particles, which could compromise product quality or safety standards.
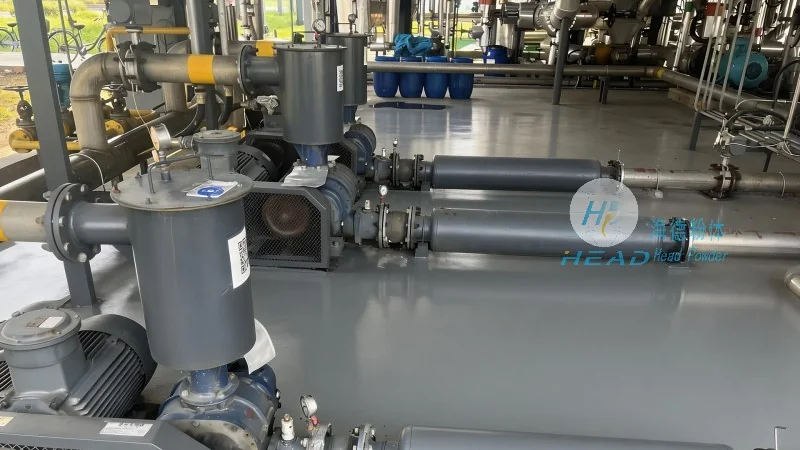
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design, development, and installation of dust-free material handling solutions. With headquarters located in Shandong, China, the company has established itself as a trusted partner for businesses seeking reliable and efficient conveyor systems that meet stringent cleanliness requirements. Their expertise lies in creating customized solutions tailored to the unique needs of each client, ensuring optimal performance and compliance with industry regulations.
The design of dust-free automatic material handling conveyors is built on several key principles aimed at minimizing dust generation and ensuring effective containment. One of the core design elements is the use of sealed and enclosed structures that prevent dust from escaping into the surrounding environment. These systems often incorporate features like dust filters, air filtration units, and negative pressure zones to maintain a clean air space within the conveyor. Additionally, the materials used for construction—such as stainless steel, aluminum, or specialized plastics—are selected for their non-porous and easy-to-clean properties, reducing the risk of dust accumulation.
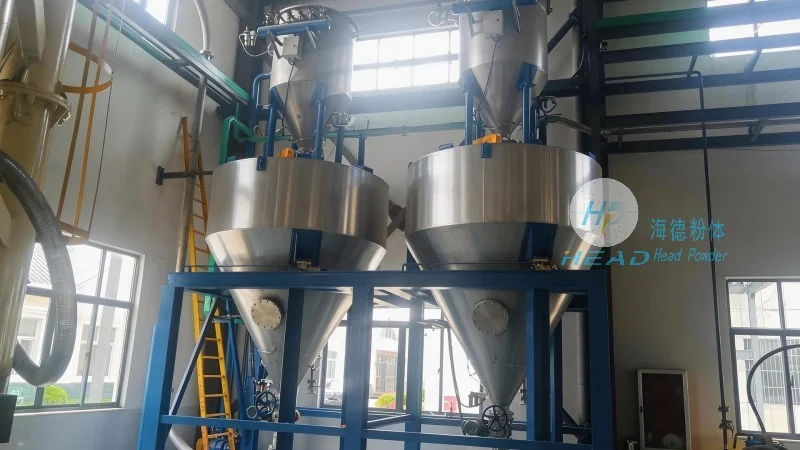
Modern dust-free automatic material handling conveyors typically consist of several integrated components that work in harmony to achieve efficient material transport. The primary components include conveyor belts or rollers, drive mechanisms, control systems, and dust containment enclosures. The conveyor belts are often made from materials like food-grade rubber or smooth plastic to prevent material adhesion and reduce friction, which can generate dust. Drive systems, usually electric motors with variable speed drives, allow for precise control over the conveyor speed, enabling smooth and consistent material movement. Control systems, often integrated with sensors and programmable logic controllers (PLCs), monitor the conveyor's operation and adjust parameters as needed to maintain optimal performance. Dust containment enclosures, designed with tight seals and access points for maintenance, ensure that any generated dust is captured and filtered before being released into the environment.
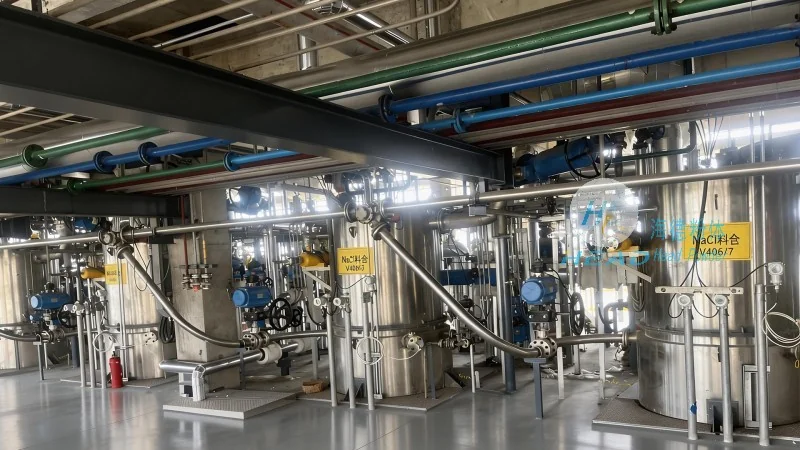
Dust-free automatic material handling conveyors offer numerous advantages that make them indispensable in industries where cleanliness is critical. These systems enhance product quality by preventing contamination from dust particles, which can affect the performance or safety of the final product. They also improve operational efficiency by automating material transport, reducing manual handling and associated errors. Furthermore, these conveyors contribute to a safer working environment by minimizing dust exposure for employees, aligning with occupational health and safety regulations. The applications of dust-free conveyors span a wide range of industries, including pharmaceuticals, where they are used to transport raw materials and finished products without compromising sterility; electronics manufacturing, where they handle sensitive components; and food processing, where they ensure that products remain free from contaminants throughout the production process.
In summary, dust-free automatic material handling conveyors represent a sophisticated solution for industries requiring high levels of cleanliness and efficiency in material transport. The design principles, components, and functionalities of these systems are carefully engineered to meet stringent contamination control standards. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing customized solutions that address the unique challenges of each industry, ensuring that businesses can maintain product quality, operational efficiency, and compliance with regulatory requirements. As technology continues to advance, these conveyors will likely evolve to incorporate even more advanced features, further enhancing their role in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top