When it comes to the efficient and safe transportation of potassium sulfate, specialized conveyor systems play a crucial role in industrial processes. These systems are engineered to handle the unique properties of potassium sulfate, ensuring optimal performance and reliability in various applications. Understanding the components and design principles of such conveyors is essential for industries that rely on consistent material flow and quality control.
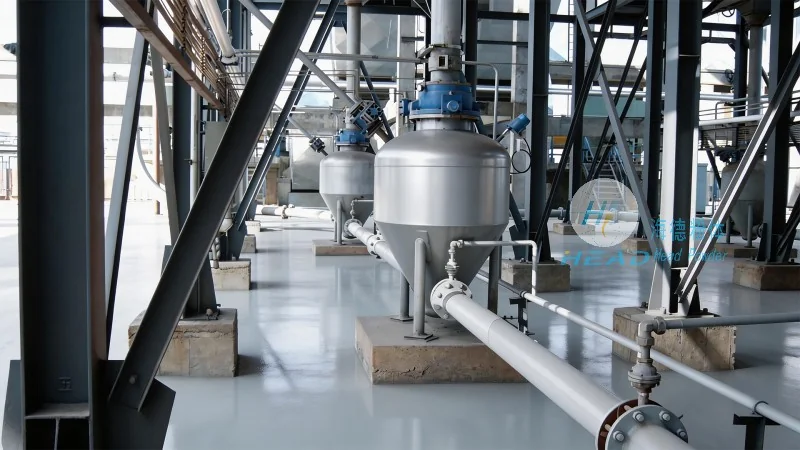
At Shandong HeadPowder Engineering Co., Ltd., we specialize in designing and manufacturing advanced material handling equipment tailored to the specific needs of our clients. With a focus on innovation and precision engineering, our team of experts develops conveyors that meet the highest standards of performance and durability. Our company, based in Shandong, China, has built a reputation for delivering reliable and efficient solutions for a wide range of industrial applications.
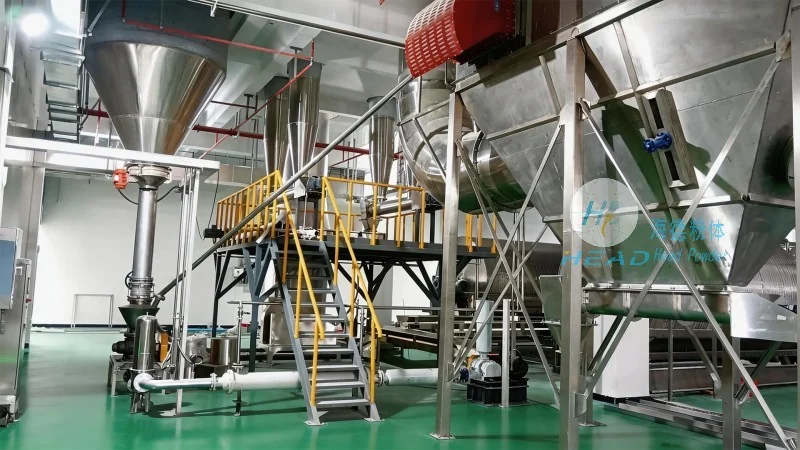
The core components of a potassium sulfate material handling conveyor include the conveyor belt, drive system, idlers, and supporting structures. The conveyor belt is typically made from materials resistant to chemical corrosion and abrasion, ensuring it can withstand the handling of potassium sulfate without degradation. The drive system, which may consist of electric motors and gearboxes, provides the necessary power to move the material along the conveyor path. Idlers are strategically placed to support the belt and maintain proper alignment, while the supporting structures provide stability and durability. These components work in harmony to ensure smooth and continuous material transport.
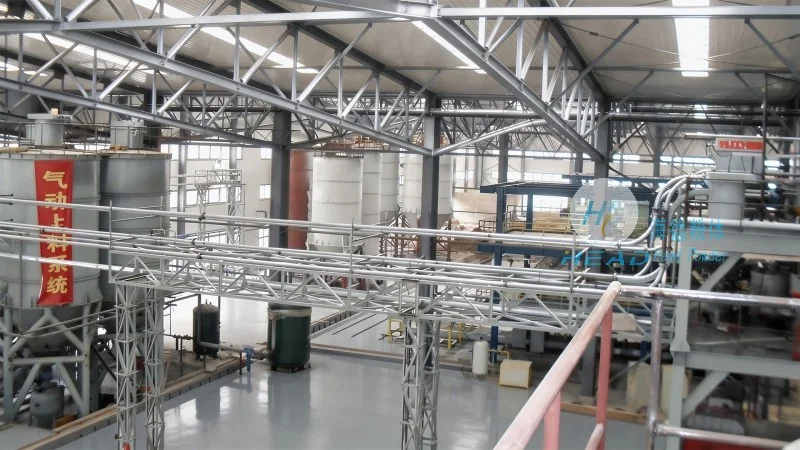
The design of a potassium sulfate material handling conveyor is based on several key principles to ensure efficiency and safety. First, the system must be designed to handle the specific physical properties of potassium sulfate, such as its particle size, density, and flow characteristics. This involves selecting appropriate belt materials and conveyor speeds to prevent material buildup or spillage. Second, the conveyor must be constructed with corrosion-resistant materials to withstand the chemical properties of potassium sulfate, which can be aggressive to certain metals. Third, the system should incorporate safety features, such as emergency stop mechanisms and protective guards, to protect operators and prevent accidents. Finally, the design should prioritize energy efficiency and low maintenance requirements to reduce operational costs over time.
Potassium sulfate material handling conveyors are widely used in various industries, including agriculture, chemical manufacturing, and food processing. In agriculture, these systems are used to transport potassium sulfate fertilizer to storage facilities or distribution centers, ensuring timely and efficient delivery to farms. In chemical manufacturing, they help move raw materials and finished products through production lines, improving overall process efficiency. The benefits of using such conveyors include increased productivity, reduced labor costs, and improved safety for workers. By automating the material handling process, industries can achieve higher throughput and better control over their operations.
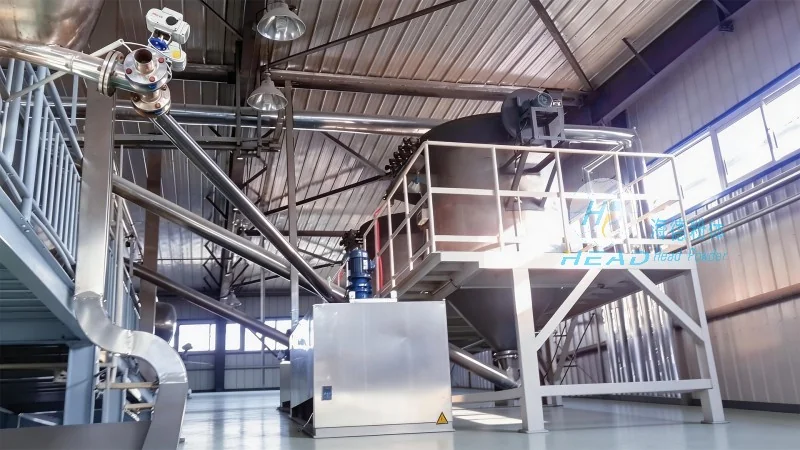
At HeadPowder, we understand that each client has unique requirements, which is why we offer customized conveyor solutions tailored to specific applications. Our team works closely with clients to understand their operational needs and design conveyors that meet their exact specifications. Additionally, we provide comprehensive maintenance services to ensure the longevity and reliability of our equipment. Regular maintenance, including belt tension checks, idler replacement, and lubrication, helps prevent breakdowns and extends the lifespan of the conveyor system. By investing in proper maintenance, clients can maximize the return on their investment and minimize downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top