Quartz stone material handling equipment is a specialized type of machinery designed to transport and process quartz stone materials efficiently and safely. These devices are crucial in various industrial applications, particularly in the manufacturing and processing sectors where quartz stone is used as a raw material. Understanding the design principles behind these equipment is essential for optimizing production processes and ensuring operational efficiency.
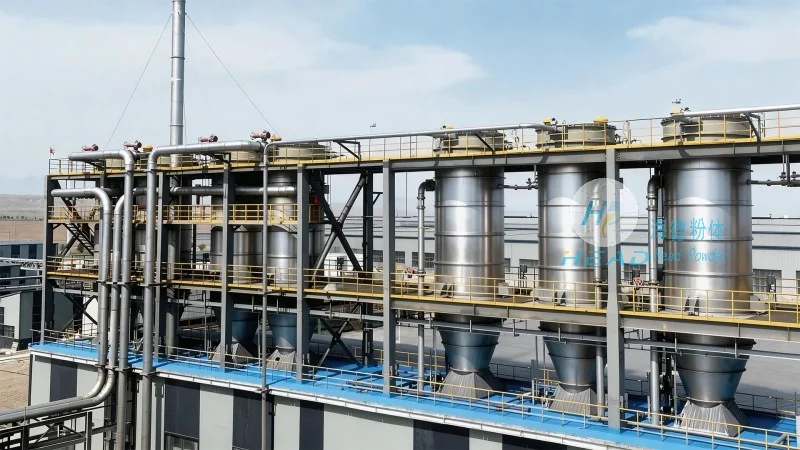
Quartz stone, known for its hardness, durability, and chemical resistance, is widely used in the production of countertops, tiles, and other construction materials. The handling of such materials requires specialized equipment capable of managing their weight, size, and abrasive properties. Quartz stone material handling equipment includes a range of devices such as conveyors, elevators, and feeders, each designed to address specific material handling challenges. The primary goal of these systems is to move quartz stone from one location to another within a production facility with minimal human intervention and maximum safety.
The design of quartz stone material handling equipment is guided by several key principles aimed at ensuring reliability, efficiency, and durability. One of the fundamental principles is the use of robust construction materials that can withstand the abrasive nature of quartz stone. Components such as belts, rollers, and frames are typically made from high-strength metals or composite materials to prevent wear and tear. Additionally, the equipment is designed with a focus on minimizing friction and heat generation, as excessive friction can damage the quartz stone and reduce the lifespan of the machinery.
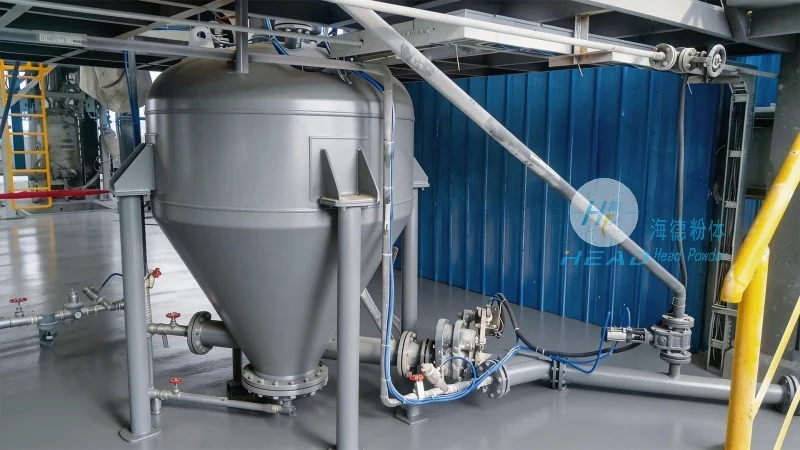
Another critical design principle is the integration of advanced control systems. Modern quartz stone material handling equipment often incorporates programmable logic controllers (PLCs) and sensors that monitor the flow of materials and adjust the operation of the equipment in real-time. This automation not only improves efficiency but also enhances safety by preventing overloading or blockages. The control systems may also include features like overload protection and emergency stop mechanisms to ensure that the equipment operates within safe parameters at all times.
Quartz stone material handling equipment typically consists of several key components, each playing a vital role in the overall operation. The conveyor system, which may be a belt conveyor or a screw conveyor, is responsible for transporting the quartz stone along the desired path. The belt conveyor uses a continuous belt to move materials, while the screw conveyor employs a rotating screw to push materials forward. Both systems are designed to handle the high density and weight of quartz stone, with heavy-duty bearings and drive mechanisms to support the load.
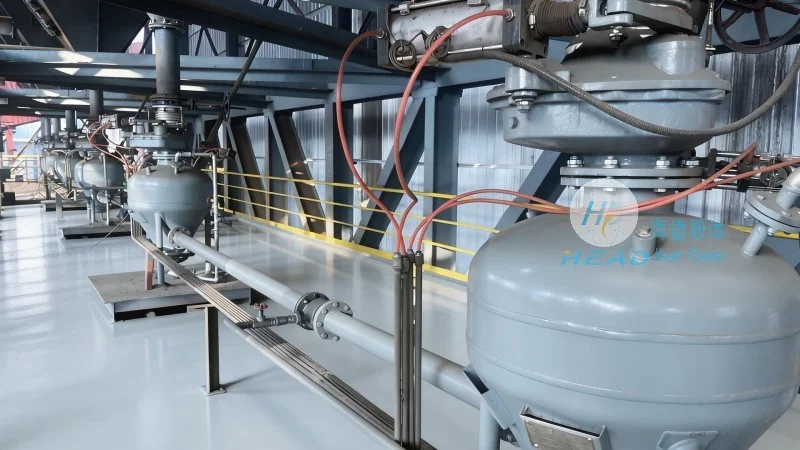
The elevator or vertical conveyor is another essential component, especially when materials need to be moved between different levels of a facility. These systems use a series of buckets or a belt to lift the quartz stone vertically, often with a chain or belt drive. The design of the elevator is critical to ensure smooth vertical movement and to prevent material spillage or blockage. The feeders, which are often integrated with the conveyor system, are responsible for controlling the flow rate of the quartz stone, ensuring a consistent and controlled supply to downstream processing equipment.
Quartz stone material handling equipment is used in a variety of industrial settings, including stone processing plants, construction material manufacturing facilities, and mining operations. The equipment is designed to handle different sizes of quartz stone, from small granules to large slabs. The operational considerations for these systems include maintaining proper alignment of components, regular lubrication of moving parts, and periodic inspection of wear parts to ensure optimal performance. Proper maintenance is crucial to prevent downtime and to extend the lifespan of the equipment.
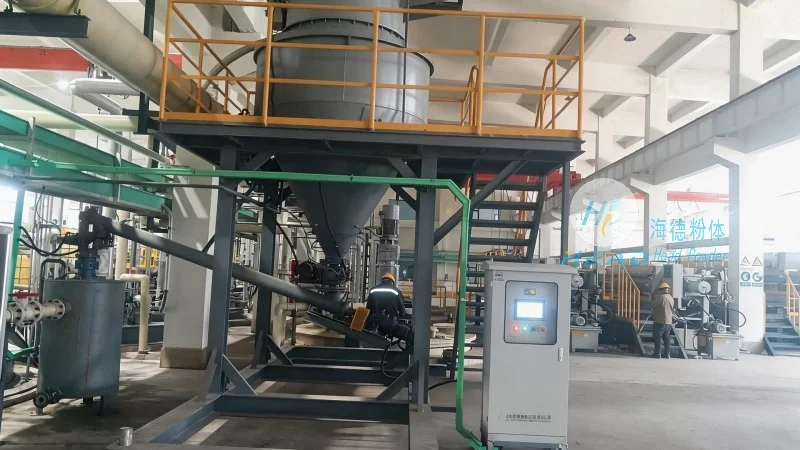
In addition to the technical aspects, the design of quartz stone material handling equipment also considers ergonomic and safety factors. The equipment is often designed with enclosed structures to contain dust and debris, reducing the risk of inhalation and other health hazards. Safety features such as guardrails, emergency stop buttons, and interlocked doors are standard to protect operators from potential accidents. The equipment is also designed to be easily accessible for maintenance, with removable panels and clear labeling of components.
Quartz stone material handling equipment is a sophisticated system that combines robust engineering with advanced control technology to efficiently transport and process quartz stone materials. The design principles behind these equipment focus on durability, efficiency, and safety, ensuring that they can handle the demanding requirements of industrial applications. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and producing high-quality quartz stone material handling equipment tailored to the specific needs of various industries. With a commitment to quality and innovation, HeadPowder provides reliable solutions that enhance productivity and operational safety in the handling of quartz stone materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top