Limestone, a fundamental raw material in the production of cement, steel, and various chemical products, requires efficient and reliable handling equipment to ensure smooth industrial processes. The proper design and operation of limestone material handling equipment are crucial for optimizing material flow, reducing downtime, and enhancing overall production efficiency. This article explores the key aspects of limestone material handling equipment, focusing on their design principles and the technology behind them.
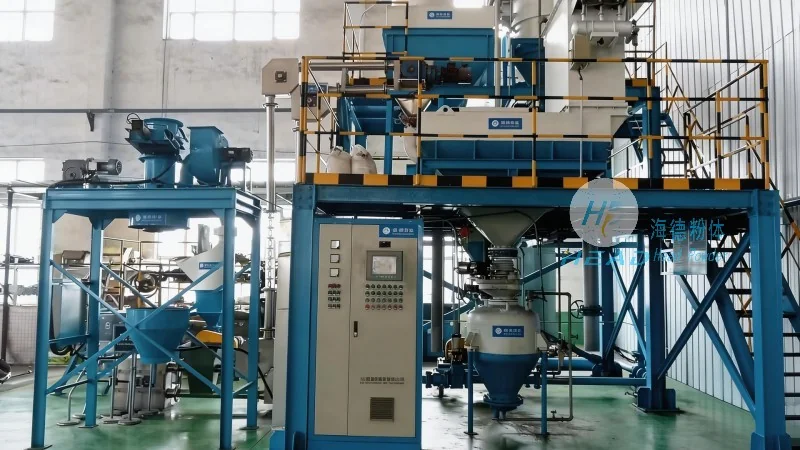
Limestone material handling equipment is specifically engineered to transport, store, and process limestone, which is often in bulk form. These systems are designed to handle the unique characteristics of limestone, such as its size, density, and potential for dust generation. The equipment must be robust, durable, and capable of withstanding the abrasive nature of limestone particles to ensure long-term performance. HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced limestone material handling solutions tailored to meet the diverse needs of industrial clients.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable company dedicated to providing high-quality limestone material handling equipment. With years of experience in the industry, HeadPowder has established itself as a reliable supplier, offering customized solutions that enhance operational efficiency and safety. The company's commitment to innovation and customer satisfaction has made it a preferred choice for businesses seeking dependable limestone handling systems.
The design of limestone material handling equipment is guided by several key principles to ensure optimal performance and longevity. First, the equipment must be constructed from materials that can withstand the abrasive and corrosive effects of limestone. High-quality steel, stainless steel, and specialized coatings are commonly used to protect components from wear and tear. Second, the system is designed to handle the bulk nature of limestone, often using mechanisms like belt conveyors, screw conveyors, or pneumatic systems. Belt conveyors are widely used for horizontal and inclined transport due to their simplicity and efficiency. Screw conveyors are suitable for vertical or horizontal transport in confined spaces, while pneumatic systems are ideal for transporting fine limestone powders over long distances with minimal dust.
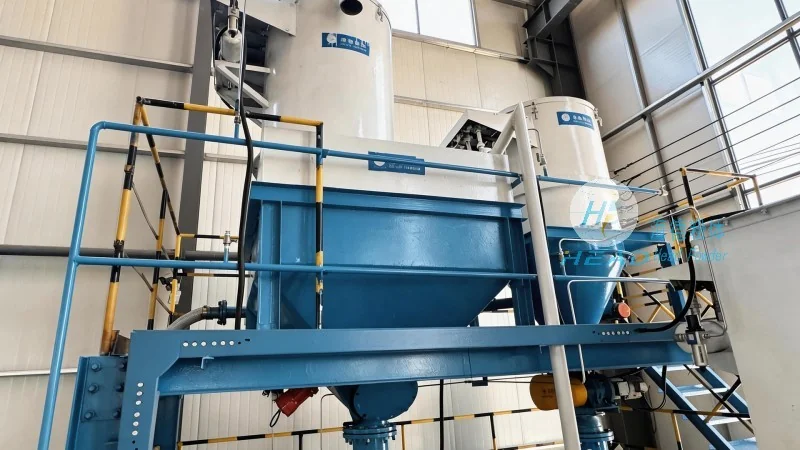
Third, the design incorporates features to manage dust and prevent material buildup. Dust collection systems and anti-static measures are integrated to maintain a safe working environment and comply with environmental regulations. Additionally, the equipment is engineered for easy maintenance and cleaning, as limestone can adhere to surfaces and cause blockages if not properly managed. The use of wear-resistant liners and adjustable components allows for quick adjustments and repairs, minimizing downtime and operational costs.
Limestone material handling equipment typically consists of several key components, each playing a critical role in the overall system. The feed hopper is the first component, designed to receive and store limestone from a source like a quarry or storage silo. It is equipped with a discharge valve to control the flow of material into the conveyor system. The conveyor itself, whether a belt or screw, is responsible for transporting the limestone from the hopper to the processing or storage area. The drive system, usually powered by electric motors, provides the necessary force to move the material along the conveyor path. A control panel is included to monitor and adjust the speed and direction of the conveyor, ensuring precise material handling.
For pneumatic systems, the equipment includes a blower or compressor to generate the air pressure needed to transport limestone particles. The air ducts and pipelines are designed to minimize pressure loss and ensure consistent material flow. The system also features dust filters and collection units to capture and remove airborne particles, preventing contamination and maintaining air quality. In some cases, the equipment may include a screening or crushing unit to process limestone into smaller, more manageable sizes before transport.
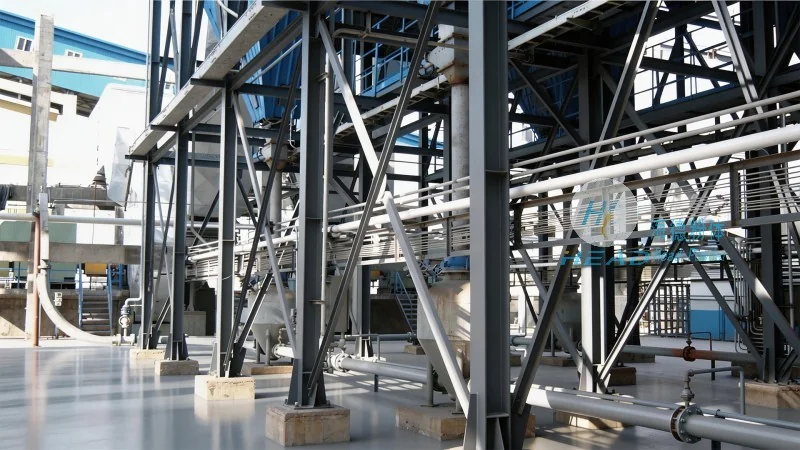
Limestone material handling equipment is widely used in various industries, with the most common applications being in the cement and chemical sectors. In cement production, limestone is a primary raw material that is ground and mixed with other components to form clinker. The equipment ensures that limestone is transported efficiently from storage to the grinding mills, where it is processed into cement. In the chemical industry, limestone is used in the production of calcium compounds, and the handling equipment ensures that the material is delivered to reactors and processing units without loss or contamination.
Other applications include the steel industry, where limestone is used as a flux to remove impurities from iron ore, and the agricultural sector, where limestone is used as a soil amendment. The versatility of limestone material handling equipment makes it suitable for a wide range of industrial processes, providing reliable and efficient material transport solutions.
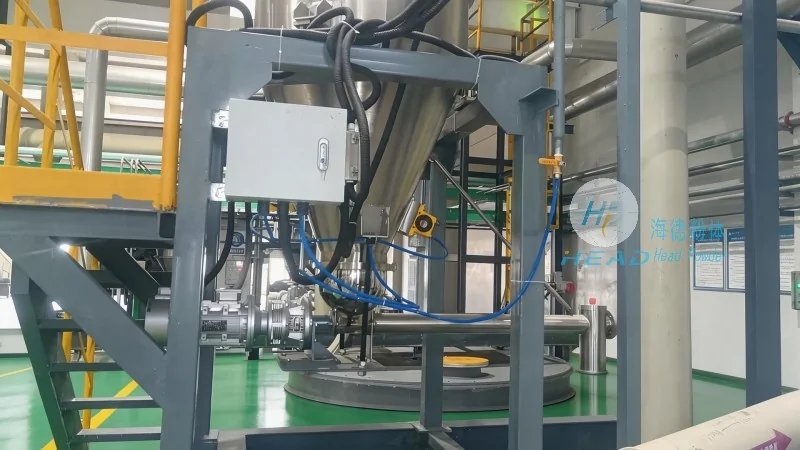
Investing in high-quality limestone material handling equipment offers numerous advantages for industrial operations. First, it improves material flow efficiency, reducing the time and labor required to transport limestone from one location to another. This leads to increased production rates and reduced operational costs. Second, the equipment is designed to minimize dust and noise, creating a safer and more comfortable working environment for employees. Third, the use of durable materials and advanced design reduces maintenance needs and extends the equipment's lifespan, providing long-term value.
Additionally, the equipment can be customized to meet specific operational requirements, such as handling different limestone sizes or processing capacities. This flexibility allows businesses to adapt their material handling systems to changing production needs without significant investment. The integration of automation and control systems further enhances operational efficiency, allowing for real-time monitoring and adjustment of the equipment's performance.
Limestone material handling equipment is a critical component of modern industrial operations, ensuring the efficient and safe transport of this essential raw material. The design principles and technology behind these systems are continuously evolving to meet the demands of various industries. Companies like HeadPowder Engineering Co., Ltd. play a vital role in developing and providing advanced limestone handling solutions that enhance productivity and sustainability. By understanding the key design principles and applications of limestone material handling equipment, businesses can make informed decisions to optimize their material handling processes and achieve long-term success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top