HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems for various industrial applications. This article provides a detailed overview of the operation process and working principle of a sand powder pneumatic conveying system, highlighting the key components, operational steps, and technical aspects that ensure efficient and reliable material handling.
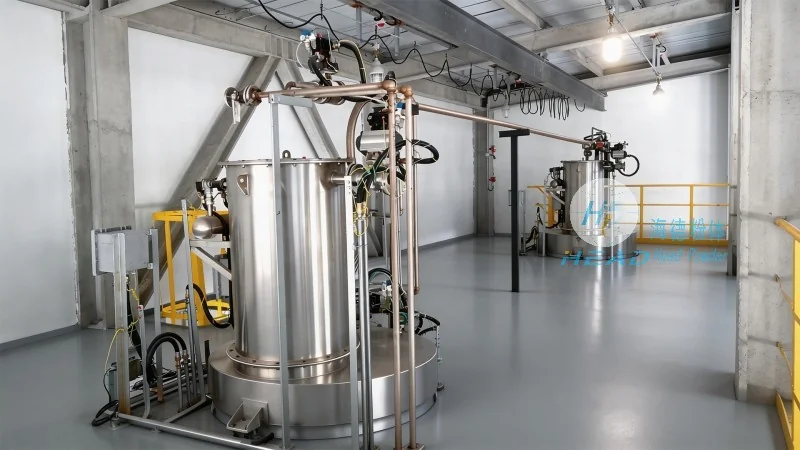
Pneumatic conveying systems are widely used in industries such as mining, construction, and manufacturing to transport bulk materials like sand, powders, and granules over short to medium distances. These systems utilize compressed air or gas to move materials through a pipeline network, eliminating the need for mechanical components like belts or buckets. The efficiency and flexibility of pneumatic conveying make it an ideal solution for handling abrasive and dusty materials, as seen in the case of sand powder transport.
The core components of a sand powder pneumatic conveying system include the material hopper, air compressor, conveyor pipeline, dust filter, and control system. Each component plays a critical role in the overall operation and performance of the system.
1. Material Hopper: The hopper is the storage container where the sand powder is loaded before being conveyed. It is designed with a sloped bottom to facilitate the smooth discharge of material into the conveyor pipeline. The hopper may also include a feeder mechanism, such as a rotary valve or a screw feeder, to regulate the flow of material into the system.
2. Air Compressor: The air compressor generates the necessary pressure and flow of air to move the sand powder through the pipeline. It is typically a positive displacement type, such as a rotary screw or reciprocating compressor, capable of delivering high-pressure air at a consistent flow rate. The compressor is equipped with a pressure regulator to maintain stable operating conditions.
3. Conveyor Pipeline: The pipeline is the main transport channel for the sand powder and air mixture. It is constructed from durable materials like stainless steel or PVC to withstand the abrasive nature of sand and prevent leakage. The pipeline is designed with appropriate bends and elbows to guide the material flow while minimizing pressure drop and material deposition.
4. Dust Filter: The dust filter is essential for capturing and removing fine particles from the exhaust air, ensuring compliance with environmental regulations and maintaining air quality. It typically consists of a baghouse or cartridge filter that traps dust particles before releasing clean air back into the environment.
5. Control System: The control system monitors and regulates the operation of the entire system, including the air compressor, feeder, and filter. It uses sensors to detect pressure, flow, and material levels, and adjusts the system parameters to optimize performance and prevent equipment damage.
The operation of a sand powder pneumatic conveying system involves several sequential steps to ensure the efficient transport of material from the hopper to the discharge point.
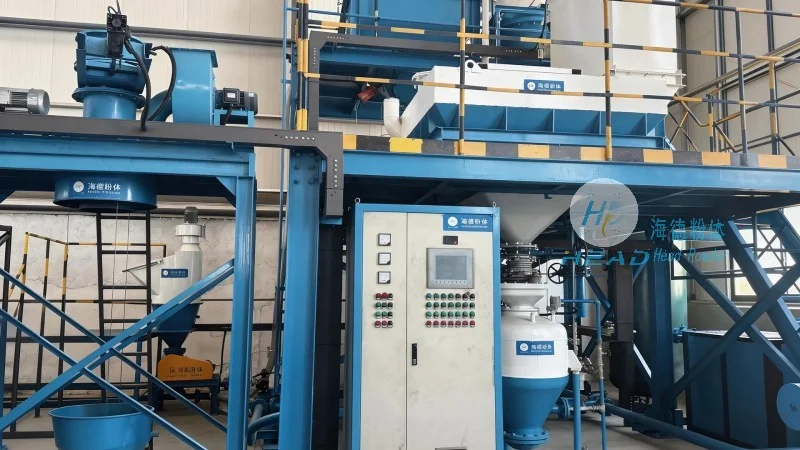
Step 1: Material Loading - Sand powder is loaded into the material hopper from a bulk storage silo or direct from a production line. The hopper is designed to hold a sufficient quantity of material to avoid frequent refilling, which can interrupt the conveying process.
Step 2: Feeder Activation - The feeder mechanism (e.g., rotary valve or screw feeder) is activated to control the flow rate of sand powder from the hopper into the conveyor pipeline. The feeder is synchronized with the air compressor to maintain a consistent material-air ratio, preventing clogging or excessive pressure buildup.
Step 3: Air Compression and Injection - The air compressor starts and delivers high-pressure air into the pipeline. The air is injected at a specific point (usually near the hopper) to create a flow of air that entrains the sand powder particles. The air velocity is carefully controlled to ensure that the particles are fully suspended and transported without settling.
Step 4: Material Transport - The sand powder particles are carried by the air stream through the pipeline, following the path defined by the pipeline layout. The system may include multiple pipeline segments, bends, and branches to direct the material to the desired discharge location, such as a storage silo or processing unit.
Step 5: Discharge and Material Separation - At the discharge point, the air and sand powder mixture enters a separator or cyclone, where the air is separated from the material. The sand powder is collected in a receiving hopper or container, while the air is directed to the dust filter for purification.
Step 6: Exhaust Air Treatment - The filtered air is released back into the environment, while the collected dust is disposed of according to local regulations. The control system continuously monitors the filter performance and alerts operators if maintenance is required.
The working principle of a sand powder pneumatic conveying system is based on the principle of fluidization and suspension of solid particles by a moving gas stream. When compressed air is introduced into the pipeline, it creates a high-velocity flow that overcomes the gravitational force acting on the sand particles, causing them to become suspended in the air stream. This suspension allows the particles to be transported through the pipeline as a homogeneous mixture, known as a "pneumatic slurry."
The key to efficient operation is maintaining the correct air-to-material ratio. If the air velocity is too low, the sand particles may settle and cause blockages in the pipeline. Conversely, if the air velocity is too high, excessive energy consumption occurs, and the system may become inefficient. The control system plays a crucial role in adjusting the air flow and material feed rate to achieve the optimal ratio.
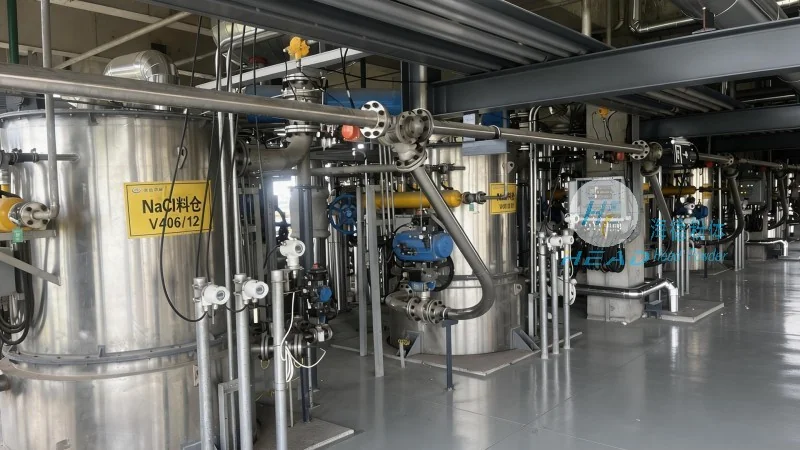
Another important aspect of the working principle is the pressure drop along the pipeline. As the air and sand mixture travels through the pipeline, friction between the particles and the pipe walls causes a gradual increase in pressure. The system design must account for this pressure drop to ensure that the air compressor can maintain sufficient pressure to overcome the resistance and deliver the material to the discharge point.
Implementing a sand powder pneumatic conveying system offers several advantages over traditional mechanical conveying methods. These include:
1. Reduced Maintenance: Unlike belt or bucket elevators, pneumatic systems have fewer moving parts, reducing the risk of mechanical failure and lowering maintenance costs.
2. Improved Safety: The enclosed pipeline design prevents dust exposure and reduces the risk of material spillage, enhancing workplace safety.
3. Flexibility in Layout: Pneumatic systems can be easily reconfigured to accommodate changes in production processes or facility layout, as the pipeline can be installed in various orientations and configurations.
4. Energy Efficiency: Modern air compressors and control systems are designed to optimize energy usage, reducing operational costs compared to traditional conveying methods.
5. Environmental Compliance: The dust filter ensures that the exhaust air meets environmental standards, minimizing the impact on the surrounding environment.
HeadPowder's sand powder pneumatic conveying systems are engineered to provide reliable and efficient material handling solutions for industries dealing with sand and other fine powders. By understanding the operation process and working principle of these systems, users can optimize their performance, reduce operational costs, and ensure compliance with environmental regulations. With a focus on quality and innovation, HeadPowder continues to deliver advanced pneumatic conveying solutions that meet the evolving needs of modern industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top