HeadPowder, a prominent engineering company headquartered in Shandong, China, is dedicated to providing advanced solutions for powder handling through its small bag powder pneumatic conveying systems. These systems are engineered to efficiently transport bulk powders using compressed air, offering a reliable and flexible method for material transfer in various industrial settings. The technology is particularly valuable for applications where traditional mechanical conveying methods may be impractical or inefficient, such as handling fine, cohesive, or sensitive powders.
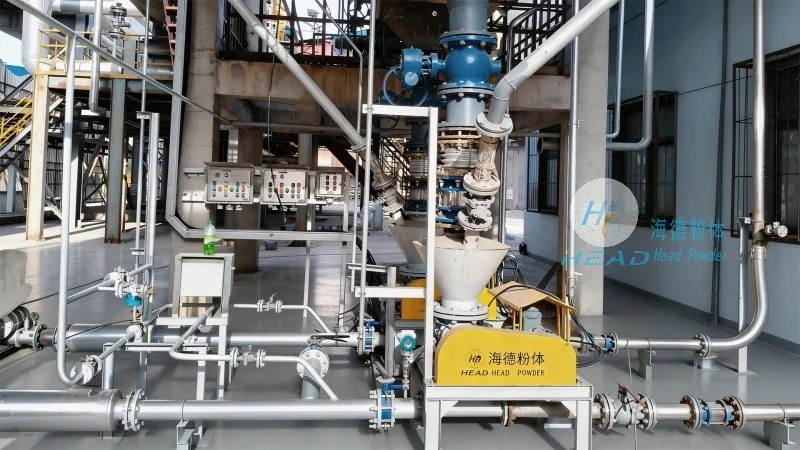
The small bag powder pneumatic conveying system comprises several essential components, each playing a critical role in the overall operation. The primary components include a storage hopper or silo, a feeder (typically a rotary valve or screw feeder), a conveying pipeline, a filter system, and a control panel. The storage hopper is designed to hold the bulk powder and may feature a discharge port for easy loading. The feeder regulates the powder flow into the conveying line, ensuring a consistent and controlled rate of material transfer. The conveying pipeline, usually constructed from stainless steel or other corrosion-resistant materials, transports the powder and air mixture. The filter system, often a combination of a bag filter and a cyclone separator, captures any escaped powder particles, maintaining air cleanliness and preventing environmental contamination. The control panel allows operators to monitor and adjust system parameters, such as air pressure, flow rate, and powder feed rate, ensuring optimal performance.
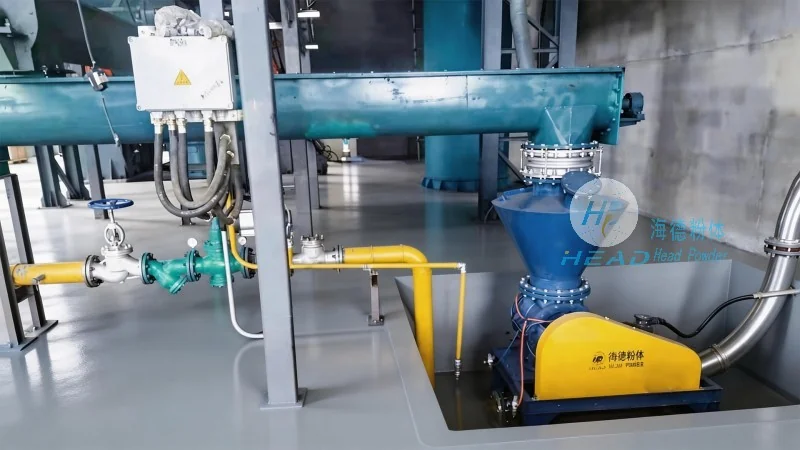
The operation of the small bag powder pneumatic conveying system follows a systematic process to ensure efficient and safe material transfer. The process begins with the loading of the powder into the storage hopper. Once the hopper is filled, the rotary valve or screw feeder is activated to control the powder flow into the conveying line. Simultaneously, the compressed air system is started, providing the necessary pressure to move the powder. The air and powder mixture travels through the pipeline, with the powder suspended in the air stream. The system's pressure and flow rate are monitored using pressure gauges and flow meters, ensuring that the conveying process is stable and efficient. At the destination point, the powder is discharged into the processing equipment, such as a mixer or reactor. The filter system at the end of the line captures any fine particles that may have escaped, returning them to the hopper for reuse. The entire process is automated, reducing the need for manual intervention and minimizing the risk of dust exposure.
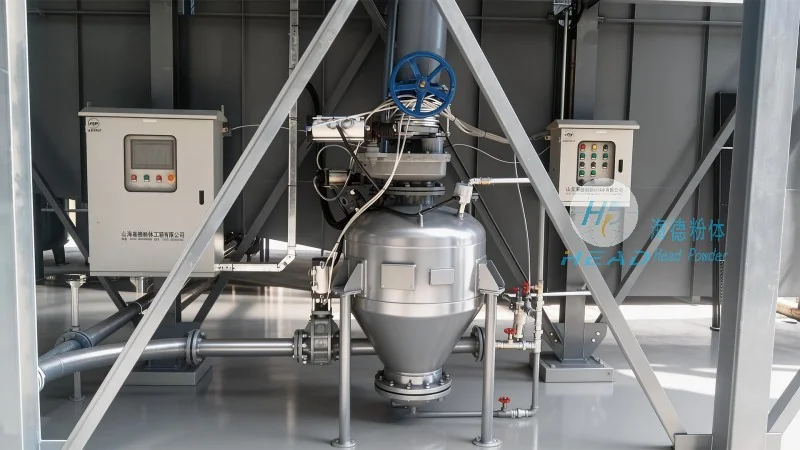
The working principle of the small bag powder pneumatic conveying system is based on the fundamental concept of using compressed air to transport powder particles. This process can be classified into two main categories: dilute phase and dense phase conveying. Dilute phase conveying involves transporting the powder at a relatively low concentration, where the powder particles are suspended in the air stream at high velocity. This method is suitable for short to medium-distance transfers and is commonly used for fine powders. Dense phase conveying, on the other hand, uses higher air pressure and lower velocity to move the powder in a more compact form, often referred to as a "plug flow." This mode is ideal for handling sensitive or abrasive powders, as it minimizes particle degradation and reduces the risk of clogging. The system's design allows for the selection of either mode based on the specific characteristics of the powder, such as particle size, density, and flowability.
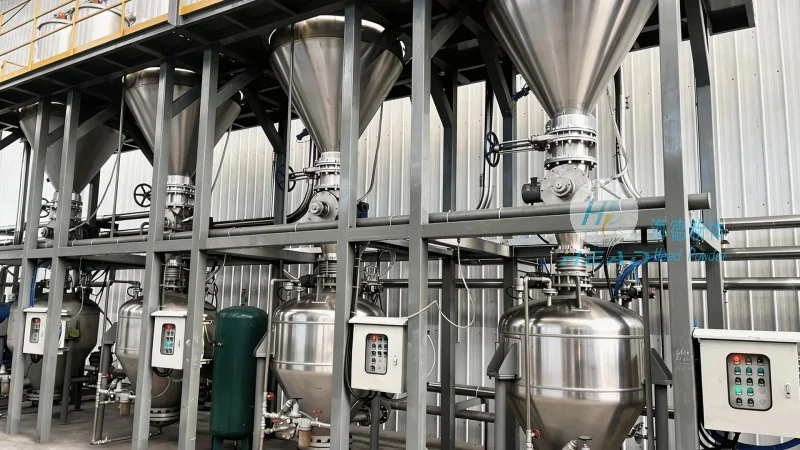
Small bag powder pneumatic conveying systems offer numerous advantages over traditional mechanical conveying methods. These benefits include improved safety by eliminating manual handling of powders, reduced labor costs due to automation, and enhanced process control through precise flow regulation. The systems are particularly advantageous for industries that require high hygiene standards, such as pharmaceuticals and food processing, where dust and contamination must be minimized. In the chemical industry, the systems are used to transport reactive or corrosive powders, leveraging the corrosion-resistant materials used in the pipeline and components. The plastics industry benefits from the ability to handle abrasive powders without damaging equipment, while the agricultural sector utilizes these systems for fertilizer and feed distribution. The flexibility of the system allows for customization to meet the specific needs of each application, ensuring optimal performance and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top