When it comes to air conveying systems for wet ammonium nitrate, the choice between positive pressure and negative pressure systems is a critical decision that impacts operational efficiency, safety, and equipment longevity. Understanding the fundamental differences between these two approaches is essential for selecting the most suitable solution for your specific application. This article will explore the key factors that influence the choice of positive pressure versus negative pressure for air conveying wet ammonium nitrate, providing a clear guide to help you make an informed decision.
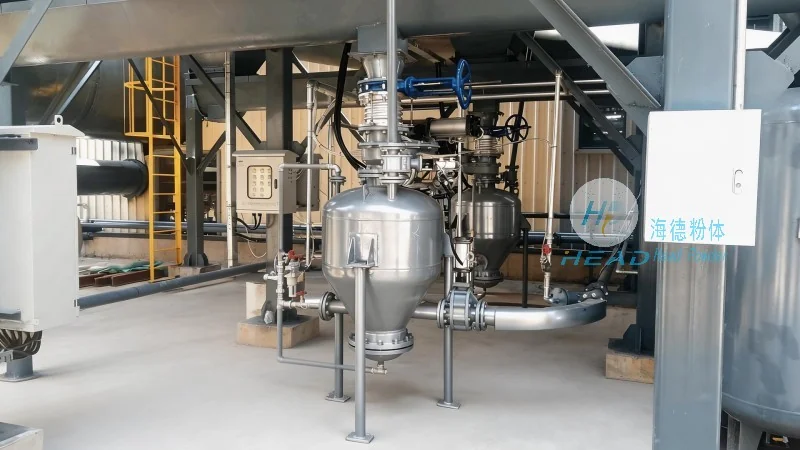
Wet ammonium nitrate is a common material in the fertilizer and chemical industries, often requiring efficient and safe material handling. Air conveying is a widely used method for transporting such bulk materials, offering advantages such as reduced mechanical wear, lower maintenance costs, and the ability to handle materials in a dust-free environment. However, the nature of wet ammonium nitrate—its moisture content, particle size, and potential for caking—makes the selection of the right air conveying system crucial. Positive pressure and negative pressure systems are the two primary types of air conveying, each with distinct characteristics and applications.
Positive pressure air conveying systems operate by blowing air into the material to be conveyed, creating a positive pressure within the system. This method is often referred to as "blowing" or "pressure-fed" conveying. In this system, the material is drawn into the conveying line by the moving air, which is typically generated by a positive displacement blower or a centrifugal fan. The positive pressure ensures that the material is continuously moved through the system, preventing backflow and ensuring consistent flow rates. For wet ammonium nitrate, positive pressure systems are particularly effective when dealing with materials that have a tendency to clog or when high conveying distances are required. The high pressure generated by the blower helps to break up agglomerates and maintain a smooth flow of material.
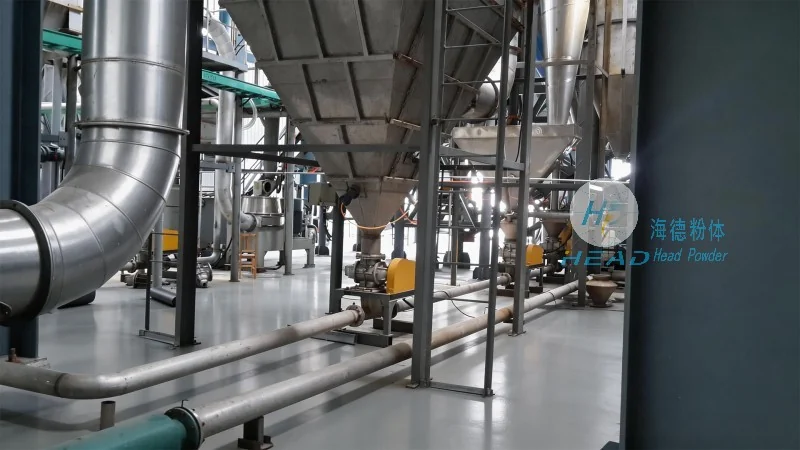
Positive pressure air conveying offers several advantages when handling wet ammonium nitrate. Firstly, it provides excellent control over the material flow, allowing for precise regulation of conveying rates. This is particularly important when dealing with moisture-sensitive materials, as it helps to prevent over-drying or under-drying during the conveying process. Secondly, positive pressure systems are generally more suitable for long-distance conveying, as the high pressure can maintain the material's velocity over extended distances without significant loss of efficiency. Thirdly, these systems are often more resistant to clogging, as the high air velocity helps to keep the material moving and prevent the buildup of deposits in the conveying lines. Additionally, positive pressure systems are typically easier to clean and maintain, as the air flow can be directed to clear any blockages or deposits in the system.
Negative pressure air conveying systems, on the other hand, operate by creating a vacuum or negative pressure within the system. This method is often referred to as "suction" or "vacuum-fed" conveying. In this system, the material is drawn into the conveying line by the suction created by a vacuum pump or a fan operating in reverse. The negative pressure pulls the material from the source, such as a hopper or a storage bin, and moves it through the system. For wet ammonium nitrate, negative pressure systems are commonly used for short to medium conveying distances and for materials that are less prone to clogging. The lower air velocity and pressure in negative pressure systems make them more suitable for handling materials with lower moisture content or when the conveying distance is relatively short.
Negative pressure air conveying also offers distinct advantages for wet ammonium nitrate applications. One of the primary benefits is the lower energy consumption compared to positive pressure systems, as the suction process requires less power to maintain the system's pressure. This can result in significant cost savings over the long term, especially for large-scale operations. Secondly, negative pressure systems are often more suitable for handling materials that are less abrasive or have a lower risk of clogging, as the lower air velocity reduces the likelihood of material buildup in the conveying lines. Thirdly, these systems are generally quieter and less disruptive to the surrounding environment, making them a good choice for applications where noise levels need to be minimized. Additionally, negative pressure systems are easier to install and integrate into existing facilities, as they do not require the same level of pressure containment as positive pressure systems.
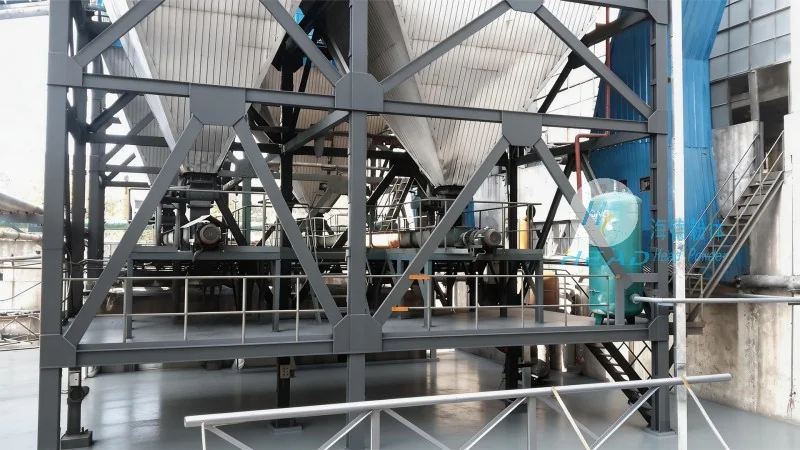
So, how can you distinguish between positive and negative pressure air conveying systems when selecting the right solution for your wet ammonium nitrate application? The key factors to consider include the conveying distance, the material's properties (such as moisture content, particle size, and tendency to clog), and the required flow rate. For long-distance conveying or materials with high moisture content and a tendency to clog, positive pressure systems are generally preferred due to their higher air velocity and pressure, which help to maintain consistent flow and prevent blockages. Conversely, for short to medium distances and materials with lower moisture content or lower clogging risk, negative pressure systems may be more suitable due to their lower energy consumption and easier installation. Another important factor is the system's compatibility with the existing infrastructure. Positive pressure systems may require additional containment measures to prevent air leakage, while negative pressure systems may need to be equipped with proper exhaust and filtration systems to ensure environmental compliance.
Choosing between positive pressure and negative pressure air conveying for wet ammonium nitrate requires a careful evaluation of the specific requirements of your application. Positive pressure systems offer superior control, longer conveying distances, and better resistance to clogging, making them ideal for challenging applications. Negative pressure systems, on the other hand, provide lower energy consumption, easier installation, and reduced noise levels, making them suitable for less demanding tasks. By understanding the characteristics of each system and considering factors such as conveying distance, material properties, and operational requirements, you can select the most appropriate air conveying solution for your wet ammonium nitrate handling needs. It is recommended to consult with a qualified engineering firm, such as Shandong HeadPowder Engineering Co., Ltd., to conduct a thorough analysis of your specific application and provide tailored recommendations for the most efficient and cost-effective air conveying system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top