Quartz sand pneumatic conveying systems are essential for efficient material handling in various industrial applications. These systems utilize air pressure to transport quartz sand and other granular materials over long distances with minimal maintenance and operational complexity. The operation process and working principle of such equipment are crucial for understanding its effectiveness and suitability for different industrial needs.
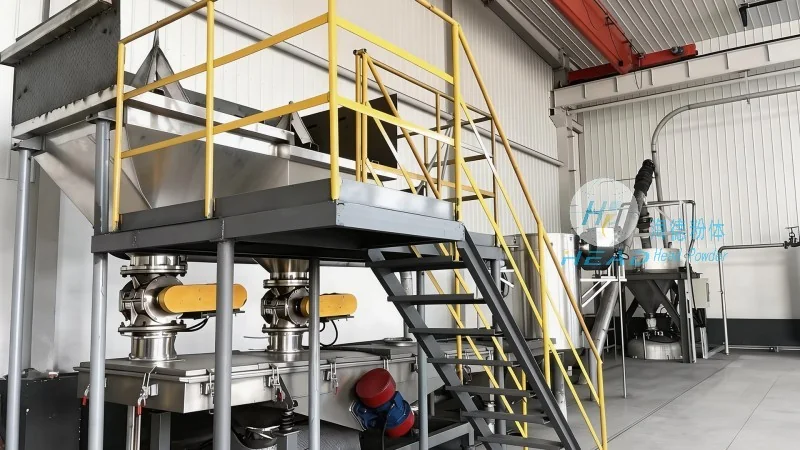
The quartz sand pneumatic conveying system typically consists of several key components, each playing a vital role in the overall operation. These include the material hopper, which stores the quartz sand; the air compressor or blower, responsible for generating the necessary air pressure; the conveying line, which transports the material; and the receiver or discharge hopper, where the material is deposited. Additionally, components like filters, silencers, and control valves ensure the system operates smoothly and safely.
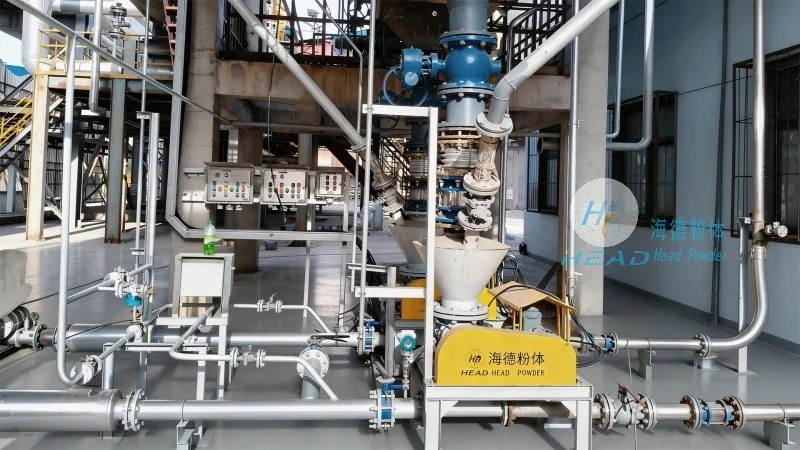
The working principle of a quartz sand pneumatic conveying system is based on the principle of air movement and material suspension. When the air compressor starts, it generates high-pressure air that enters the conveying line. The quartz sand is introduced into the system, either by gravity or through a feeder, and is then entrained by the air flow. The air-sand mixture travels through the conveying line to the receiver, where the air is separated from the material. The separated air is typically filtered and recycled back into the system, while the quartz sand is collected in the receiver. This process allows for continuous and efficient transport of quartz sand without the need for mechanical parts in contact with the material, reducing wear and tear.
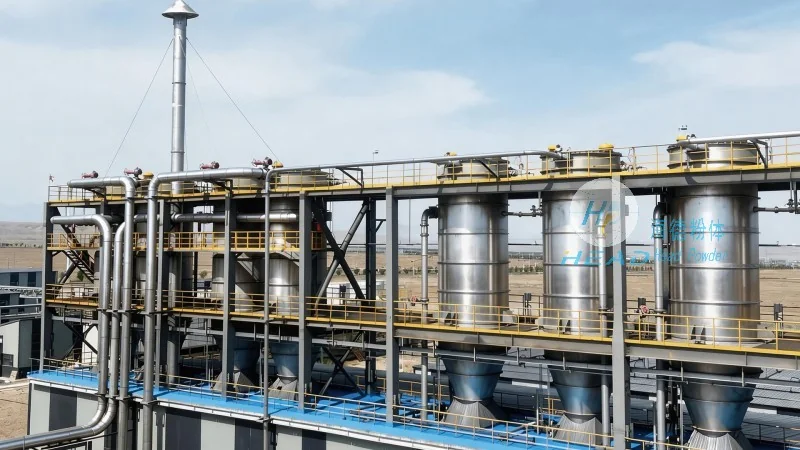
The operation process of a quartz sand pneumatic conveying system involves several sequential steps. First, the quartz sand is loaded into the material hopper. The feeder then regulates the flow of sand into the conveying line. The air compressor is activated, and the air pressure is adjusted to the appropriate level for the desired conveying distance and material characteristics. The sand is then introduced into the air stream, and the mixture is conveyed to the receiver. At the receiver, the air is separated from the sand, often using a cyclone or filter system. The sand is collected in the discharge hopper, and the air is recycled back to the compressor. This cycle repeats continuously as long as the system is in operation, ensuring a steady supply of quartz sand to the processing equipment.
Quartz sand pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These include reduced material degradation due to minimal contact with equipment, lower maintenance costs as there are fewer moving parts, and the ability to transport materials over long distances without the need for intermediate storage. The systems are widely used in industries such as construction, glass manufacturing, and mining, where quartz sand is a critical raw material. They are particularly suitable for applications requiring clean and dust-free material handling, as the enclosed system prevents dust from escaping into the environment.
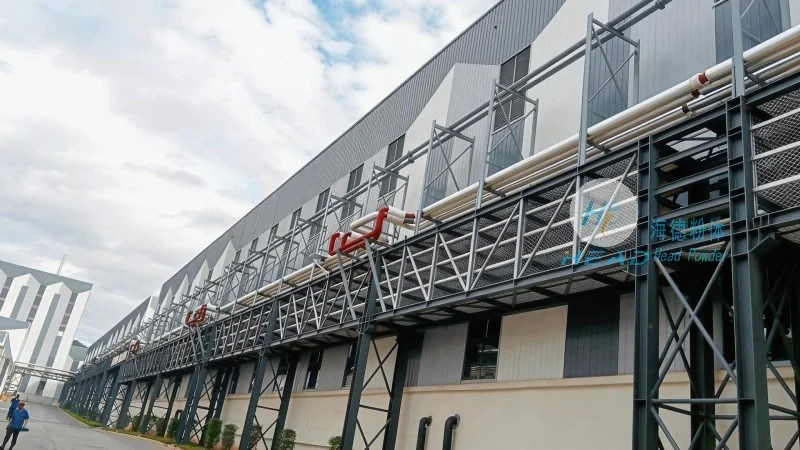
HeadPowder, a leading manufacturer of quartz sand pneumatic conveying systems, specializes in providing high-quality equipment tailored to the specific needs of industrial clients. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the material handling industry. HeadPowder's systems are designed to meet the highest standards of efficiency, reliability, and safety, ensuring optimal performance in various industrial environments. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility and a dedicated team of engineers and technicians.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top