Organic fertilizer pneumatic conveying systems are essential in modern agricultural and industrial settings, providing efficient and safe methods for transporting organic materials. Developed by Shandong HeadPowder Engineering Co., Ltd., a prominent manufacturer based in China, these systems offer reliable solutions for handling organic fertilizers with precision and minimal environmental impact. This article explores the operation process and working principles of such systems, offering a comprehensive overview of their functionality and benefits.
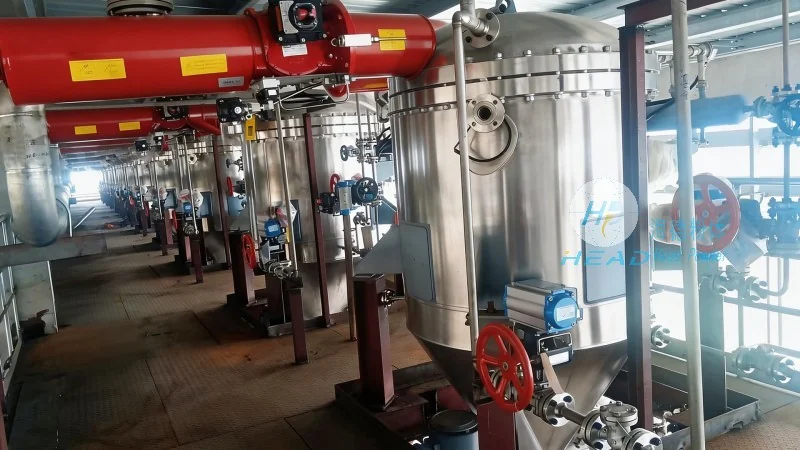
HeadPowder, the brand under Shandong HeadPowder Engineering Co., Ltd., specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for organic fertilizer processing. With a strong presence in Shandong, China, the company leverages decades of industry experience to deliver high-quality equipment that meets the demands of agricultural and environmental sectors. The company’s headquarters is located in Shandong, where it operates a state-of-the-art facility dedicated to research, development, and production of pneumatic conveying solutions.
The organic fertilizer pneumatic conveying system typically comprises several key components, each with a critical role in the overall operation. These components include a hopper for material storage, a feeder to control the flow of fertilizer, a blower or air compressor to generate conveying air, a pipeline network for material transport, and a receiver or discharge unit for material collection. Additional elements like filters, silencers, and pressure relief valves ensure safe and efficient operation. Each component is engineered to work in harmony, ensuring smooth and continuous material handling.
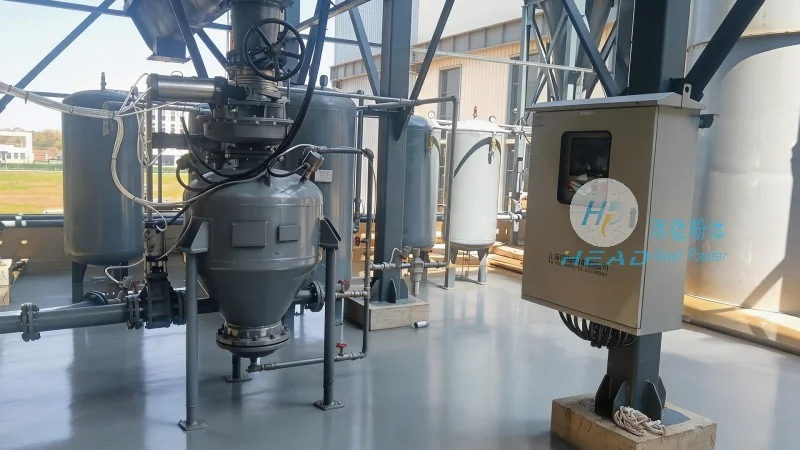
The operation of the organic fertilizer pneumatic conveying system follows a systematic sequence, beginning with material loading into the hopper. The feeder then regulates the flow of fertilizer into the pipeline, while the blower generates a high-pressure air stream. This air stream propels the organic fertilizer particles through the pipeline, transporting them from the source to the destination. The receiver collects the conveyed material, and the system maintains consistent flow by adjusting air pressure and material feed rate. The process is automated, allowing for precise control and minimal human intervention, which enhances operational efficiency and reduces labor costs.
The core working principle of the organic fertilizer pneumatic conveying system is based on using air as a medium to transport solid materials. The system operates on the principle of pneumatic transport, where the air flow creates a negative or positive pressure environment within the pipeline. In a negative pressure system, the blower draws air and material from the hopper, creating a vacuum that pulls the fertilizer through the pipeline. In a positive pressure system, the blower pushes air and material through the pipeline, creating a pressure differential that moves the material. Both systems rely on the interaction between air velocity and particle size to ensure effective conveying. The system’s efficiency is influenced by factors such as air velocity, material density, and pipeline length, all optimized during design for maximum performance.
Organic fertilizer pneumatic conveying systems offer numerous advantages over traditional mechanical conveying methods. These include reduced labor costs, increased operational efficiency, and improved safety due to the enclosed system design, which minimizes dust exposure and environmental contamination. The systems are also highly flexible, allowing easy integration with existing processing facilities and adaptability to varying material types and quantities. Additionally, the enclosed pipeline network prevents material spillage and contamination, maintaining product quality and compliance with environmental regulations. The reliability of these systems, coupled with low maintenance requirements, makes them a cost-effective solution for long-term use in agricultural and industrial applications.
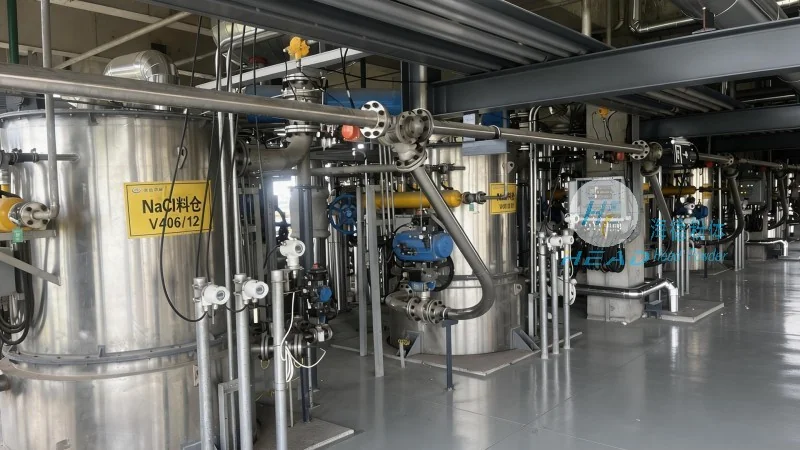
The organic fertilizer pneumatic conveying systems manufactured by HeadPowder are widely used in various industries, including agricultural fertilizer production, composting facilities, and organic waste processing plants. These systems are particularly beneficial in large-scale operations where efficient material handling is critical for productivity and profitability. The systems are also suitable for transporting organic fertilizers to storage facilities, blending plants, or distribution centers, ensuring a consistent supply chain. By leveraging advanced technology and engineering expertise, HeadPowder’s systems cater to the specific needs of different industries, providing customized solutions that enhance operational performance and sustainability.
In conclusion, the organic fertilizer pneumatic conveying system by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and efficient solution for the transportation of organic materials. Through its systematic operation process and robust working principles, the system ensures reliable and safe handling of organic fertilizers, contributing to the sustainability of agricultural and environmental practices. With a strong commitment to quality and innovation, HeadPowder continues to advance the technology of pneumatic conveying systems, meeting the evolving needs of the industry and promoting efficient material handling worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top