The sugar powder pneumatic conveying system is a specialized industrial equipment designed for the efficient transportation of granular or powdered materials, particularly in the sugar processing industry. This system utilizes air as the conveying medium to move sugar powder from one location to another, ensuring a clean, dust-free, and reliable transfer process. The system is engineered to handle the unique characteristics of sugar powder, such as its fine particle size, hygroscopic nature, and the need for contamination-free handling, making it an essential component in modern sugar production and processing facilities.
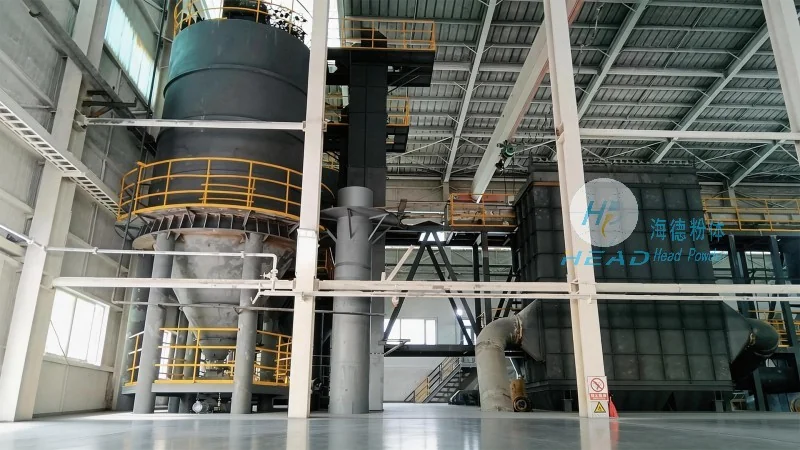
Headpowder, the professional manufacturer of this advanced pneumatic conveying system, is a leading company based in Shandong, China. With years of experience in the engineering and manufacturing of material handling equipment, Headpowder specializes in providing customized solutions tailored to the specific needs of the sugar industry. The company's commitment to quality, innovation, and customer satisfaction has established it as a trusted partner for sugar processing plants worldwide.
The core of the sugar powder pneumatic conveying system lies in its ability to use compressed air to transport the material. The system typically consists of several key components, including a hopper for material storage, a rotary valve or feeder to control the flow of sugar powder, a conveying pipe network, and a receiver or destination vessel. The process begins when the sugar powder is fed from the hopper into the conveying line through the feeder. Compressed air is then introduced into the pipe, creating a flow that lifts and propels the powder particles through the system. The air and powder mixture travels through the pipeline, with the air providing the necessary force to overcome gravity and friction, ensuring smooth and continuous movement. At the receiving end, the air is separated from the powder, often through a cyclone separator or filter, and the purified air is discharged, while the sugar powder is collected in the designated container. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency.
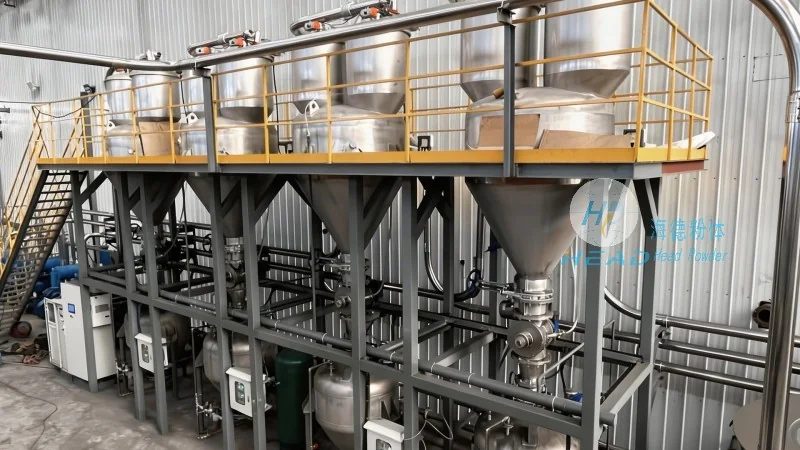
The operation of the sugar powder pneumatic conveying system involves a series of controlled steps to ensure optimal performance and material handling. First, the sugar powder is loaded into the storage hopper, which is equipped with a level indicator to monitor the material volume. The feeder, usually a rotary valve or a screw feeder, regulates the flow rate of the powder into the conveying line. The compressed air is supplied from a dedicated air compressor, which maintains a consistent pressure and flow rate. The air is introduced into the conveying pipe at the inlet, creating a positive pressure that draws the powder into the system. As the air and powder mixture moves through the pipeline, it passes through any necessary fittings, such as bends or expansion joints, which are designed to minimize pressure loss and maintain the flow. The receiving vessel is positioned at the end of the system, where the powder is deposited. The air, now separated from the powder, is filtered and vented to the atmosphere, while the powder is collected in the receiver. The system can operate in either positive or negative pressure modes, depending on the application requirements. Positive pressure systems are commonly used for long-distance or high-rise conveying, as they maintain a higher pressure than the ambient air, ensuring the material is continuously pushed forward. Negative pressure systems, on the other hand, are used for short-distance conveying or when the material needs to be drawn from a lower elevation, as they create a vacuum that pulls the powder into the system.
Compared to traditional mechanical conveying methods, the sugar powder pneumatic conveying system offers several significant advantages. One of the primary benefits is the elimination of mechanical contact with the material, which prevents contamination and ensures the purity of the sugar powder. This is particularly important in the food industry, where product quality and safety are paramount. Additionally, the system reduces the risk of product degradation due to friction or impact, as the powder is conveyed in a gentle, air-supported manner. The system also provides a dust-free environment, which enhances workplace safety and compliance with environmental regulations. Furthermore, the pneumatic conveying system is highly flexible and can be easily integrated with existing production lines, allowing for seamless material transfer between different stages of the sugar processing process. The modular design of the system enables customization to meet specific operational requirements, such as varying flow rates, conveying distances, or material characteristics. This adaptability makes the system suitable for a wide range of applications, from small-scale sugar processing plants to large industrial facilities.
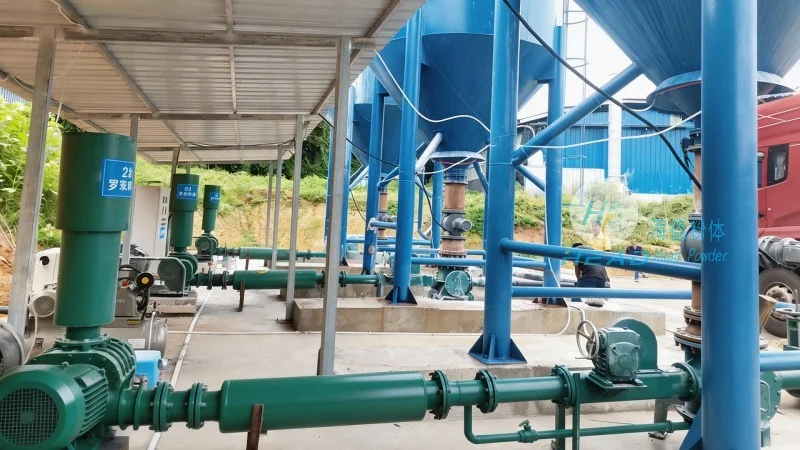
To ensure the long-term reliability and efficiency of the sugar powder pneumatic conveying system, regular maintenance and proper operation are essential. The system components, such as the hopper, feeder, and conveying pipes, should be inspected regularly for any signs of wear or damage. The rotary valve or screw feeder should be checked for proper alignment and lubrication to prevent blockages or uneven flow. The air compressor and air filtration system must be maintained to ensure consistent air quality and pressure. The cyclone separator or filter should be cleaned periodically to prevent clogging and maintain optimal air separation efficiency. The receiving vessel and storage hopper should be inspected for any material buildup or contamination, which could affect the quality of the final product. Regular cleaning of the system, especially after handling different types of materials or during shutdown periods, is crucial to prevent cross-contamination and maintain hygiene standards. By following a proper maintenance schedule, the system can operate at peak performance, minimizing downtime and maximizing the overall efficiency of the sugar processing operation.
The sugar powder pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. represents a cutting-edge solution for the efficient and reliable transportation of sugar powder in the sugar industry. By leveraging the principles of pneumatic conveying, this system offers superior performance, enhanced product quality, and improved operational efficiency compared to traditional methods. With its robust design, flexible configuration, and commitment to quality, Headpowder's system is an ideal choice for sugar processing plants seeking to optimize their material handling processes. The company's expertise and experience in the field ensure that customers receive a tailored solution that meets their specific needs, contributing to the overall success and profitability of their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top