Grain powder pneumatic conveying systems are critical equipment in the agricultural and food processing sectors, designed to transport bulk materials such as grains, powders, and fine particulates through a pressurized or vacuum air stream. These systems provide an efficient and reliable method for moving materials over short to medium distances, commonly utilized in storage facilities, processing plants, and distribution centers. The technology integrates pneumatic principles with mechanical components to ensure safe, clean, and continuous material handling, making them indispensable in industries where material transport efficiency and hygiene are paramount.
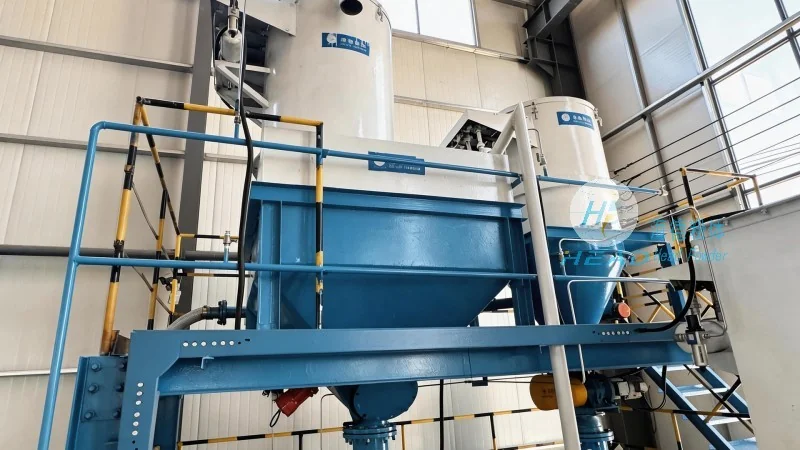
The fundamental components of a grain powder pneumatic conveying system include the material hopper, feed mechanism, air compressor or vacuum pump, conveying line, and discharge outlet. The material hopper stores the bulk grain or powder, while the feed mechanism—such as a rotary valve or screw feeder—controls the flow rate into the system. The air compressor generates the necessary pressure or vacuum to move the material through the conveying line, which is typically constructed from metal or flexible tubing. The discharge outlet delivers the material to the destination, such as a silo, processing unit, or packaging line. Each component is essential for the system's smooth operation and efficient material transport.
The working principle of a grain powder pneumatic conveying system is based on suspending material particles in an air stream. In a pressurized system, air is forced into the conveying line, creating a high-pressure environment that lifts and transports the material particles. The material is carried by the air flow, and the velocity of the air determines the system's capacity and conveying distance. In a vacuum system, a vacuum pump creates a low-pressure area that draws the material into the line, pulling it from the source to the destination. The choice between pressurized and vacuum systems depends on factors like material characteristics, distance, and system layout. The system ensures the material remains suspended in the air stream, preventing clogging and maintaining consistent flow.
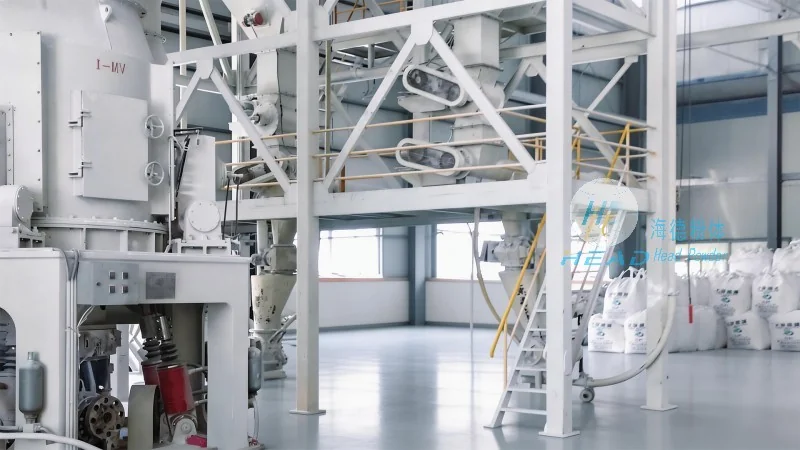
The operation process of a grain powder pneumatic conveying system involves sequential steps to ensure proper material handling. First, the material is loaded into the hopper, and the feed mechanism is activated to control the flow rate. The air compressor or vacuum pump is then started, creating the necessary pressure or vacuum. The material is fed into the conveying line as the air stream moves through, carrying the particles to the discharge outlet. The system monitors pressure and flow rates to maintain optimal performance, adjusting as needed to prevent overloading or underloading. The entire process is automated, allowing for continuous operation with minimal human intervention. This automation ensures efficiency and consistency, reducing downtime and improving overall productivity.
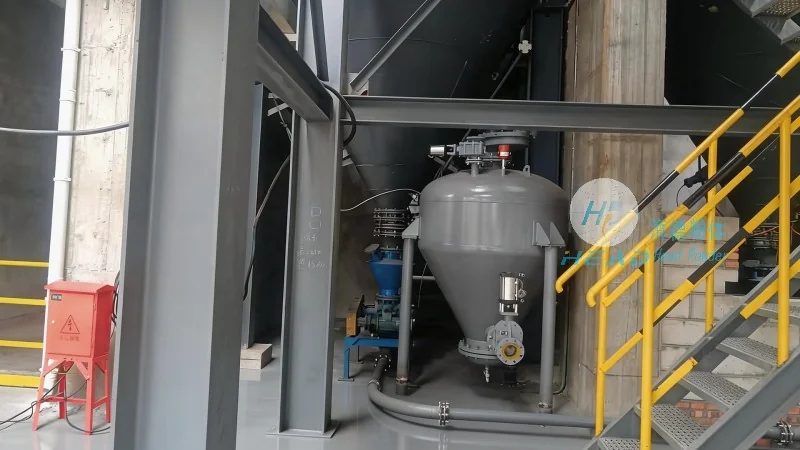
Pneumatic conveying systems offer several advantages for grain and powder handling, making them a preferred choice in many industries. One key advantage is the ability to transport materials in a closed system, which prevents contamination from dust, moisture, or environmental factors. This is particularly critical for food-grade grains, where hygiene and product safety are non-negotiable. Additionally, pneumatic systems are flexible and can be configured to handle various material types and distances, from short in-plant transfers to long-distance transport. They also reduce labor costs by automating the material handling process, as the system can operate continuously without constant monitoring. Furthermore, these systems are energy-efficient compared to traditional methods like belt conveyors or trucks, as they use air pressure to move materials, minimizing energy consumption. The compact design of pneumatic systems also saves space in processing facilities, making them suitable for both new and existing plants.
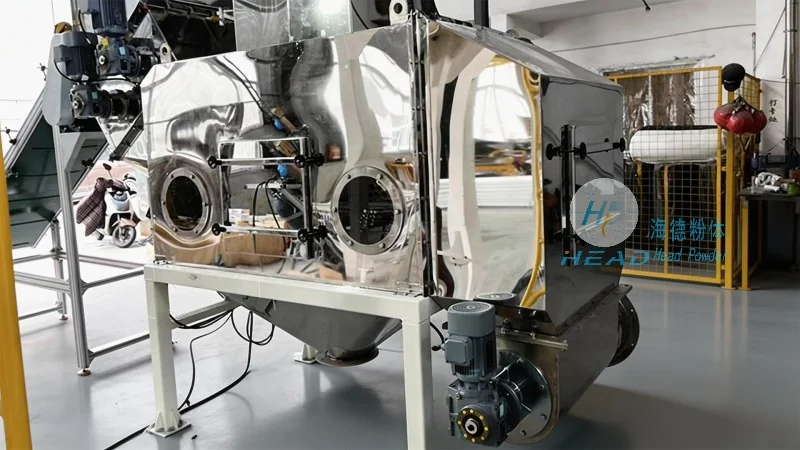
Grain powder pneumatic conveying systems are widely applied in various applications within the agricultural and food processing sectors. In grain storage facilities, these systems are used to transfer harvested grains from storage silos to processing units or packaging lines. They are also employed in flour mills to move raw flour from grinding equipment to storage silos or packaging machines. Additionally, in food processing plants, pneumatic conveyors are used to transport ingredients like sugar, spices, or other powders to mixing and packaging equipment. The systems are particularly useful in applications where material handling needs to be clean, efficient, and hygienic, such as in the production of bakery products, snacks, or other food items. The ability to handle fine powders without clogging or contamination makes these systems ideal for industries where product quality and safety are paramount.
Proper maintenance is essential to ensure the long-term performance and reliability of grain powder pneumatic conveying systems. Regular maintenance tasks include checking the air compressor or vacuum pump for proper operation, inspecting the conveying line for blockages or wear, and cleaning the material hopper and feed mechanism to prevent material buildup. It is also important to monitor pressure and flow rates during operation to detect any issues early. Common troubleshooting steps include checking for air leaks in the system, ensuring the feed mechanism is operating at the correct speed, and cleaning the discharge outlet to prevent clogging. If the system experiences reduced capacity or increased pressure, it may indicate a blockage in the conveying line, which can be cleared by stopping the system and manually removing the material. Regular maintenance and timely troubleshooting help to minimize downtime and extend the lifespan of the equipment, ensuring consistent and reliable material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top