Cocoa powder, a critical ingredient in chocolate and confectionery production, demands efficient and hygienic handling during processing. The pneumatic conveying system is a key technology utilized by manufacturers to transport cocoa powder from storage silos or processing units to production lines. This article explores the operation process and working principle of such systems, emphasizing the equipment's design, functionality, and the role of Shandong HeadPowder Engineering Co., Ltd. as a leading provider in the industry.
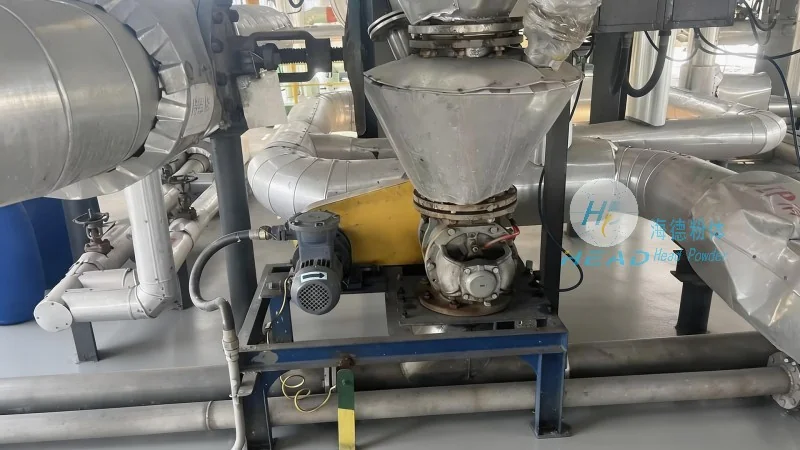
The cocoa powder pneumatic conveying system comprises several interconnected components that collaborate to ensure smooth material transport. Key components include a hopper or feeder for receiving the powder, a blower or compressor to generate air pressure, a pipeline network for conveying the powder, a separation unit to isolate the powder from the air, and a receiver or discharge hopper at the destination. Each component is engineered to preserve the integrity of the cocoa powder while ensuring efficient and clean operation.
The system's operation follows a systematic sequence: cocoa powder is fed into the hopper from a storage silo or processing unit, then regulated by the feeder into the pipeline. Simultaneously, the blower generates a high-pressure air stream introduced into the pipeline. As the air flows, it carries the cocoa powder particles, creating a mixture that travels through the pipeline to the destination. At the end, a separation unit (cyclone or bag filter) separates the powder from the air. The powder is collected in the receiver hopper, while the air is either vented or recirculated. This process ensures continuous and reliable transport of cocoa powder.
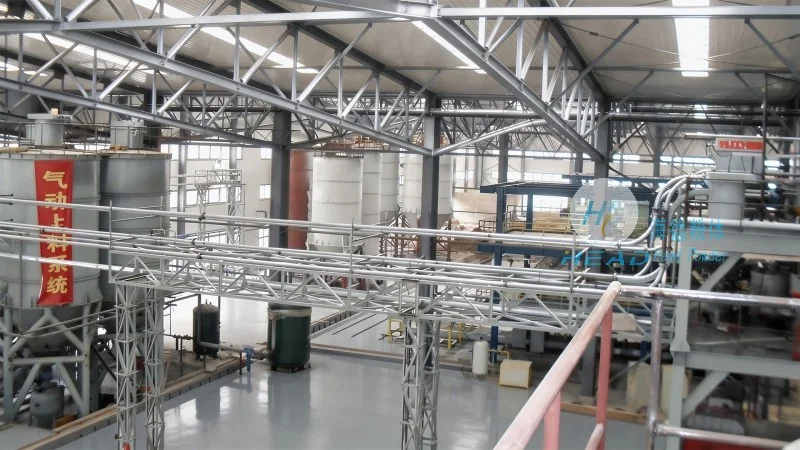
The pneumatic conveying system operates on principles of fluid dynamics. In a positive pressure system, the blower supplies high-pressure air that forces cocoa powder particles through the pipeline. The air acts as a carrier, suspending particles and transporting them. The air velocity must be sufficient to keep particles suspended without causing equipment wear or powder degradation. In a negative pressure system, the blower creates a vacuum at the destination, drawing the powder-air mixture into the pipeline. Both systems leverage air flow to move solid particles, with the choice depending on application requirements like distance and material properties.
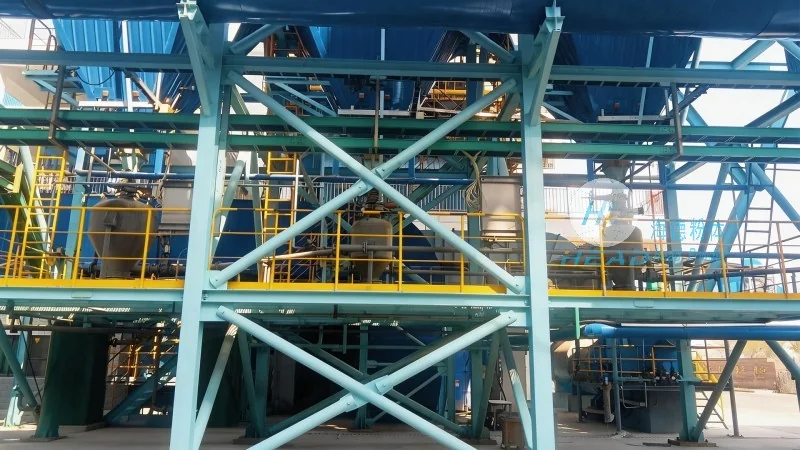
The system offers several technical advantages: it provides a hygienic, dust-free transport method essential for food processing to maintain product quality and comply with regulations. It is highly efficient, moving large volumes over long distances with lower energy consumption than traditional methods like belt conveyors. The equipment is flexible, easily integrated into existing production lines, allowing adjustments to flow rates or destinations. These benefits make the system suitable for applications such as transporting cocoa powder from storage to mixing units, from mixing to packaging, or in batch processing where precise material control is critical.
Shandong HeadPowder Engineering Co., Ltd., branded as headpowder, is a leading manufacturer of pneumatic conveying systems and related equipment for the food processing industry. Headpowder specializes in designing and producing customized solutions tailored to clients' needs, including those in cocoa and chocolate manufacturing. The company is headquartered in Shandong, China, and has built a strong reputation for delivering high-quality, reliable equipment that meets international hygiene and performance standards. With a focus on innovation and customer satisfaction, headpowder remains a trusted partner for businesses seeking efficient and effective cocoa powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top