HeadPowder, a leading manufacturer in the field, specializes in providing advanced pneumatic conveying solutions for industrial applications. The company, based in Shandong, China, has established itself as a trusted partner for clients seeking efficient and reliable equipment for handling magnesium oxide and other bulk materials. This article delves into the operational process and working principles of their pneumatic conveying systems, highlighting key components and the technology behind seamless material transport.
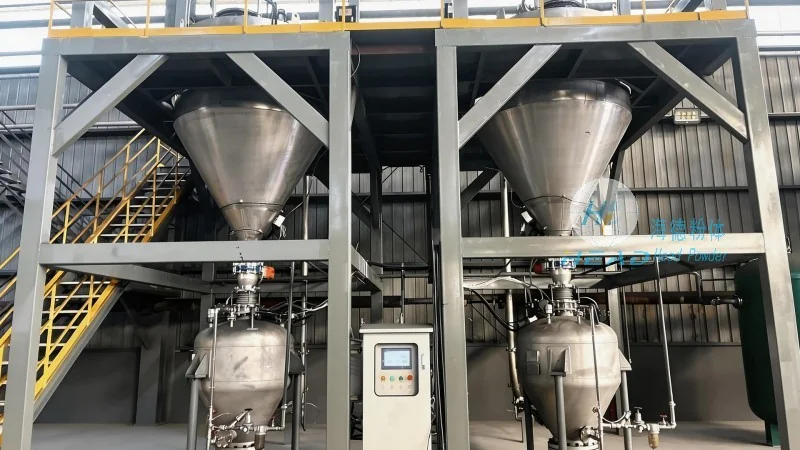
The magnesium oxide pneumatic conveying system consists of several critical components that work in tandem to ensure effective material handling. These include the hopper, which serves as the storage and feeding unit, the air compressor or blower that generates the necessary airflow, the pipeline network that transports the material, and the control system that regulates the entire process. Each component plays a vital role in maintaining the system's efficiency and safety.
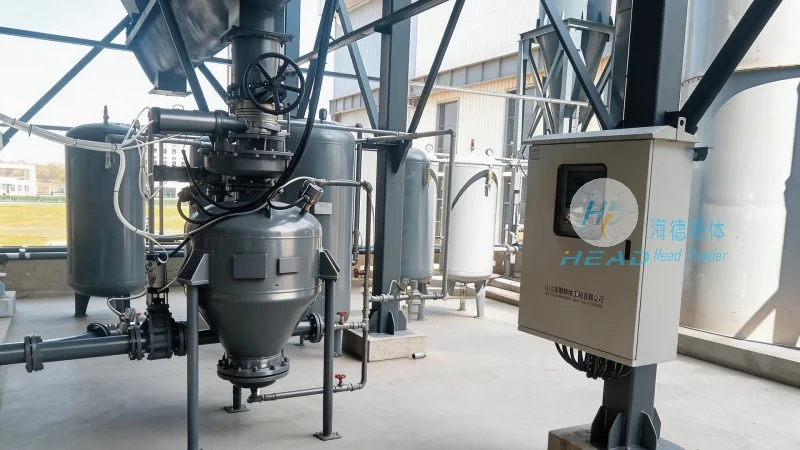
The operation process begins with the material being loaded into the hopper. The control system then activates the air compressor, which generates a high-pressure airflow. This airflow is directed into the pipeline, creating a pressure differential that draws the magnesium oxide from the hopper into the system. As the material is conveyed through the pipeline, it is mixed with the air, forming a slurry-like mixture. The mixture travels through the pipeline network to the discharge point, where the material is separated from the air and deposited into the receiving container. The control system continuously monitors the pressure, flow rate, and material level to ensure optimal performance and prevent any potential issues.
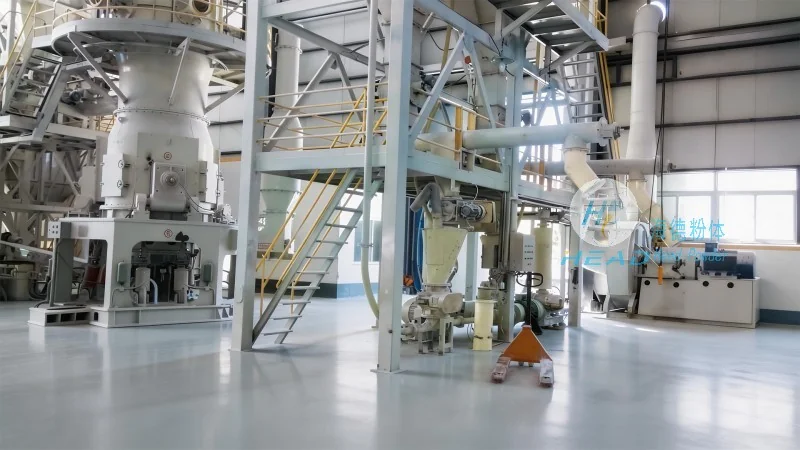
The working principle of the pneumatic conveying system is based on the principle of fluidization and the use of air as the conveying medium. The air compressor provides the necessary pressure to create a flow of air through the pipeline. The material is introduced into the system at the hopper, where it is entrained by the air flow. The air flow carries the material particles along the pipeline, maintaining a consistent velocity to prevent particle settling or blockages. The system utilizes either positive pressure or negative pressure (or a combination of both) depending on the application requirements. Positive pressure systems are commonly used for short-distance conveying, while negative pressure systems are suitable for longer distances or when handling dusty materials. The control system ensures that the air pressure and flow rate are adjusted according to the material characteristics and system requirements, optimizing the conveying efficiency.
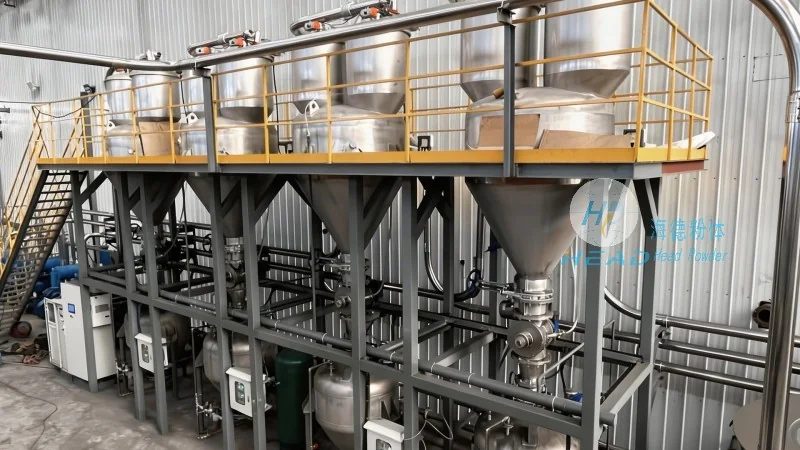
Implementing a pneumatic conveying system for magnesium oxide offers several advantages over traditional methods such as belt conveyors or bucket elevators. These systems provide a dust-free and enclosed environment, reducing the risk of material contamination and improving workplace safety. They also offer higher conveying speeds and greater flexibility in terms of layout and routing, allowing for more efficient use of space. Additionally, the system can handle a wide range of material sizes and moisture contents, making it suitable for various industrial applications. The automated control system enhances operational efficiency and reduces the need for manual intervention, leading to lower labor costs and increased productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top