Mineral powder material handling systems are integral to modern industrial operations, facilitating the efficient transport of bulk materials such as ores, powders, and granules. These systems are designed to optimize workflow, enhance operational efficiency, and ensure safety in environments ranging from mining sites to chemical processing plants. The principles underlying these systems revolve around selecting the appropriate transport mechanism based on material properties, such as particle size, moisture content, and abrasiveness, as well as the operational requirements of the application.
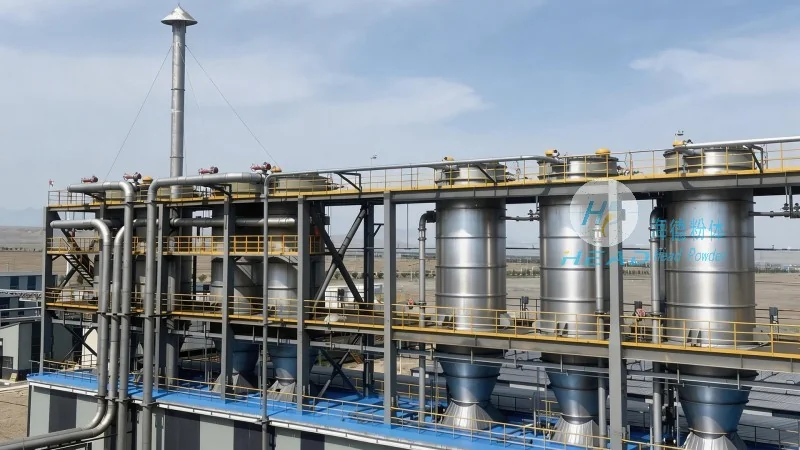
The fundamental principles of mineral powder material handling systems include the selection of suitable transport technologies and the integration of control systems to manage material flow. Belt conveyors, a common choice for horizontal and slight incline transport, utilize continuous belts to move materials at high speeds and capacities. Their design allows for easy integration with other equipment, such as crushers and screens, enabling seamless material processing. Pneumatic conveying systems, on the other hand, employ air pressure to transport fine powders through pipelines, offering advantages like reduced material degradation and the ability to handle materials with high moisture content. Bucket elevators are used for vertical transport, effectively lifting materials from lower to higher levels while maintaining consistent flow rates.
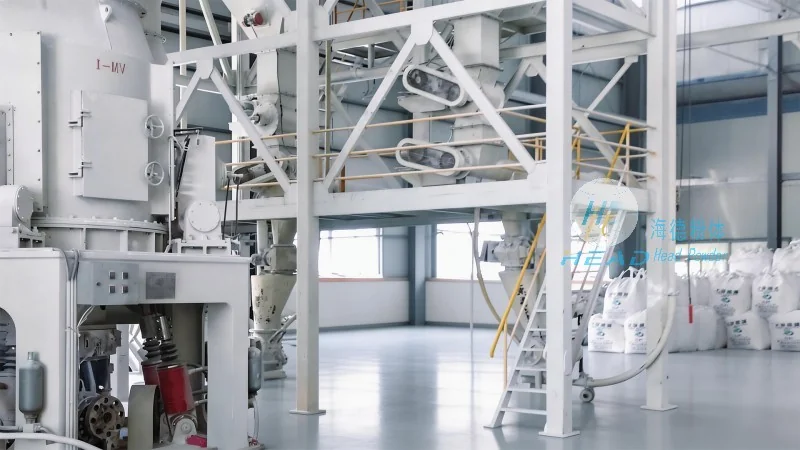
The working scene characteristics of mineral powder handling systems vary significantly across industries, influenced by factors like material type, processing scale, and environmental conditions. In mining operations, these systems must handle large volumes of crushed ores and rocks, often in harsh outdoor environments with high dust levels and temperature fluctuations. The systems are typically constructed with heavy-duty components to withstand abrasion and impact, ensuring long-term reliability. In chemical processing, the focus shifts to material purity and containment, as systems must prevent cross-contamination and ensure compliance with safety regulations. For example, in a pharmaceutical plant, mineral powder handling systems are designed with stainless steel components and sealed conveyor lines to maintain sanitary conditions and prevent product contamination. In food processing, the systems must adhere to strict hygiene standards, with features like easy cleaning and non-stick surfaces to handle powders like flour or sugar.
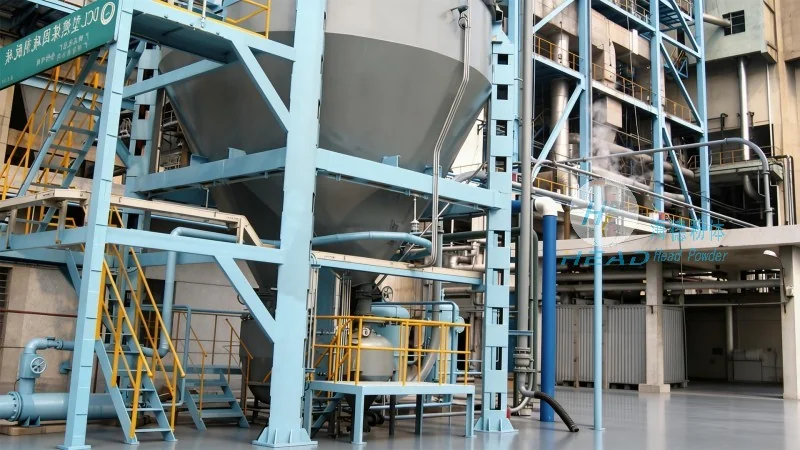
Efficient mineral powder material handling systems incorporate several key features that enhance performance and operational reliability. High-capacity belt conveyors, equipped with variable speed drives and durable rubber belts, allow for precise control over material flow rates, reducing spillage and improving throughput. Pneumatic conveying systems utilize advanced air filtration and pressure control to maintain consistent material transport, minimizing system downtime due to blockages or pressure fluctuations. Modern control systems, including PLC-based automation and SCADA monitoring, enable real-time data collection and remote operation, optimizing energy consumption and reducing maintenance costs. Additionally, safety features such as emergency stop buttons, overload sensors, and dust suppression systems are integrated to protect operators and comply with occupational health and safety regulations.
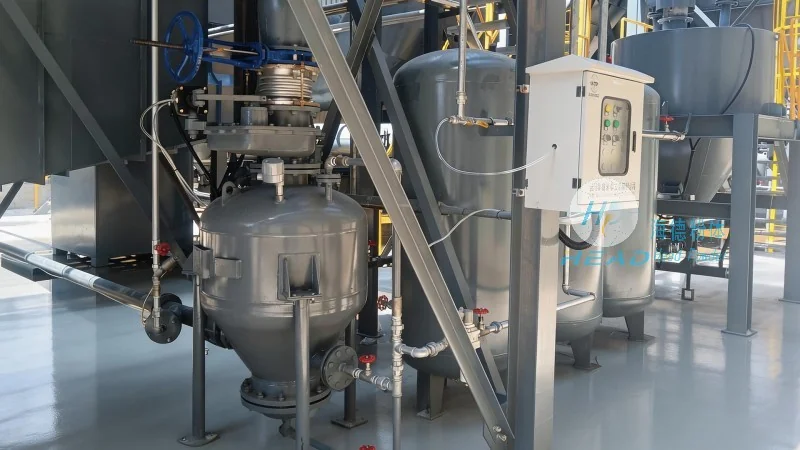
Real-world applications of mineral powder material handling systems illustrate their critical role in enhancing productivity and operational efficiency across various industries. In a coal mining facility, a belt conveyor system transports crushed coal from the mine to a processing plant, with a capacity of up to 3000 tons per hour. The system’s robust design, including reinforced idlers and heavy-duty pulleys, ensures reliable operation even under heavy loads and abrasive conditions. In a cement manufacturing plant, a pneumatic conveying system transports fine limestone powder from a grinding mill to a blending silo, ensuring precise dosing and minimal material loss. These examples demonstrate how mineral powder handling systems contribute to increased production rates, reduced labor costs, and improved product quality, making them indispensable in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top