HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling systems tailored for silica fume, a high-performance mineral admixture widely used in concrete and cement production. The silica fume material handling system is engineered to efficiently transport this fine powder, which is crucial for enhancing the durability and strength of construction materials. This article explores the underlying principles of such systems and highlights the key characteristics of their operational scenarios.
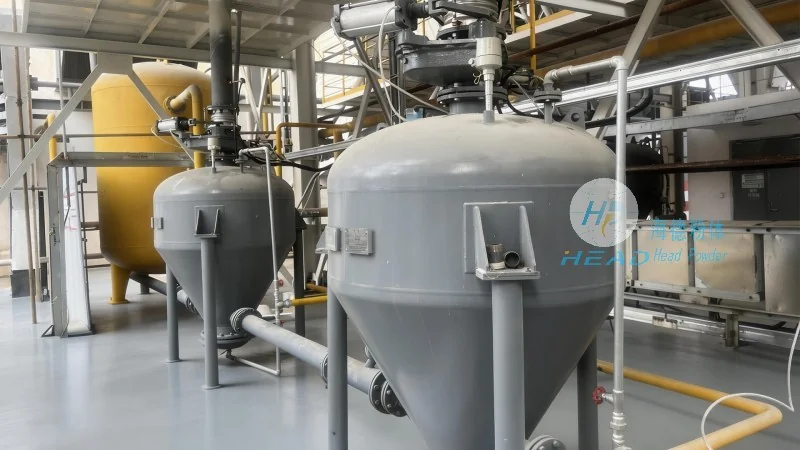
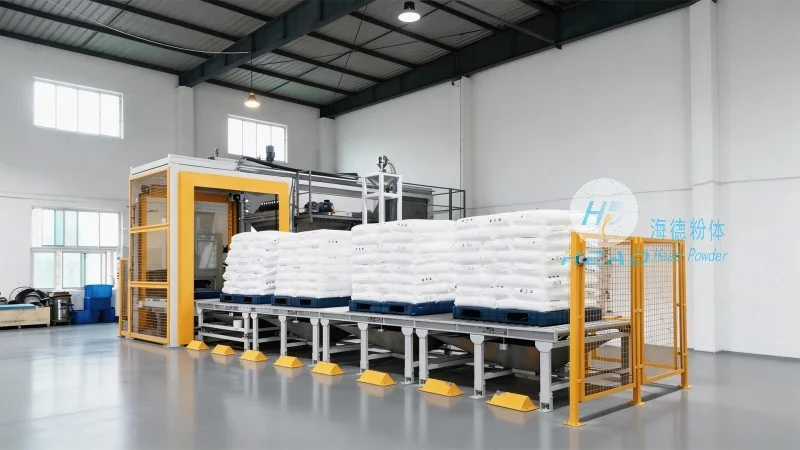
The fundamental principle of silica fume material handling systems revolves around the integration of advanced mechanical and pneumatic technologies to ensure safe, efficient, and reliable transportation of the fine powder. The system typically comprises several key components, including storage silos, conveying equipment (such as screw conveyors, pneumatic pipelines, or bucket elevators), and control systems. The storage silos are designed to accommodate large volumes of silica fume, often equipped with aeration systems to prevent caking and maintain consistent material flow. The conveying equipment is selected based on the specific characteristics of silica fume—its fine particle size, high specific surface area, and potential for dust generation. Pneumatic conveying, for instance, is commonly used for long-distance or high-rise applications due to its ability to handle fine powders without the need for mechanical contact, reducing wear and tear on equipment. Screw conveyors are preferred for short-distance, horizontal or slightly inclined transport, offering a cost-effective solution for moderate volumes. The control system plays a critical role in regulating the flow rate, pressure, and temperature within the system, ensuring optimal performance and preventing issues like blockages or overloading.
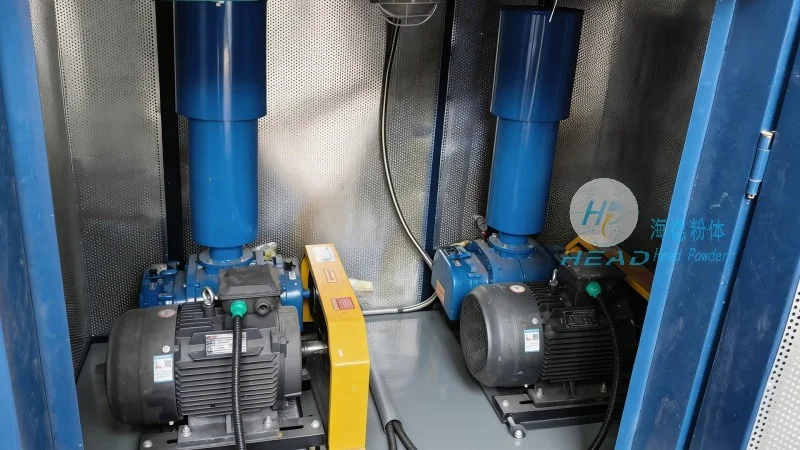
The operational scenarios of silica fume material handling systems vary significantly depending on the industrial application and environmental conditions. In concrete production facilities, the system is integrated into the batching process, where silica fume is added as a supplementary cementitious material (SCM) to replace a portion of Portland cement. The working scene here is characterized by high production throughput, often requiring continuous and automated material flow to meet the demands of large-scale construction projects. The system must be capable of handling high volumes of silica fume while maintaining precise dosage control to ensure consistent concrete quality. In cement factories, the silica fume handling system is part of the raw material preparation stage, where it is blended with other raw materials before being fed into the kiln. The working scene in this context involves higher temperatures and more stringent quality control, as the system must withstand the thermal stress and maintain the purity of the silica fume. Additionally, the system is often integrated with other material handling equipment, such as raw material crushers and mixers, requiring seamless coordination to avoid bottlenecks. In specialized industrial settings, such as refractory or specialty cement production, the silica fume handling system may operate in more controlled environments, focusing on the precise dosing of the admixture to achieve specific material properties. The working scene here emphasizes accuracy and repeatability, as small variations in silica fume content can significantly impact the final product's performance. Furthermore, the system must address the challenges posed by silica fume's fine particle size and dust generation, implementing dust collection and filtration systems to comply with environmental regulations and ensure workplace safety. The operational characteristics of the system in these scenarios include high efficiency, low maintenance, and robustness against the harsh conditions of industrial environments.
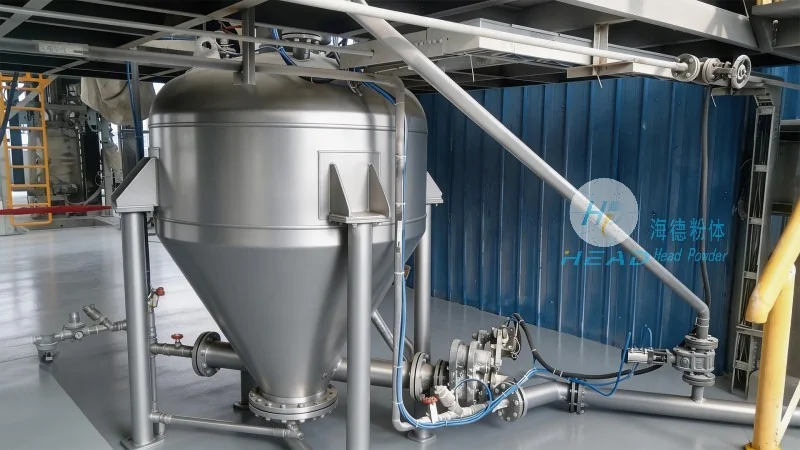
Shandong HeadPowder Engineering Co., Ltd., the parent company of HeadPowder, is a reputable enterprise dedicated to providing comprehensive engineering solutions for material handling and processing. With its headquarters in Shandong, China, the company leverages decades of experience in the construction and cement industries to develop tailored solutions for silica fume material handling. The company's team of engineers and technicians specializes in understanding the unique properties of silica fume and the specific requirements of different industrial applications, enabling the design of systems that are both efficient and cost-effective. HeadPowder's commitment to innovation is reflected in its use of advanced materials and technologies, such as high-strength stainless steel for conveying components to resist corrosion from silica fume, and intelligent control systems that optimize energy consumption and reduce operational costs. The company's operational base in Shandong positions it strategically to serve clients across the region and beyond, with a focus on delivering reliable and sustainable material handling solutions. By combining technical expertise with a customer-centric approach, HeadPowder ensures that its silica fume material handling systems meet the highest standards of performance and safety, supporting the growth and success of its clients in the construction and cement sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top